Cartons Are Crushed or Bottles Are Damaged in Case Packing
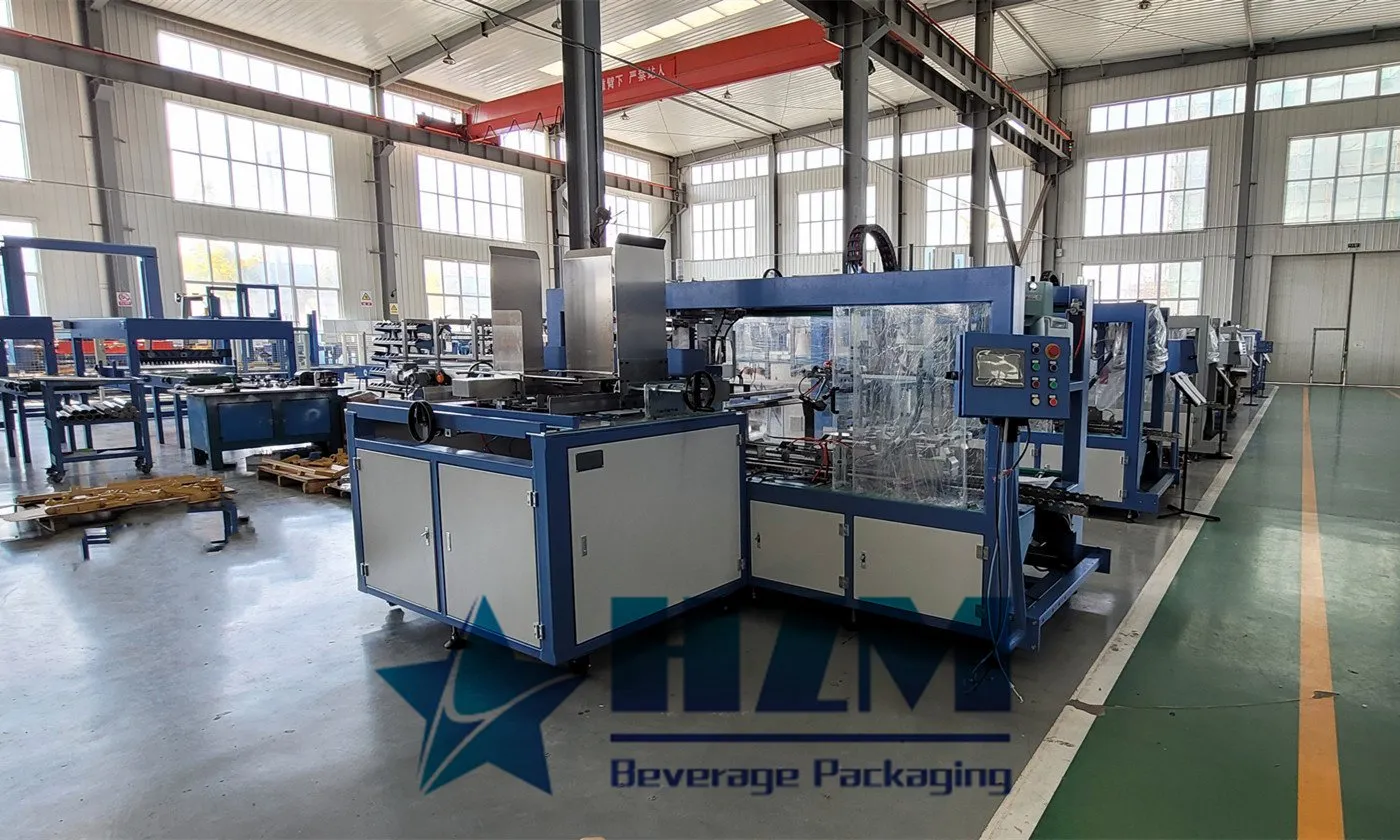
Check whether the case lacks strength or the machine applies excess force. Measure carton condition, pack geometry, compression, pusher load, guide clearance and downstream backpressure.
Use lockout/tagout before clearing a jam or entering the guarded packaging or palletizing cell. Allow heaters and sealing bars to cool, and secure suspended or robot-handled loads.
Locate the fault
- Case corners buckle after closing
- Bottle caps or labels scuff inside the carton
- Pusher or servo load alarms occur
- Damage appears only in one pack pattern
Inspection sequence
- Inspect damage location and determine the first station where it appears
- Verify carton material, moisture condition and dimensions
- Measure the assembled product group and internal case clearance
- Review pusher torque or force and actual end position
- Inspect mechanical stops, compression belts and guides
- Check downstream accumulation and case release timing
Corrective work
- Use carton board qualified for storage and load conditions
- Correct pack pattern, dividers or case dimensions
- Restore pusher and compression settings and repair binding
- Reduce harmful downstream backpressure and improve release control
Operating records and follow-up
- Incoming-check board and score quality
- Control carton storage
- Trend servo load
- Qualify every pack pattern
- Inspect downstream handling as part of packer setup
Equipment details: Automatic Drop Type Carton Packing Machine.
Need help planning your packaging line?
Share your product, bottle and capacity requirements for a practical equipment recommendation.
Choosing Between Shrink Packs and Cartons for Beverage Bottles
Shrink packing groups bottles in film and applies a controlled shrinking process. Carton packing loads bottles or cans into a specified board package.
Learn more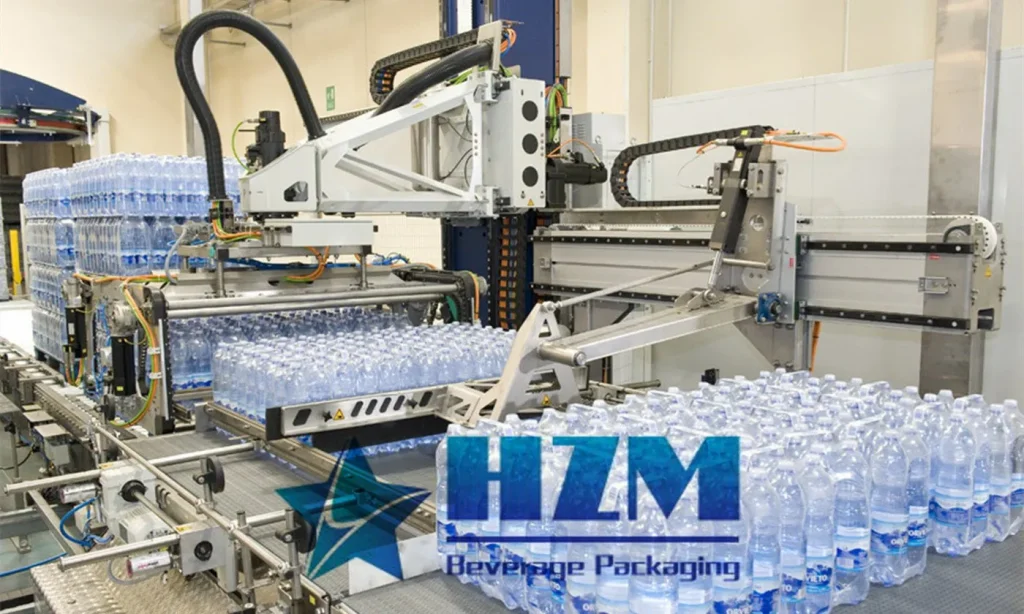
What an Automatic Palletizer Does After Case Packing
Identify palletizer infeed, layer formation or robot picking, pallet supply and discharge, then assess pack stability and the complete operating cycle.
Learn more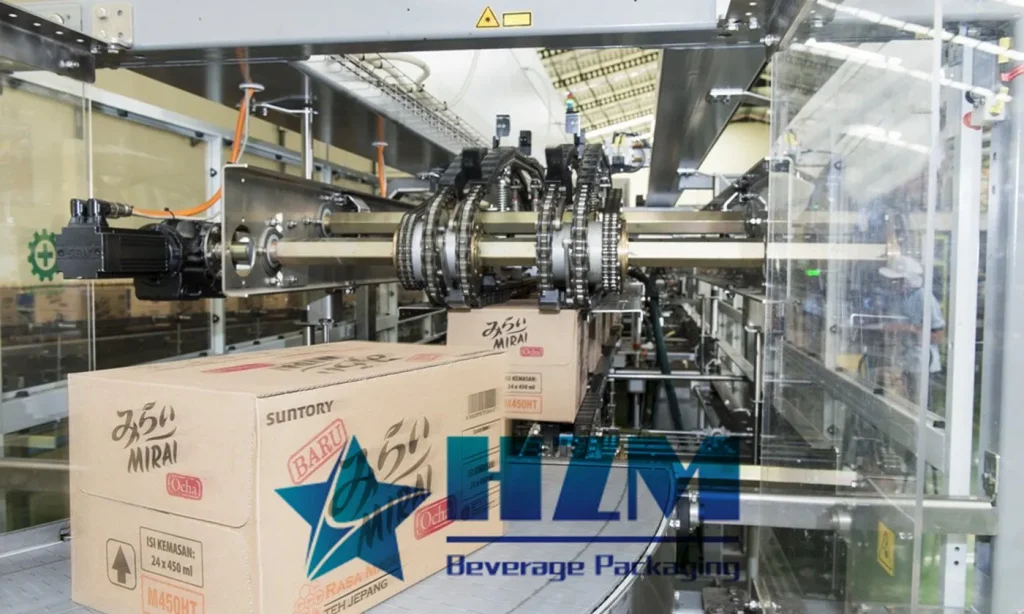
Choosing Equipment for Bottles Packed in Cartons
A machine loading filled bottles into corrugated cases performs secondary packaging. It is different from equipment that fills beverage directly into a carton package.
Learn more
Automatic Palletizer for Bottled Water Cartons and Shrink Packs: Selection Guide
How to specify an automatic palletizer for bottled water cartons, trays and shrink packs, including load data, pallet patterns, speed, stability, layout, safety and factory acceptance tests.
Learn more
Stabilizing Bottle Infeed Before Case Packing
Packing faults often begin before the packing head. Watch the transfer from single-file bottles to the required group and identify where a bottle first rotates, tips or loses spacing.
Learn more
Finding Where a Can First Becomes Damaged
A dented can at the seamer exit may have been damaged much earlier. Inspect incoming cans, depalletizing, conveyor transfers, filling lifts and seamer infeed in sequence.
Learn more