Insights & Updates
Hot-Fill Temperature Is Unstable at the Filler: Troubleshooting Steps
Unstable product temperature during hot filling should be investigated before small losses become a repeat breakdown. Operators need a safe test sequence that protects product, preserves the original settings and proves the cause with measured data.
Process-system alarms can affect both food safety and finished-product consistency. Temperature, time, flow, concentration, pressure and hygienic state must be evaluated as a connected process rather than as isolated instruments. In this case, temperature falls during speed changes or short stops is the key observation to preserve. Use the guide to rank likely causes and document the restored condition.
Quick answer: Treat hot-fill temperature as a process deviation. Hold affected product, verify the calibrated measurement point, then check heater capacity, recirculation, flow, bypass valves, stop-time logic and heat loss to the filler.
What operators usually see
Before opening the machine, compare the visible and measured symptoms. Note whether each one is continuous, intermittent or tied to a specific station: For this case, preserve evidence that shows whether temperature falls during speed changes or short stops.
- Temperature falls during speed changes or short stops
- Filler inlet and bowl instruments disagree
- The first bottles after restart are cooler than the validated limit
- Temperature oscillates with recirculation-valve movement
Make the equipment safe and protect the product
Place affected product on hold and follow the validated food-safety plan. Isolate heat, pressure, chemicals and rotating equipment before inspection; only an authorized process authority may release product after a critical deviation.
Preserve the batch record and trend temperature, flow, pressure, conductivity or concentration, valve states, recipe version and alarm history from before, during and after the deviation. Explicitly record whether temperature falls during speed changes or short stops.
Most likely causes, in practical checking order
1. Insufficient or unstable recirculation
Low flow and dead legs allow the filler circuit to cool during interruptions To test this explanation without guessing, place product from the uncertain period on hold under the food-safety plan Record the result before moving to the next cause.
2. Heat-exchanger or utility limitation
Fouling, low steam pressure or poor control prevents required heat transfer at peak rate A practical confirmation step is to compare installed sensors with a traceable reference at the approved measurement point. Compare the finding with a known-good run.
3. Sensor error or poor location
A drifting probe or unrepresentative installation reports a temperature different from the coldest product point Do not compensate for this condition in the recipe. First, trend inlet, return and filler temperatures with flow and line state Keep the original setting and measured result in the fault record.
4. Incorrect stop and divert sequence
Product reaches the filler before the loop has returned to validated temperature Separate this cause from the others with one controlled check: check heating-medium pressure, control-valve position and exchanger differential pressure Use the same product, format and speed for the comparison.
Step-by-step diagnostic procedure
Use the last known-good run as the baseline. If a check needs energized access or pressure exposure, use the manufacturer’s approved specialist procedure.
- Place product from the uncertain period on hold under the food-safety plan
- Compare installed sensors with a traceable reference at the approved measurement point
- Trend inlet, return and filler temperatures with flow and line state
- Check heating-medium pressure, control-valve position and exchanger differential pressure
- Verify recirculation flow and valve alignment in production and stop modes
- Review restart permissives and diversion logic against the validated process
Corrective actions that address the root cause
Apply a correction only to the cause demonstrated by the checks. Save the old parameter, removed part and measured condition for review.
- Repair or calibrate the confirmed faulty temperature channel
- Restore heating utility, exchanger cleanliness and stable control
- Correct recirculation restrictions and leaking or mispositioned valves
- Reinstate the validated hold, divert and restart sequence with authorized process approval
How to verify the repair before full-speed production
Before releasing full-speed production, reproduce the operating condition that originally exposed the fault. Then complete this acceptance check: Confirm that unstable product temperature during hot filling is absent for multiple consecutive cycles, not only for one sample. Review the alarm history and keep diagnostic product segregated until the site’s quality procedure releases it.
- Confirm that unstable product temperature during hot filling is absent for multiple consecutive cycles, not only for one sample.
- Compare the repaired result for “Temperature falls during speed changes or short stops” with the approved quality limit and the last known-good baseline.
- Check adjacent stations and downstream package quality for side effects associated with insufficient or unstable recirculation.
- For “Hot-Fill Temperature Is Unstable at the Filler: Troubleshooting Steps”, record the final settings, measurements, parts used and restart authorization.
Prevent the problem from returning
Add the checks below to the operator, sanitation or preventive-maintenance standard and assign a measurable acceptance condition.
- Calibrate critical temperature sensors on a risk-based schedule
- Trend coldest-point temperature through every stop
- Verify heat-exchanger performance before peak season
- Test divert and restart interlocks
- Require process-authority review for temperature or residence-time changes
When to stop troubleshooting and call a specialist
Stop and contact the machine or component supplier when unstable product temperature during hot filling cannot be isolated with non-invasive checks, when it returns after an approved repair, or when calibration requires protected service tools. Escalate immediately for a damaged pressure boundary, uncontrolled motion, food-safety risk, exposed conductor or repeated protective trip. Send the service engineer the fault history, photos, samples, trend data, recipe revision and work already completed.
Relevant equipment for this application
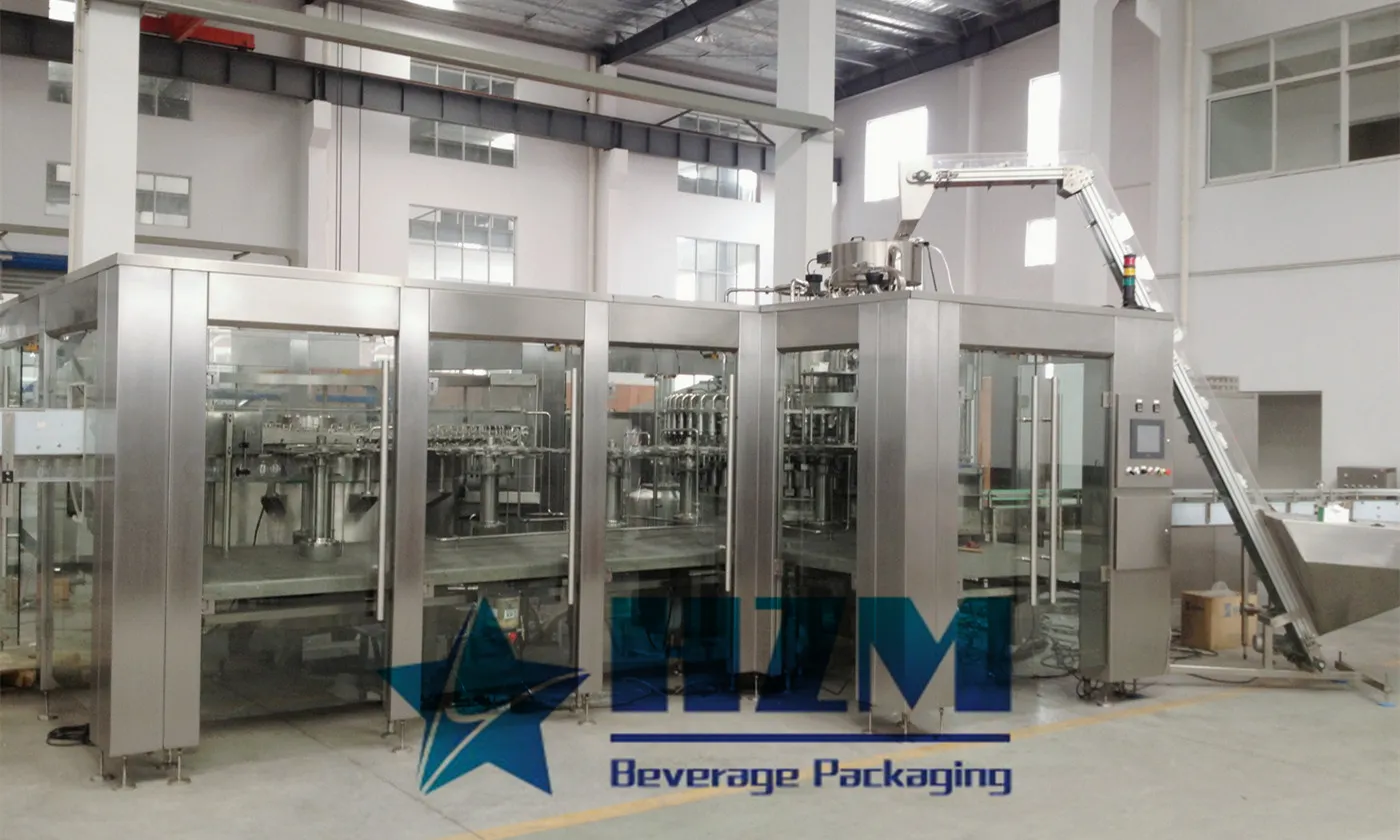
The site example most closely related to unstable product temperature during hot filling is the PET Bottle juice Beverage Hot Filling Machine. Equipment selection should be checked against samples, quality limits, required sustained output and available utilities.
Frequently asked questions
What should be checked first when unstable product temperature during hot filling?
Treat hot-fill temperature as a process deviation. Hold affected product, verify the calibrated measurement point, then check heater capacity, recirculation, flow, bypass valves, stop-time logic and heat loss to the filler. Preserve the original settings and take representative samples before repair work begins.
How can we distinguish insufficient or unstable recirculation from heat-exchanger or utility limitation?
Low flow and dead legs allow the filler circuit to cool during interruptions In contrast, fouling, low steam pressure or poor control prevents required heat transfer at peak rate Compare the two mechanisms under the same operating condition by completing these checks: place product from the uncertain period on hold under the food-safety plan Then compare installed sensors with a traceable reference at the approved measurement point
Can production continue while unstable product temperature during hot filling?
Only when the plant’s documented risk assessment and quality procedure allow it. For unstable product temperature during hot filling, stop and segregate production when package integrity, sanitation, validated processing, pressure safety, electrical protection or an uncontrolled reject trend is involved.
What evidence will help the equipment supplier respond faster?
Provide the model and serial number, product and format, target speed, first fault, timestamps, photos or video, affected station pattern and maintenance history. For this issue, also include temperature falls during speed changes or short stops and the measured result from this check: review restart permissives and diversion logic against the validated process
Talk to our engineering team
Need help planning your packaging line?
Share your product, bottle and capacity requirements for a practical equipment recommendation.
Equipment
PET Bottle juice Beverage Hot Filling Machine
Hot filling for juice and tea in heat-compatible PET bottles, with automatic rinsing, filling and capping.
Learn more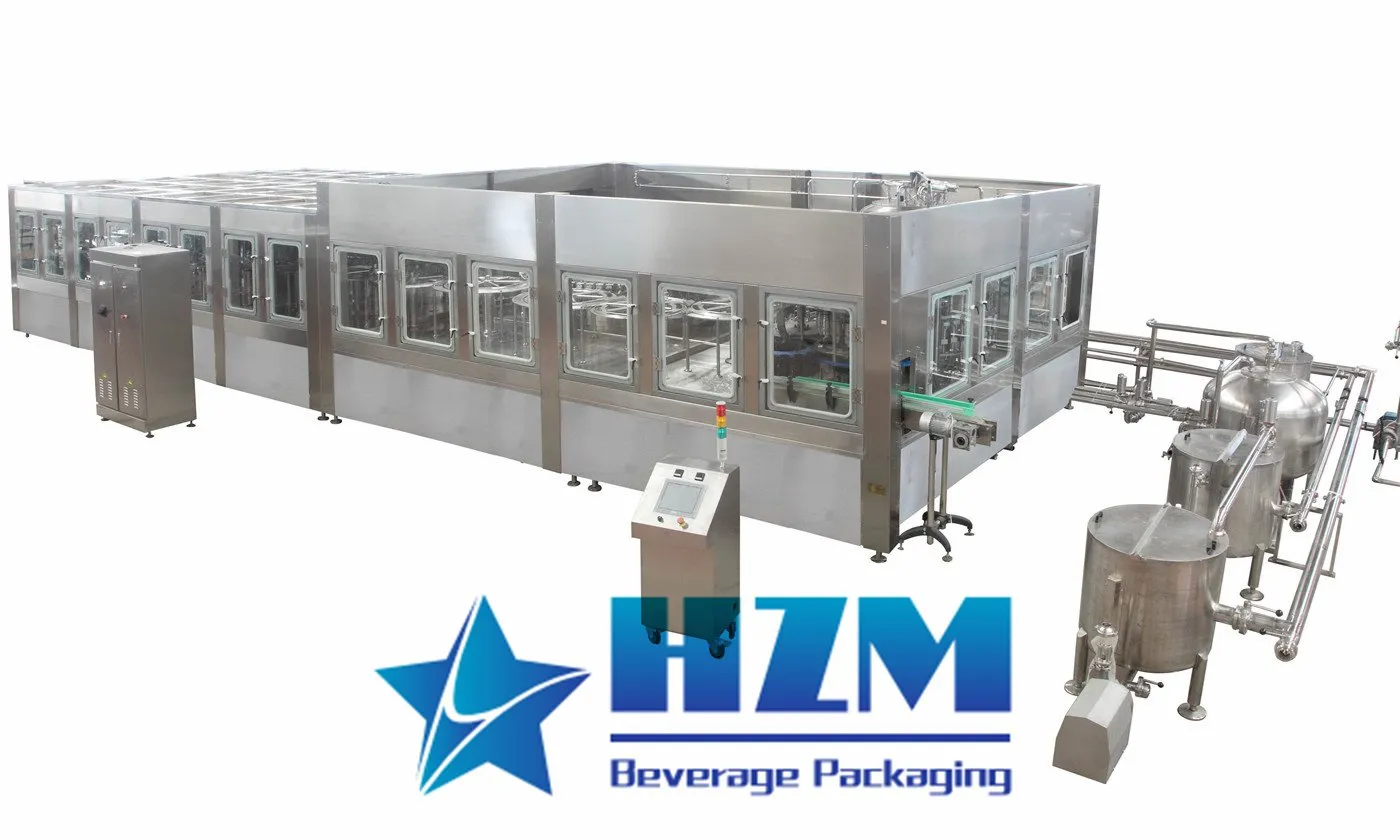
Equipment
Moderate Temperature Juice Filling Machine
Moderate-temperature juice filling with automatic bottle rinsing and capping, with XXGF models from 6,000 to 24,000 bottles/hour at 500 ml.
Learn more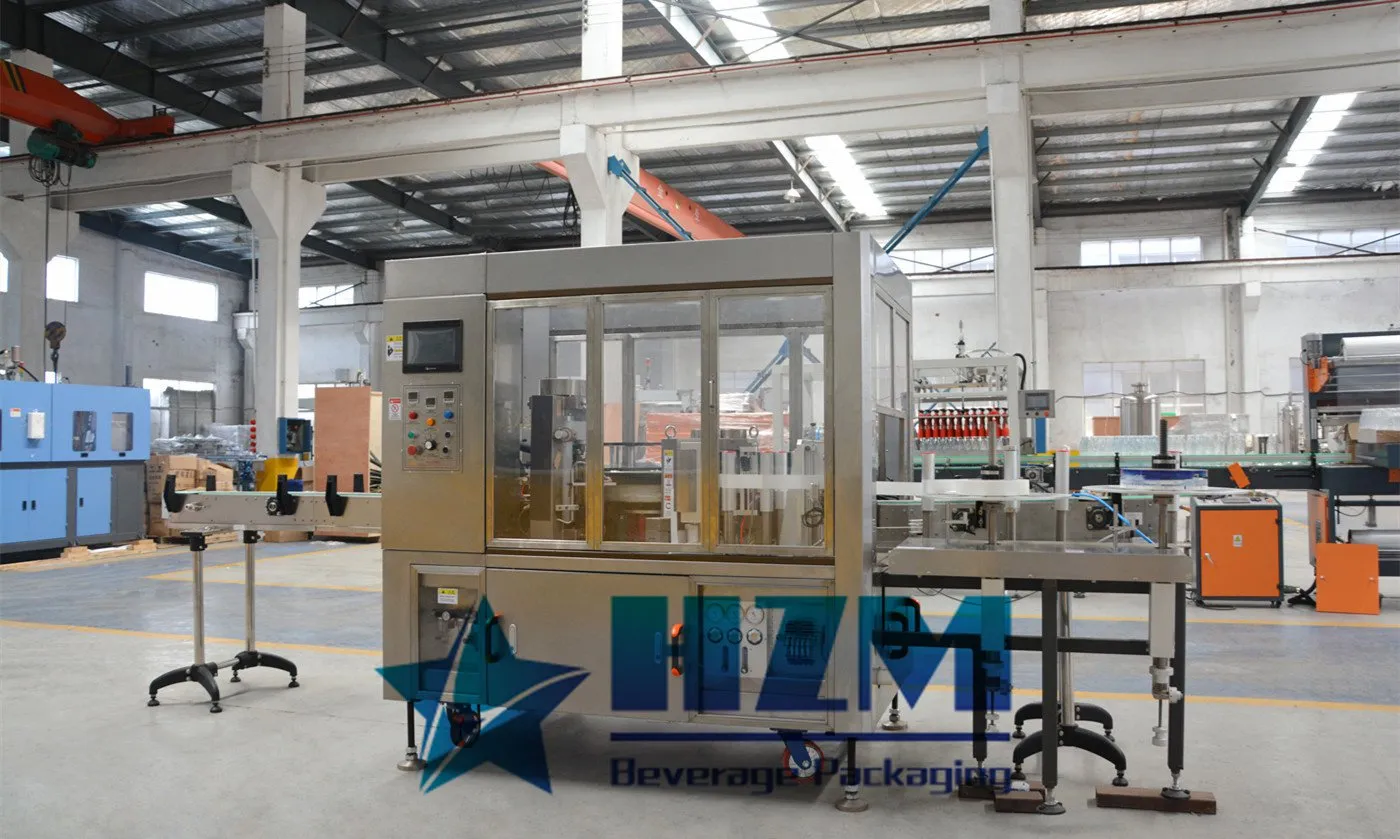
Equipment
Automatic Linear Type Hot Glue Labeling Machine
Linear hot-glue labelling for water and soft-drink bottles, using roll-fed OPP labels at 8,000–24,000 bottles/hour.
Learn more
Equipment
Automatic BOPP Hot Glue Labeling Machine
Rotary BOPP hot-glue labelling for beverage containers, with RG models from 8,000 to 24,000 bottles/hour.
Learn more
2025-10-24
Differences Between Hot Filling and Cold Filling in Beverage Filling Machines
In the field of beverage filling machines, Hot filling and Cold filling (also known as aseptic filling) are two core processes. Their fundamental differences lie in the product temperature during filling, sterilization logic, and applicable scenarios, which directly affect the beverage quality, shelf life, packaging costs, and equipment investment.
Learn more
2023-06-09
Juice and Tea Filling Line Guide: Product Temperature and Process Selection
Practical HZM guidance on juice and tea filling line, focused on product temperature and process selection, line integration, RFQ data and measurable acceptance checks.
Learn more2023-06-09
200-500ml Ultra-Clean Filling Machine
The ultra-clean filling production line adopts aseptic isolation technology and reliable sterilization methods. Bottles and caps undergo thorough sterilization before filling and sealing in an aseptic environment.
Learn more2023-06-09
Juice and Tea Filling Line Guide: FAT Checks for Fill Level and Temperature
Practical HZM guidance on juice and tea filling line, focused on fat checks for fill level and temperature, line integration, RFQ data and measurable acceptance checks.
Learn more2023-06-09
Enclosed Juice Filling Lines: Hygiene and Hot-Fill Design
A practical guide to enclosure, hygienic zoning, product-contact design, hot filling, cleaning and environmental control for juice filling lines.
Learn more
2023-06-09
Glass Bottle Filling Line Guide: Hot-Fill Temperature and Container Protection
Practical HZM guidance on glass bottle filling line, focused on hot-fill temperature and container protection, line integration, RFQ data and measurable acceptance checks.
Learn more