Insights & Updates
Compressed-Air Pressure Drops When the Bottling Line Speeds Up
Compressed-air pressure collapsing during peak line demand should be investigated before small losses become a repeat breakdown. Operators need a safe test sequence that protects product, preserves the original settings and proves the cause with measured data.
Controls and utility faults are best diagnosed from the load back toward the source. First determine whether the stop was commanded, protective, mechanical or caused by an unstable supply. In this case, pneumatic cylinders slow at target speed is the key observation to preserve. Use the guide to rank likely causes and document the restored condition.
Quick answer: Measure pressure at the machine while recording flow and compressor state. Check leaks, receiver capacity, filters and dryers, pipe restriction, compressor control and simultaneous high-demand events before raising the pressure setpoint.
What operators usually see
Before opening the machine, compare the visible and measured symptoms. Note whether each one is continuous, intermittent or tied to a specific station: For this case, preserve evidence that shows whether pneumatic cylinders slow at target speed.
- Pneumatic cylinders slow at target speed
- Capper or packer alarms appear together
- Header pressure is normal but machine pressure is low
- Compressor stays loaded without recovering the receiver
Make the equipment safe and protect the product
Electrical tests must be performed by qualified personnel using the site electrical-safety and lockout/tagout procedures. Release pneumatic pressure and verify stored energy before touching actuators.
Capture the first fault, timestamp, drive current, supply pressure or voltage, PLC state, interlock chain and machine condition before resetting anything. Repeated resets destroy useful evidence. Explicitly record whether pneumatic cylinders slow at target speed.
Most likely causes, in practical checking order
1. Demand exceeds available capacity
Simultaneous blowing, capping and packaging consumption is greater than delivered free air To test this explanation without guessing, log compressor discharge, receiver and point-of-use pressure on the same timeline Record the result before moving to the next cause.
2. Distribution pressure loss
Undersized pipe, long runs, filters, dryers and restrictions consume pressure at peak flow A practical confirmation step is to measure or estimate peak air demand by machine state. Compare the finding with a known-good run.
3. Large leaks or failed drains
Air is lost continuously or a drain sticks open Do not compensate for this condition in the recipe. First, perform an approved leak survey during production and shutdown Keep the original setting and measured result in the fault record.
4. Poor receiver or compressor control
Insufficient storage and a wide control delay cannot absorb short peaks Separate this cause from the others with one controlled check: check filter and dryer differential pressure and condensate drains Use the same product, format and speed for the comparison.
Step-by-step diagnostic procedure
Use the last known-good run as the baseline. If a check needs energized access or pressure exposure, use the manufacturer’s approved specialist procedure.
- Log compressor discharge, receiver and point-of-use pressure on the same timeline
- Measure or estimate peak air demand by machine state
- Perform an approved leak survey during production and shutdown
- Check filter and dryer differential pressure and condensate drains
- Inspect pipe size, isolation valves and local regulators
- Review compressor loading, sequencing and receiver volume with the utility supplier
Corrective actions that address the root cause
Apply a correction only to the cause demonstrated by the checks. Save the old parameter, removed part and measured condition for review.
- Repair leaks and failed drains
- Replace loaded filters and remove restrictions
- Add correctly engineered local storage or distribution capacity
- Correct compressor sequencing or capacity rather than masking loss with excessive pressure
How to verify the repair before full-speed production
Before releasing full-speed production, reproduce the operating condition that originally exposed the fault. Then complete this acceptance check: Confirm that compressed-air pressure collapsing during peak line demand is absent for multiple consecutive cycles, not only for one sample. Review the alarm history and keep diagnostic product segregated until the site’s quality procedure releases it.
- Confirm that compressed-air pressure collapsing during peak line demand is absent for multiple consecutive cycles, not only for one sample.
- Compare the repaired result for “Pneumatic cylinders slow at target speed” with the approved quality limit and the last known-good baseline.
- Check adjacent stations and downstream package quality for side effects associated with demand exceeds available capacity.
- For “Compressed-Air Pressure Drops When the Bottling Line Speeds Up”, record the final settings, measurements, parts used and restart authorization.
Prevent the problem from returning
Add the checks below to the operator, sanitation or preventive-maintenance standard and assign a measurable acceptance condition.
- Trend point-of-use pressure
- Perform periodic leak surveys
- Maintain filters, dryers and drains
- Sequence large pneumatic consumers
- Review air capacity before speed or equipment expansion
When to stop troubleshooting and call a specialist
Stop and contact the machine or component supplier when compressed-air pressure collapsing during peak line demand cannot be isolated with non-invasive checks, when it returns after an approved repair, or when calibration requires protected service tools. Escalate immediately for a damaged pressure boundary, uncontrolled motion, food-safety risk, exposed conductor or repeated protective trip. Send the service engineer the fault history, photos, samples, trend data, recipe revision and work already completed.
Relevant equipment for this application
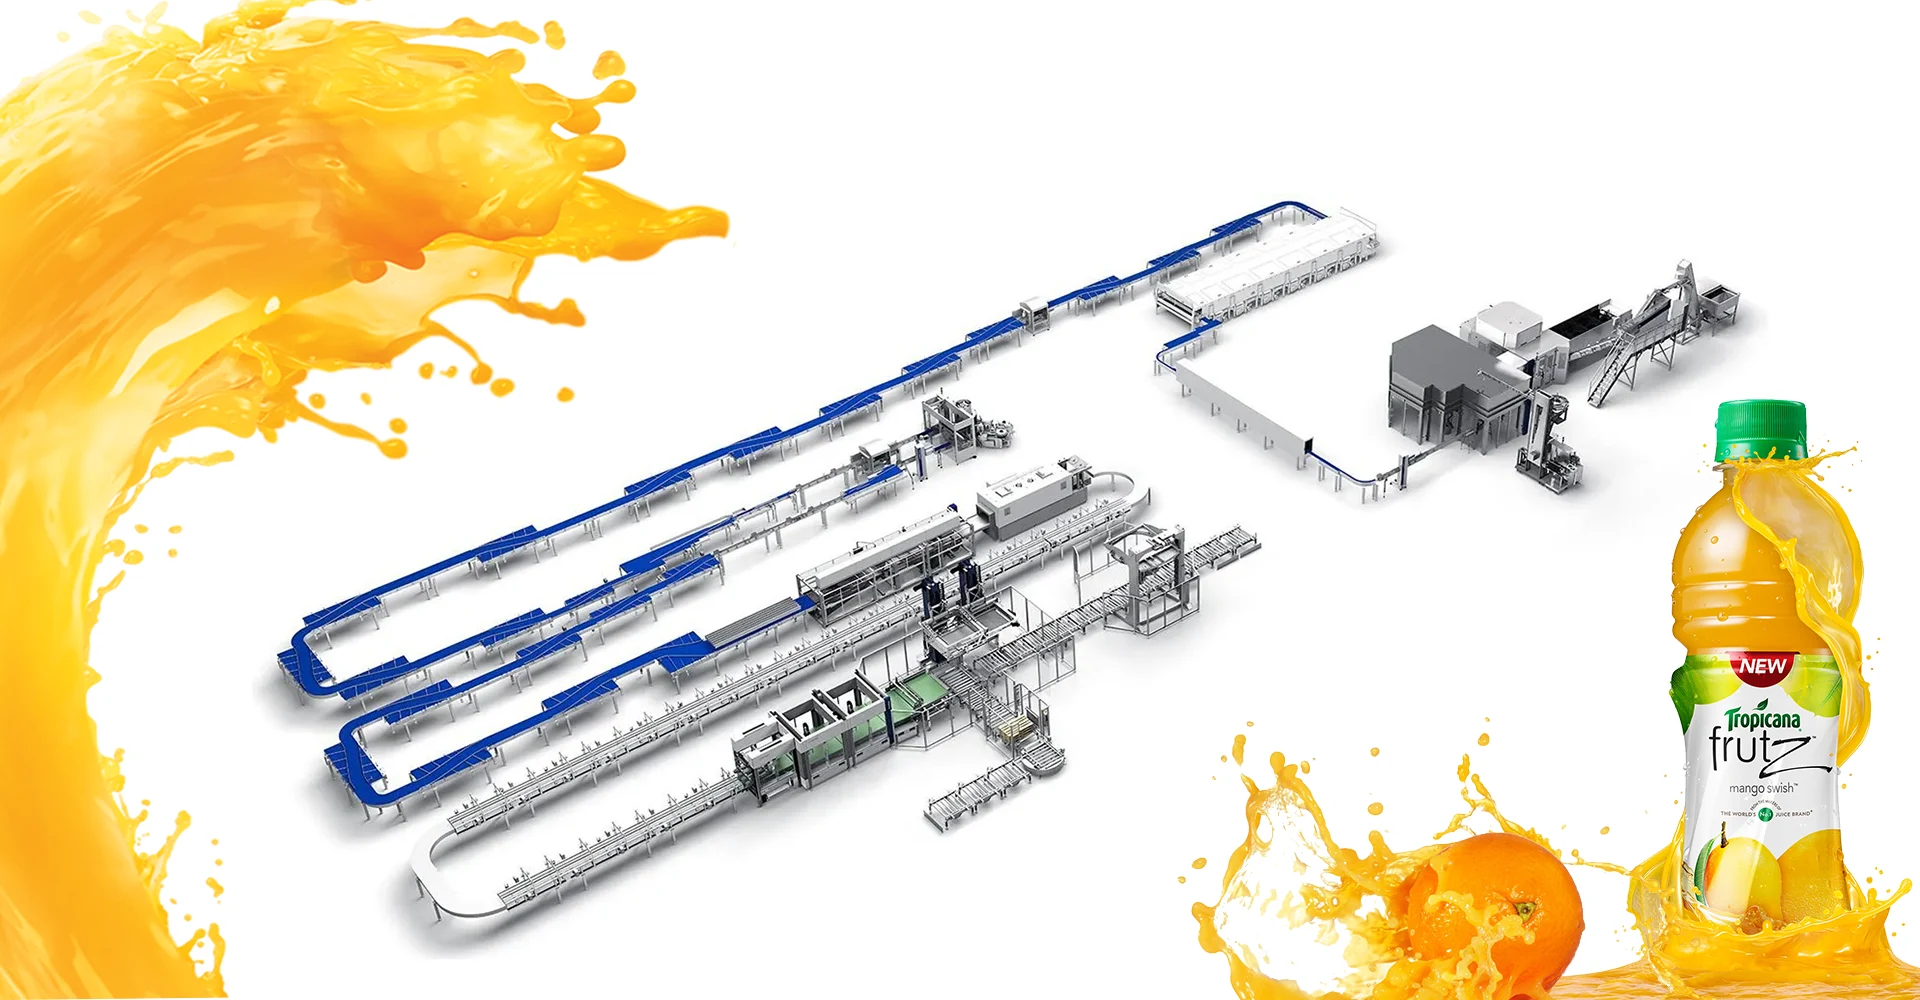
The site example most closely related to compressed-air pressure collapsing during peak line demand is the Beverage Filling Line – Juice, Water, Soft Drinks, cola, Beer. Equipment selection should be checked against samples, quality limits, required sustained output and available utilities.
Frequently asked questions
What should be checked first when compressed-air pressure collapsing during peak line demand?
Measure pressure at the machine while recording flow and compressor state. Check leaks, receiver capacity, filters and dryers, pipe restriction, compressor control and simultaneous high-demand events before raising the pressure setpoint. Preserve the original settings and take representative samples before repair work begins.
How can we distinguish demand exceeds available capacity from distribution pressure loss?
Simultaneous blowing, capping and packaging consumption is greater than delivered free air In contrast, undersized pipe, long runs, filters, dryers and restrictions consume pressure at peak flow Compare the two mechanisms under the same operating condition by completing these checks: log compressor discharge, receiver and point-of-use pressure on the same timeline Then measure or estimate peak air demand by machine state
Can production continue while compressed-air pressure collapsing during peak line demand?
Only when the plant’s documented risk assessment and quality procedure allow it. For compressed-air pressure collapsing during peak line demand, stop and segregate production when package integrity, sanitation, validated processing, pressure safety, electrical protection or an uncontrolled reject trend is involved.
What evidence will help the equipment supplier respond faster?
Provide the model and serial number, product and format, target speed, first fault, timestamps, photos or video, affected station pattern and maintenance history. For this issue, also include pneumatic cylinders slow at target speed and the measured result from this check: review compressor loading, sequencing and receiver volume with the utility supplier
Talk to our engineering team
Need help planning your packaging line?
Share your product, bottle and capacity requirements for a practical equipment recommendation.
Equipment
Bottle Air Conveyor
The bottle air conveyor transfers empty PET bottles from the blowing machine to the filler.
Learn more
2023-06-09
PET Blow Molding System Guide: High-Pressure Air Quality and Recovery
Practical HZM guidance on pet blow molding system, focused on high-pressure air quality and recovery, line integration, RFQ data and measurable acceptance checks.
Learn more
2026-08-03
PET Blow Molding Compressed Air Cost: A Practical Energy Audit
Find compressed-air waste in PET bottle production by measuring pressure, specific consumption, leakage, recovery and compressor loading by bottle SKU.
Learn more
2023-06-09
Blow-Fill-Cap Combi Block Guide: High-Pressure Air and Energy Planning
Practical HZM guidance on blow-fill-cap combi block, focused on high-pressure air and energy planning, line integration, RFQ data and measurable acceptance checks.
Learn more2023-07-12
Air conveyor systems
The air conveyor, also known as a pneumatic conveyor, serves the purpose of efficiently transporting empty bottles between machines within a filling line. It also acts as a buffer, allowing for automatic operation of the entire line. Primarily, it is employed to transfer empty PET bottles from the blowing machine to the filling machine, also known as the filler.
Learn more
2023-06-26
HZM Machinery: Leading in Bottle Air Conveyor Manufacturing
Bottle Air Conveyors, also known as pneumatic conveyors, play a crucial role in the beverage and food industries. HZM Machinery, a leading manufacturer of Bottle Air Conveyors, has gained recognition and acclaim in the industry for its exceptional quality, innovative technology, and outstanding customer service.
Learn more
2023-06-09
Glass Bottle Filling Line Guide: Pressure Control for Carbonated Beverages
Practical HZM guidance on glass bottle filling line, focused on pressure control for carbonated beverages, line integration, RFQ data and measurable acceptance checks.
Learn more