Coordinating Filler Speed with Product and Container Supply
A variable-frequency drive changes motor speed within the machine’s permitted operating range. It does not automatically coordinate carbonation, pressure control or bottle accumulation. These functions must follow the engineered machine sequence.

Observe the whole speed change
Trend filler speed, product level and pressure together. Inspect bottle spacing and the transfer to capping as the line accelerates or slows. A stable motor command can coexist with unstable product supply.
Accept a usable operating range
Check quantity, foam and closure at the agreed low and normal rates, including restart. Save only settings verified for the particular format. Avoid raising speed to overcome an unresolved upstream shortage or downstream blockage.
Need help planning your packaging line?
Share your product, bottle and capacity requirements for a practical equipment recommendation.
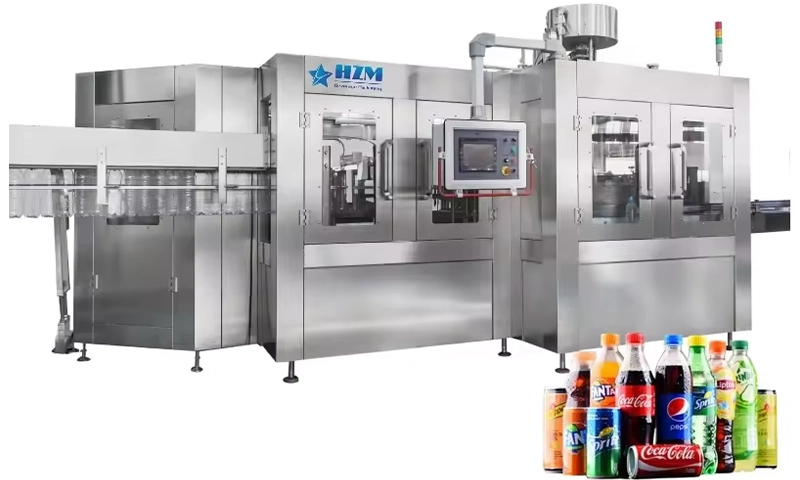
Carbonated Soft Drink Filling Machine
Carbonated soft drink rinsing, isobaric filling and capping, with DXGF models from 3,000 to 15,000 bottles/hour at 500 ml.
Learn more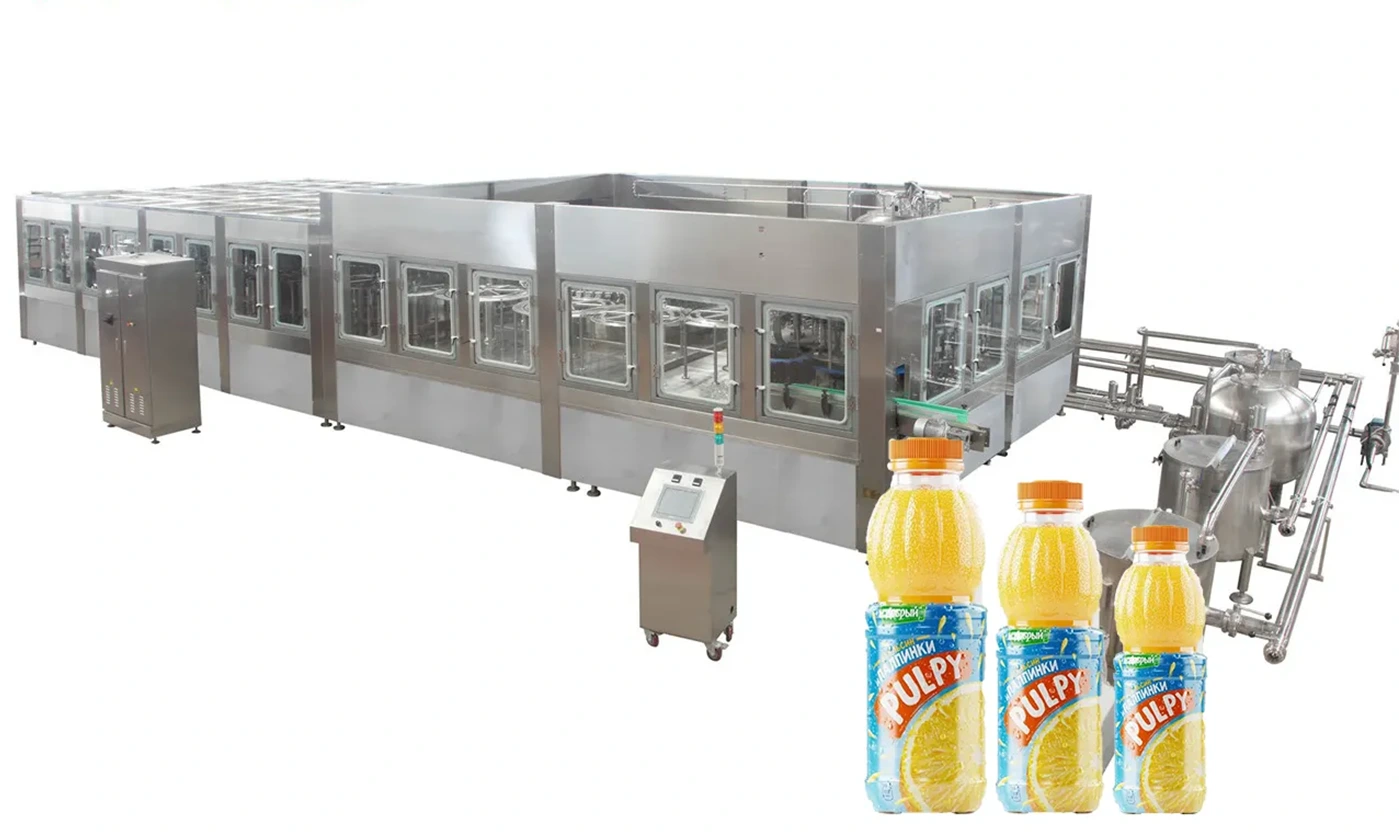
Fully Automatic Beverage Filling Machine
The fully automatic beverage filling machine combines bottle rinsing, filling and capping.
Learn more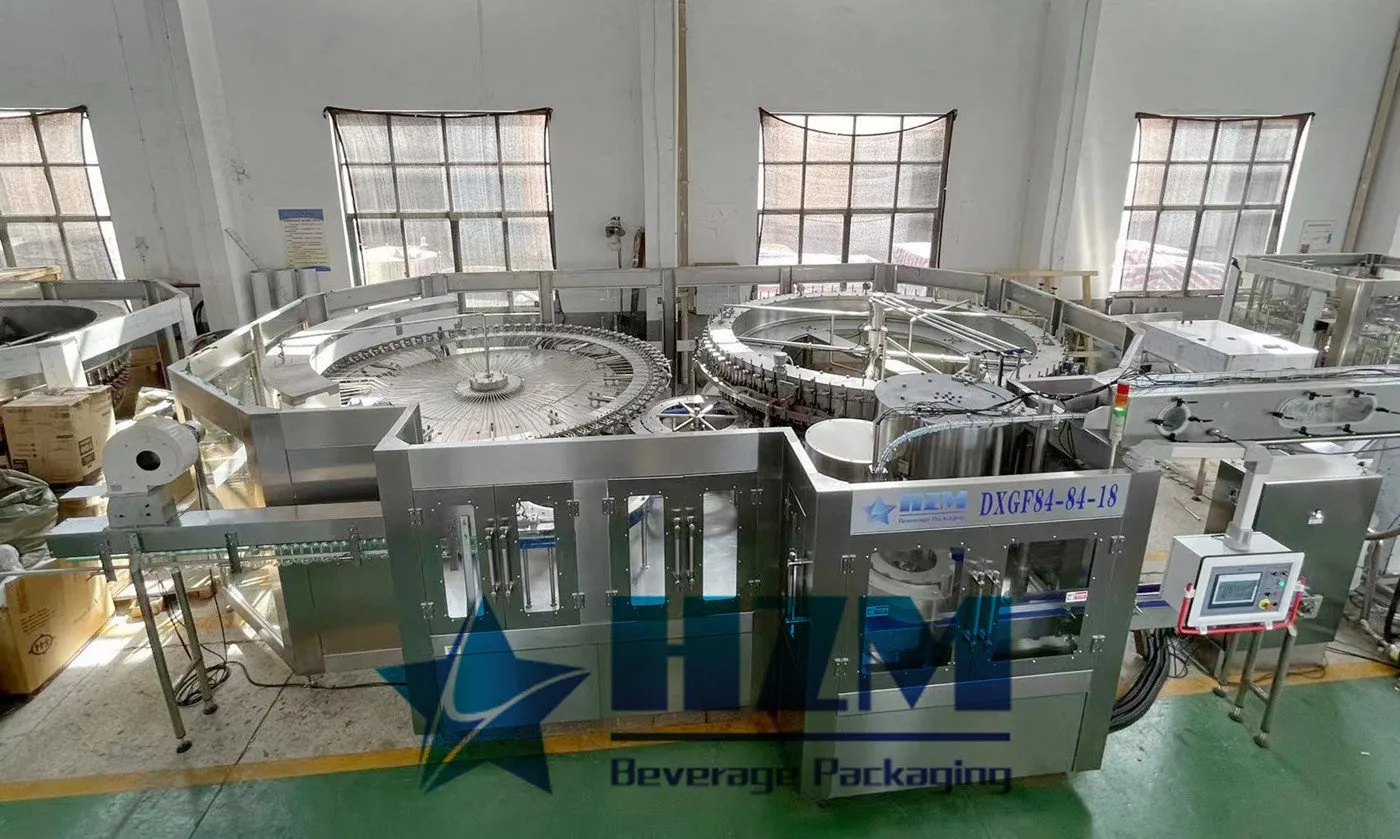
Carbonated Drinks Filling Machine
Carbonated drink rinsing, isobaric filling and capping for PET bottles, with capacities of 4,000–36,000 bottles/hour at 500 ml.
Learn more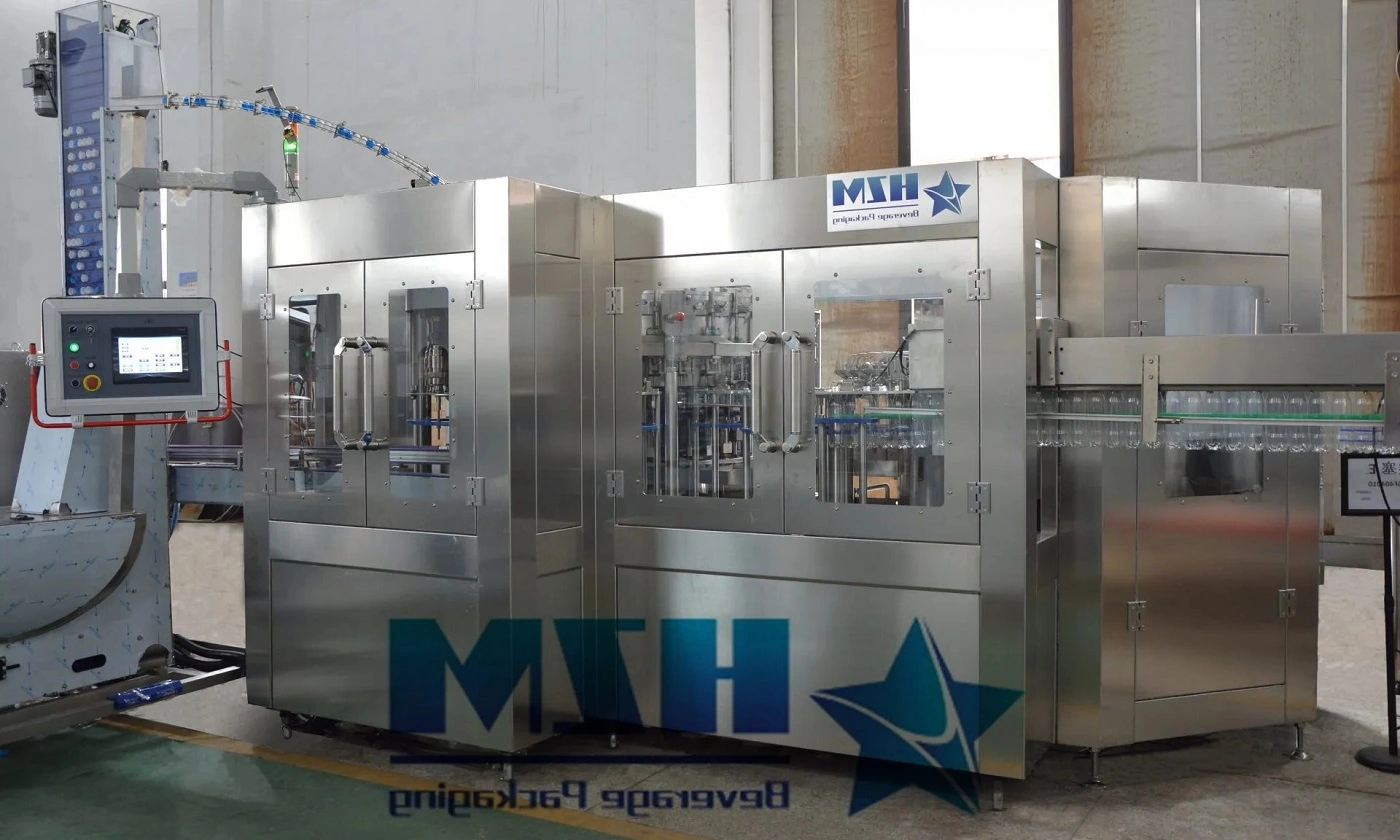
Soft Drinks Sparkling Water Filling Machine
PET bottle filling for soft drinks and sparkling water, combining rinsing, counter-pressure filling and capping.
Learn more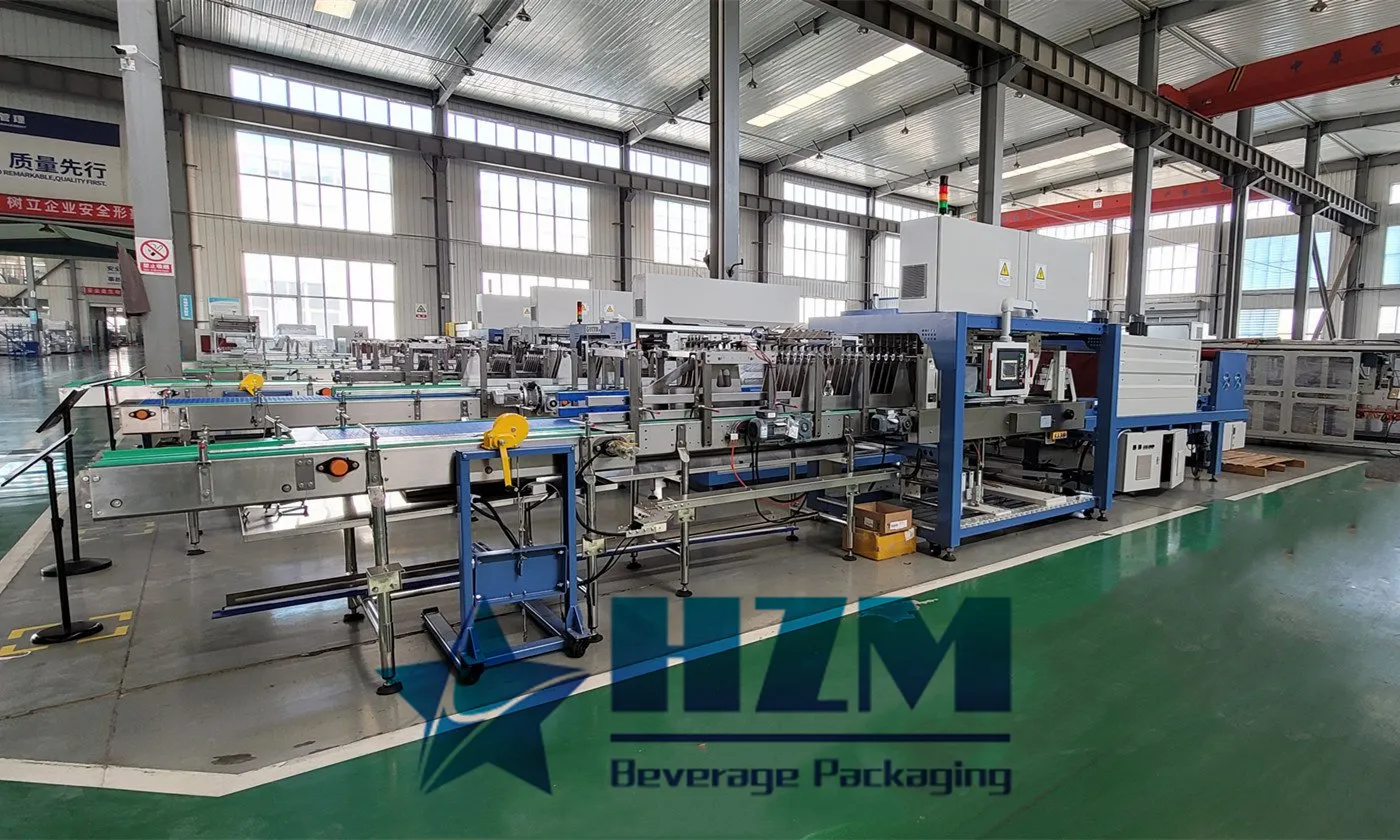
Automatic Beverage Packaging Machines – Juice, Soda & Soft Drinks
HZM beverage packaging equipment connects juice, soda and soft drink filling with labelling, coding and secondary packaging.
Learn more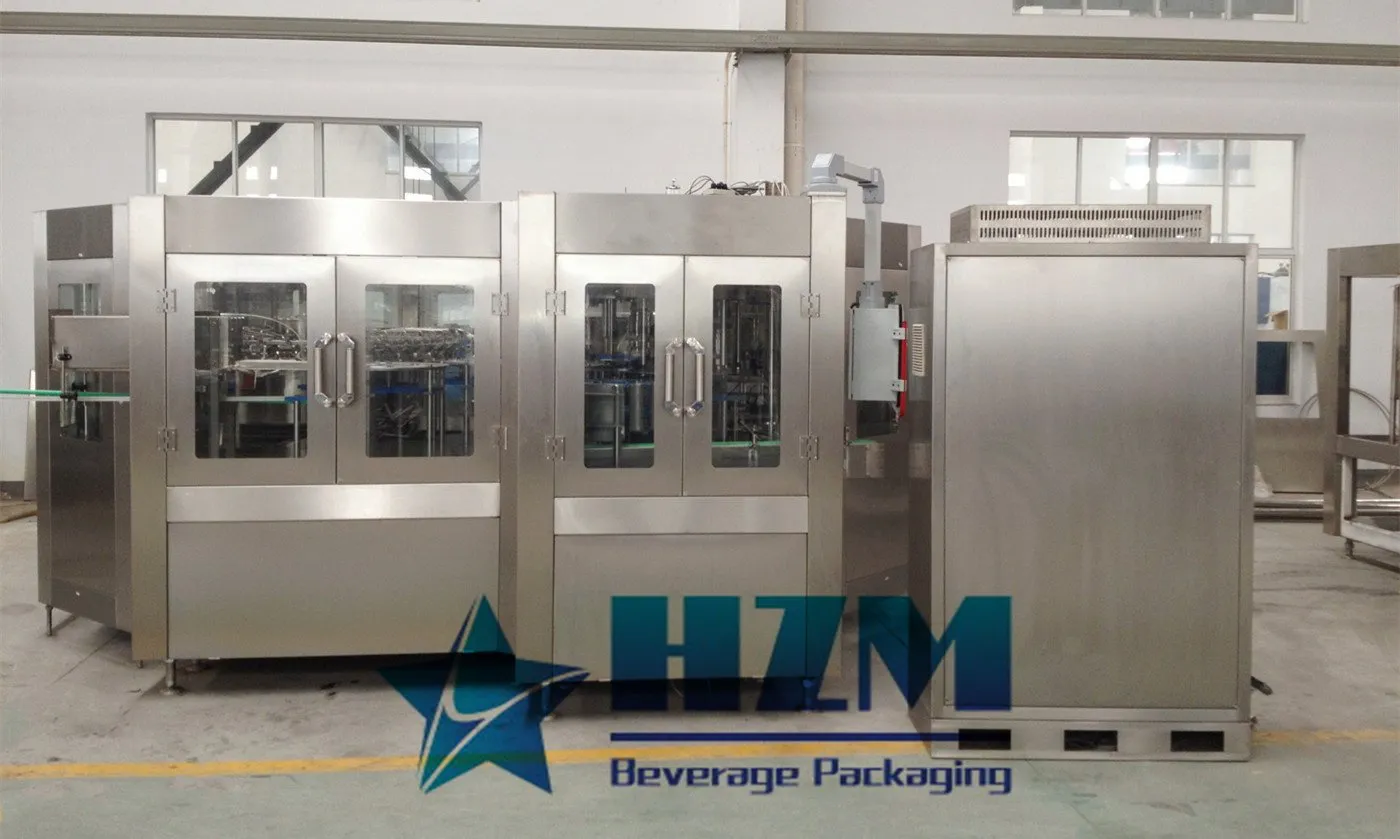
PET Bottle CSD Beverage Filling Machine
Automatic PET bottle rinsing, isobaric filling and capping for cola, soda water and other carbonated soft drinks.
Learn more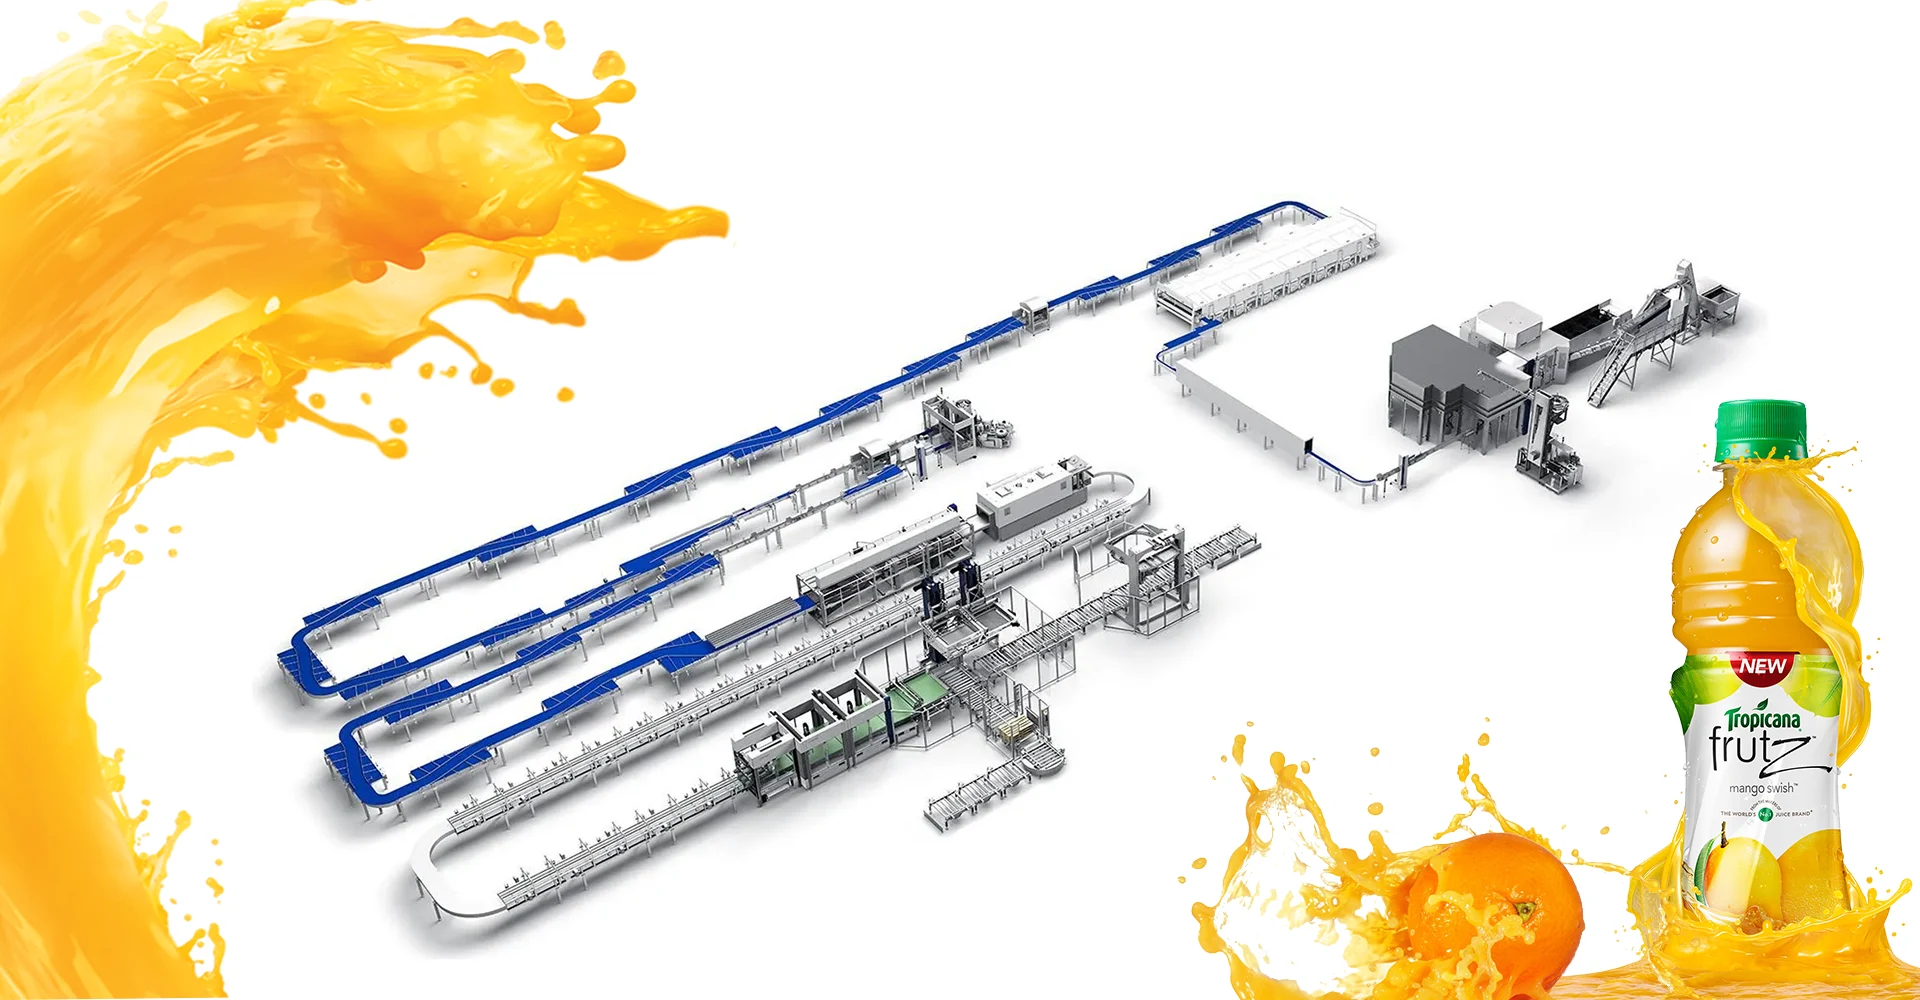
Beverage Filling Machine & Turnkey Filling Line for Juice, Soft Drinks and Cans
Beverage filling machines and turnkey lines for juice, soft drinks, water and beer in PET bottles, glass bottles or cans.
Learn more
Soda Water Filling Machine
Soda water filling equipment with bottle rinsing, isobaric filling and capping for PET-bottled sparkling water.
Learn more
Beverage Packaging Machine for Juice, Soft Drinks, Carbonated Drinks, and Energy Drink
HZM supplies beverage production and packaging equipment for juice, soft drinks, carbonated drinks and energy drinks.
Learn moreFilling Carbonated Drinks in Small PET Bottles
Small bottles still require controlled pressure filling and a compatible neck-and-cap combination.
Learn moreBeer Production Line 200ml Carbonated Soft Drink Filling Machine
High quality Beer Production Line 200ml Carbonated Soft Drink Filling Machine from China, China's leading 200ml Carbonated Soft Drink Filling Machine product, with strict quality control 200ml Beer Production Line factories, producing high quality 54000 BPH Carbonated Soft Drink Filling Machine products.
Learn moreSpecifying an 8,000-Bottle Carbonated Filling Duty
An 8,000 bottles-per-hour target needs a bottle volume and defined beverage conditions.
Learn moreTurning a Carbonated Filler Output Target into a Test
A target such as 24,000 bottles per hour is a production requirement until it is tied to a named configuration and test conditions.
Learn more
Choosing a Labeling System from the Label and Container
A labeling system includes container presentation, label feed, application and inspection.
Learn more28000 BPH SS316 Carbonated Soft Drink Filling Machine For Sale
This top-of-the-line filling machine boasts an impressive 28,000 bottles per hour (BPH) output, making it ideal for large-scale beverage production. Constructed from durable SS316 stainless steel, it's built to handle the demands of high-volume carbonated soft drink filling with precision and efficiency.
Learn more