Insights & Updates
PET Bottles Fall Over on the Conveyor
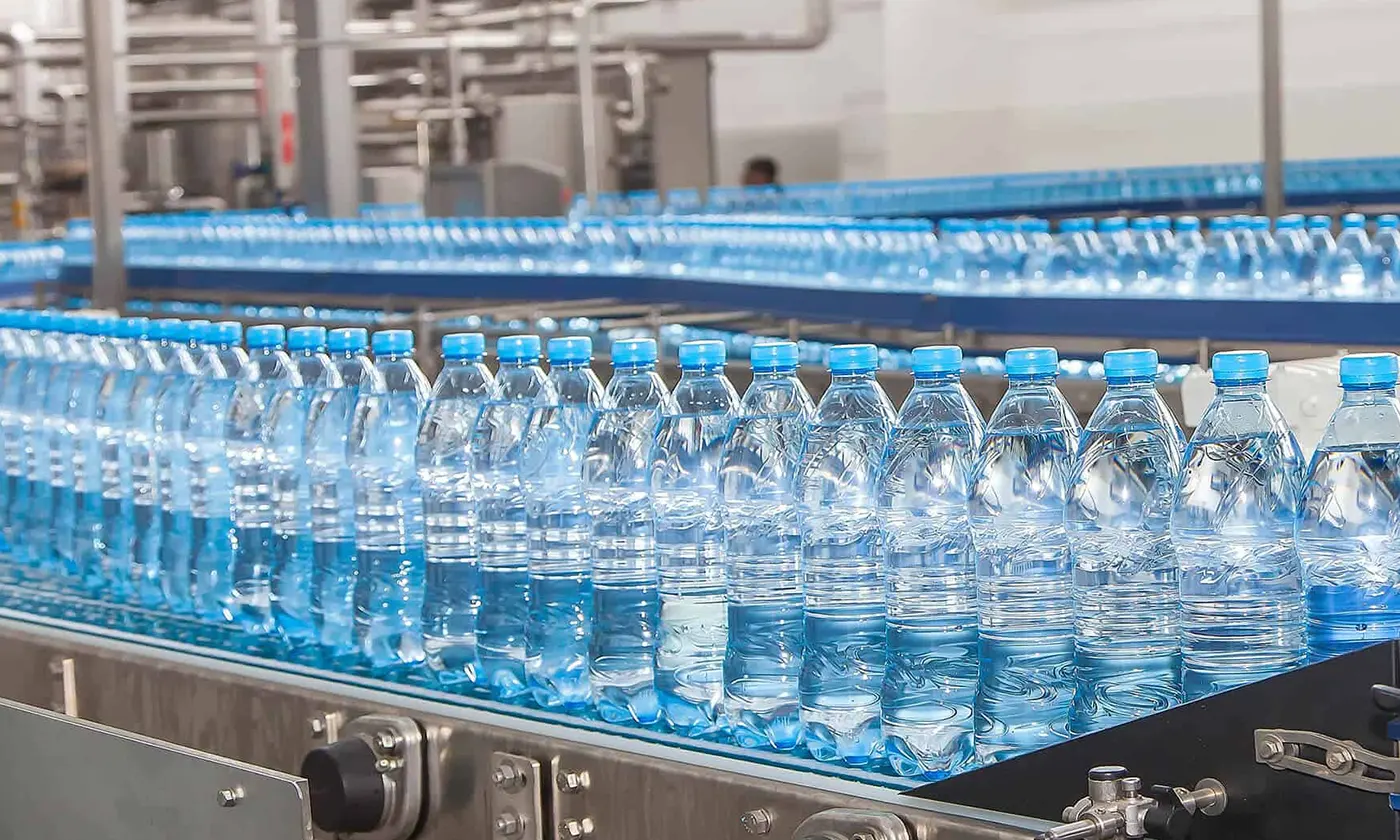
PET bottles tipping or falling during conveying should be investigated before small losses become a repeat breakdown. Operators need a safe test sequence that protects product, preserves the original settings and proves the cause with measured data.
A conveyor problem should be treated as a line-balance problem as well as a mechanical one. Container geometry, guide settings, chain condition, lubrication, accumulation pressure, sensor logic and adjacent machine speeds all matter. In this case, empty bottles tip more often than filled bottles is the key observation to preserve. Use the guide to rank likely causes and document the restored condition.
Quick answer: Evaluate bottle stability, fill level, base shape, guide height and clearance, conveyor speed transitions, air movement and accumulation. Lightweight bottles need controlled support without being squeezed.
What operators usually see
Before opening the machine, compare the visible and measured symptoms. Note whether each one is continuous, intermittent or tied to a specific station: For this case, preserve evidence that shows whether empty bottles tip more often than filled bottles.
- Empty bottles tip more often than filled bottles
- Falling starts at curves or speed transitions
- Bottles rock on their bases
- Guide rails leave dents in thin sidewalls
Make the equipment safe and protect the product
Stop and lock out the affected conveyor and adjacent machines before clearing containers, adjusting guides, touching chains or testing a drive. Never defeat interlocks to observe a jam from inside a guarded zone.
Mark the exact jam location and record line speed, container format, guide clearance, chain current, lubrication status, accumulation state and upstream/downstream machine conditions. Explicitly record whether empty bottles tip more often than filled bottles.
Most likely causes, in practical checking order
1. Unstable bottle geometry
Poor base formation, high center of gravity or ovality reduces the restoring margin To test this explanation without guessing, map the first tipping point and note empty or filled condition Record the result before moving to the next cause.
2. Guide height or clearance wrong
Rails contact a flexible panel or leave too much space for lean A practical confirmation step is to check bottle base rock, perpendicularity and cavity pattern. Compare the finding with a known-good run.
3. Abrupt acceleration or curve force
Speed steps and tight radii create lateral force above the base Do not compensate for this condition in the recipe. First, measure guide height and clearance with actual tolerance-limit bottles Keep the original setting and measured result in the fault record.
4. Air or accumulation disturbance
Blower drafts and backpressure move lightweight containers unpredictably Separate this cause from the others with one controlled check: trend conveyor speeds through transitions and curves Use the same product, format and speed for the comparison.
Step-by-step diagnostic procedure
Use the last known-good run as the baseline. If a check needs energized access or pressure exposure, use the manufacturer’s approved specialist procedure.
- Map the first tipping point and note empty or filled condition
- Check bottle base rock, perpendicularity and cavity pattern
- Measure guide height and clearance with actual tolerance-limit bottles
- Trend conveyor speeds through transitions and curves
- Observe accumulation and nearby air jets or fans
- Run controlled speed steps to identify the stability threshold
Corrective actions that address the root cause
Apply a correction only to the cause demonstrated by the checks. Save the old parameter, removed part and measured condition for review.
- Correct bottle blow or incoming-container quality
- Set guide rails to stable non-compressive contact
- Smooth acceleration and synchronize adjacent conveyors
- Reduce harmful air and accumulation forces
How to verify the repair before full-speed production
Before releasing full-speed production, reproduce the operating condition that originally exposed the fault. Then complete this acceptance check: Confirm that pet bottles tipping or falling during conveying is absent for multiple consecutive cycles, not only for one sample. Review the alarm history and keep diagnostic product segregated until the site’s quality procedure releases it.
- Confirm that pet bottles tipping or falling during conveying is absent for multiple consecutive cycles, not only for one sample.
- Compare the repaired result for “Empty bottles tip more often than filled bottles” with the approved quality limit and the last known-good baseline.
- Check adjacent stations and downstream package quality for side effects associated with unstable bottle geometry.
- For “PET Bottles Fall Over on the Conveyor”, record the final settings, measurements, parts used and restart authorization.
Prevent the problem from returning
Add the checks below to the operator, sanitation or preventive-maintenance standard and assign a measurable acceptance condition.
- Qualify bottle stability before lightweighting
- Use format gauges for guides
- Trend tip-over locations
- Control speed ramps
- Link blower-cavity rejects with conveyor events
When to stop troubleshooting and call a specialist
Stop and contact the machine or component supplier when pet bottles tipping or falling during conveying cannot be isolated with non-invasive checks, when it returns after an approved repair, or when calibration requires protected service tools. Escalate immediately for a damaged pressure boundary, uncontrolled motion, food-safety risk, exposed conductor or repeated protective trip. Send the service engineer the fault history, photos, samples, trend data, recipe revision and work already completed.
Relevant equipment for this application
The site example most closely related to pET bottles tipping or falling during conveying is the Conveyor Belt System For PET Bottle And GLASS Bottle. Equipment selection should be checked against samples, quality limits, required sustained output and available utilities.
Frequently asked questions
What should be checked first when pET bottles tipping or falling during conveying?
Evaluate bottle stability, fill level, base shape, guide height and clearance, conveyor speed transitions, air movement and accumulation. Lightweight bottles need controlled support without being squeezed. Preserve the original settings and take representative samples before repair work begins.
How can we distinguish unstable bottle geometry from guide height or clearance wrong?
Poor base formation, high center of gravity or ovality reduces the restoring margin In contrast, rails contact a flexible panel or leave too much space for lean Compare the two mechanisms under the same operating condition by completing these checks: map the first tipping point and note empty or filled condition Then check bottle base rock, perpendicularity and cavity pattern
Can production continue while pET bottles tipping or falling during conveying?
Only when the plant’s documented risk assessment and quality procedure allow it. For pET bottles tipping or falling during conveying, stop and segregate production when package integrity, sanitation, validated processing, pressure safety, electrical protection or an uncontrolled reject trend is involved.
What evidence will help the equipment supplier respond faster?
Provide the model and serial number, product and format, target speed, first fault, timestamps, photos or video, affected station pattern and maintenance history. For this issue, also include empty bottles tip more often than filled bottles and the measured result from this check: run controlled speed steps to identify the stability threshold
Talk to our engineering team
Need help planning your packaging line?
Share your product, bottle and capacity requirements for a practical equipment recommendation.
Equipment
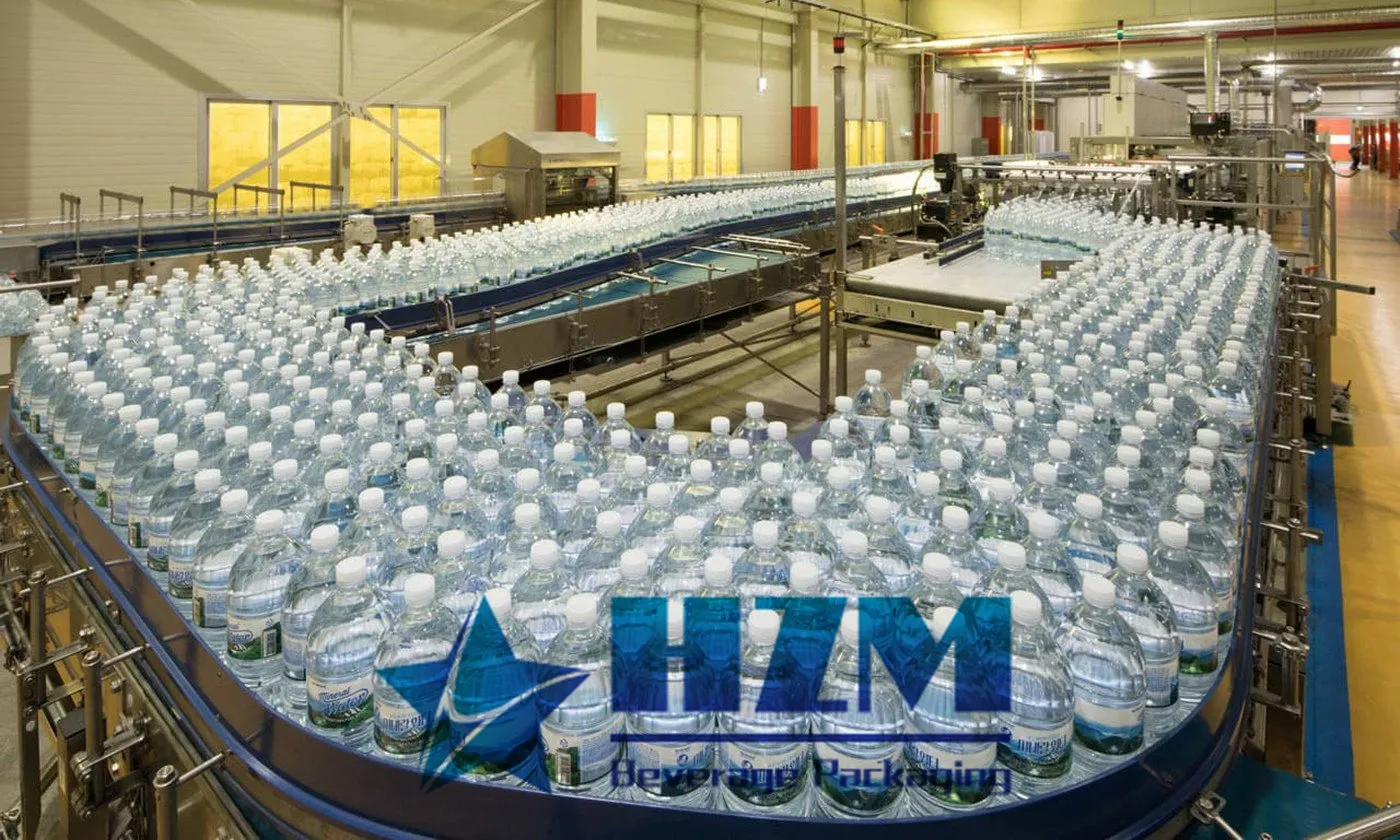
Bottle Conveyor
The bottle conveyor transfers containers between filling, labelling and packing machines.
Learn more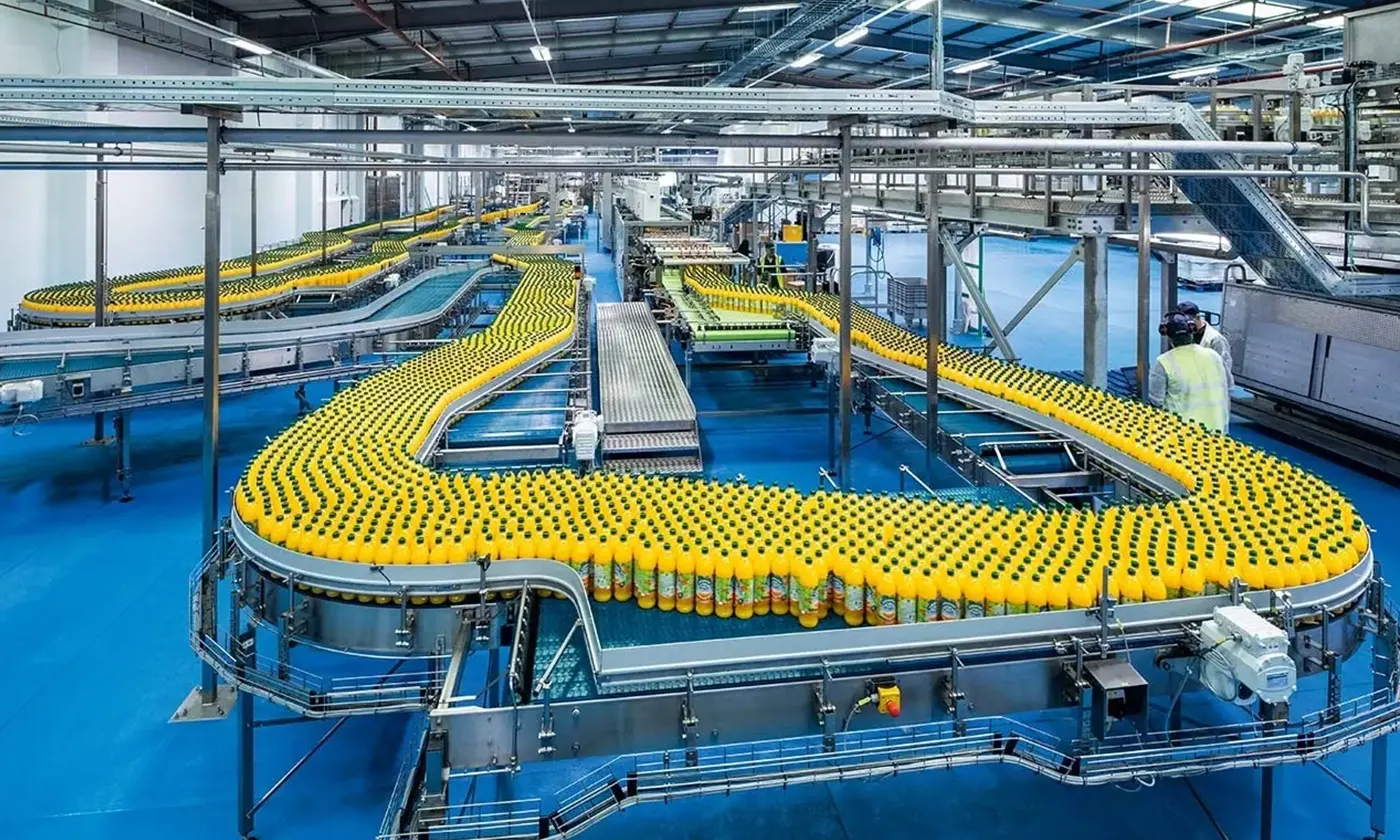
Equipment
Bottle Water & Beverage Conveyor System
The bottled-water and beverage conveyor system connects container supply, filling and packaging.
Learn moreEquipment
Conveyor Belt System For PET Bottle And GLASS Bottle
The conveyor system transfers PET and glass bottles between production machines.
Learn more
Equipment
Packs Conveyor
The packs conveyor moves finished packs, cartons and other packaged products between packing and handling stations.
Learn more
Equipment
Bottle Air Conveyor
The bottle air conveyor transfers empty PET bottles from the blowing machine to the filler.
Learn more
Equipment
Conveyor Belt For Bottle Water Production Line
This conveyor belt system moves bottles through a bottled-water production line, from empty-bottle feeding to filled-bottle labelling and packing.
Learn more2023-07-13
bottle conveyor
A bottle conveyor is a specialized manufacturing equipment utilized in factories and bottling plants to facilitate the smooth transportation of bottles. While sharing similarities with standard conveyor belts, the design of a bottle conveyor is tailored specifically to hold bottles upright and prevent spills
Learn more
2023-07-06
Your Reliable Conveyor Machine Manufacturer
In modern industrial production, Conveyor Machines are indispensable for efficient material transportation and automated production. When seeking a trusted manufacturer, HZM Machinery stands out as a reliable partner.
Learn more2023-07-12
Air conveyor systems
The air conveyor, also known as a pneumatic conveyor, serves the purpose of efficiently transporting empty bottles between machines within a filling line. It also acts as a buffer, allowing for automatic operation of the entire line. Primarily, it is employed to transfer empty PET bottles from the blowing machine to the filling machine, also known as the filler.
Learn more2026-08-20
Bottle Conveyor Jams at the Same Location Every Shift
Mark the first contact point and inspect guide transitions, chain condition, dead plates, speed change, bottle dimensions, lubrication and upstream accumulation. The pile-up often occurs downstream of the actual interference. Follow this practical fault-isolation, repair and prevention guide for bottling-line operators and maintenance teams.
Learn more2026-09-11
Conveyor VFD Trips on Overcurrent: Electrical or Mechanical?
Record the exact fault and operating state before reset. With qualified electrical personnel, separate mechanical binding and acceleration load from motor, cable, parameter, supply and drive faults. Follow this practical fault-isolation, repair and prevention guide for bottling-line operators and maintenance teams.
Learn more
2023-06-25
The Diverse Applications of Bottle Conveyors in Various Industries
In many industries, bottle conveyors are widely employed to efficiently transport bottles and enhance production efficiency. As a professional manufacturer specializing in bottle conveyors, HZM Machinery not only demonstrates outstanding product quality but also plays a significant role in multiple industries' applications.
Learn more