Insights & Updates
Beverage Can Filling Line Guide: Counter-Pressure Filling and Foam Control
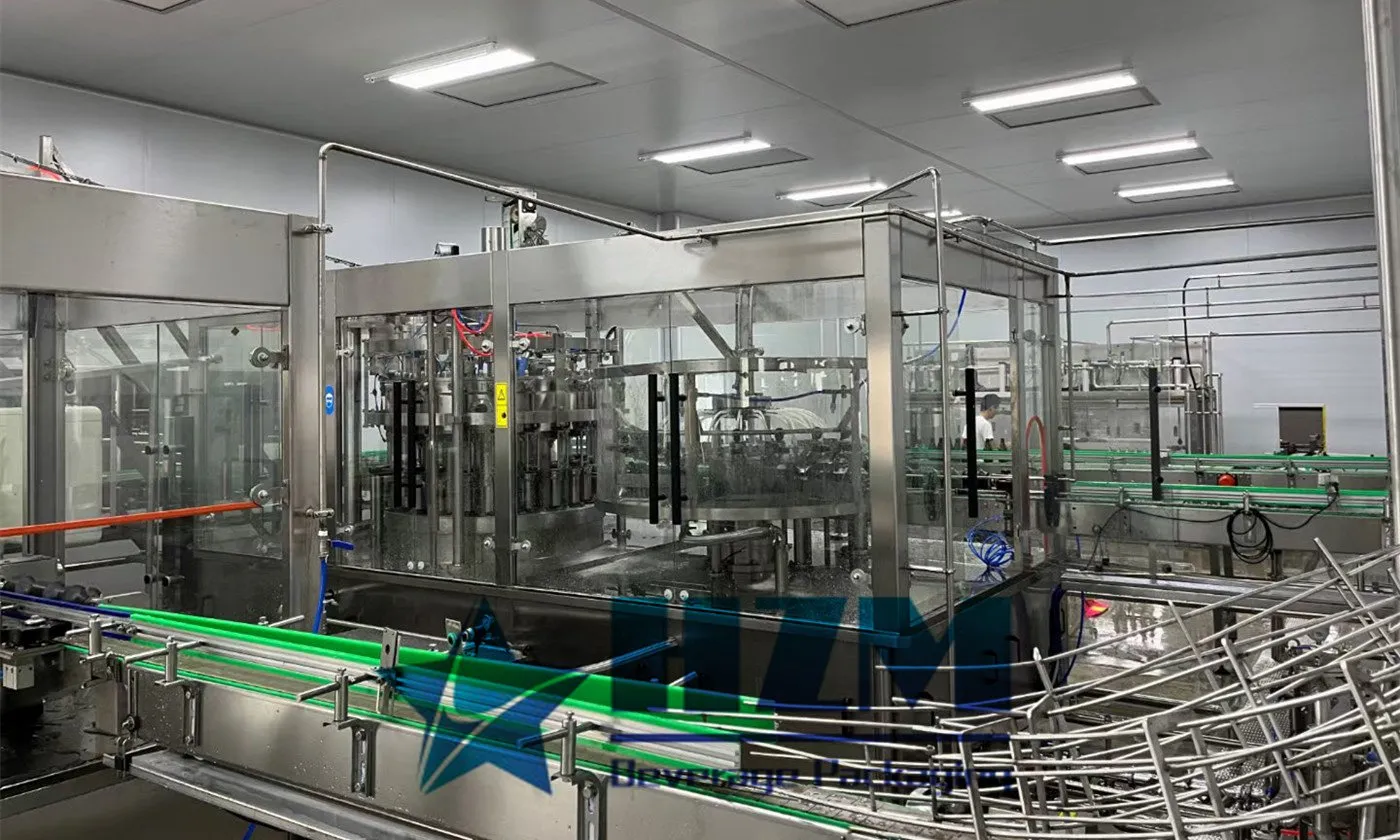
A reliable beverage can filling line project starts with verified application data, not a model code or an unsupported certificate list. This guide focuses on counter-pressure filling and foam control and shows what a buyer should define before HZM Machinery confirms the process, equipment scope and acceptance conditions.
Key procurement takeaways
- Define product, container, closure and saleable output before comparing machine models.
- Confirm the complete line boundary, utilities and downstream pack format in the RFQ.
- Use samples and measurable FAT conditions instead of broad marketing claims.
- Reserve access, training, spare parts and ramp-up time in the project plan.
Define the application before equipment selection
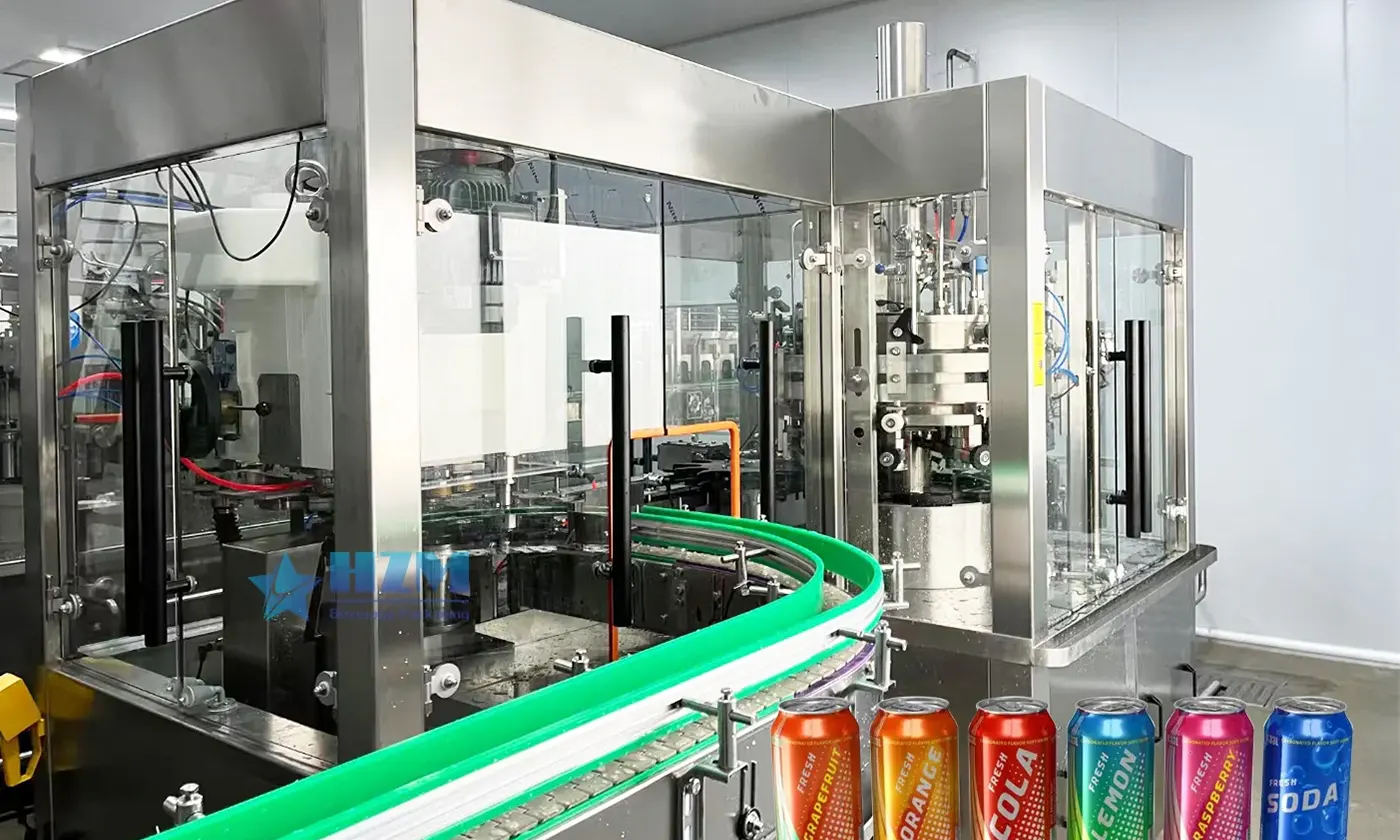
A canning line combining clean can transfer, controlled filling, seaming, inspection, coding and secondary packaging. The final configuration depends on the customer product, packaging samples, factory conditions and required automation. HZM therefore reviews the following inputs before issuing a technical proposal.
- Required net output by can size
- Seamer inspection method
- Tray, film or carton pack format
- Can body and end specifications
- Required net output by can size
Counter-Pressure Filling and Foam Control
Tie the engineering decision to product data, physical samples and an agreed acceptance method. HZM reviews these inputs before confirming the final process route, machine configuration and interfaces.
The specification should state who supplies each interface, how the line will respond to short stops, and which readings must be available to operators. This avoids gaps between process equipment, the main machine, conveyors and packaging, especially when several suppliers are involved.
Place the machine inside a complete production line
For equipment-level information, review Aluminum Can Filling Machine. The Cans Filling Production Line page shows the wider line sequence, while 36,000 BPH Carbonated Drink Production Line in Europe provides context from an actual HZM project. These references help define scope, but the quotation must still be based on the buyer’s current samples and user requirement specification.
| Decision point | Why it matters | What to provide |
|---|---|---|
| Product and hygiene | Determines process route, contact materials and cleaning method. | Required net output by can size |
| Container and closure | Controls handling, change parts and inspection requirements. | Seamer inspection method |
| Output and interfaces | Sets machine balance, buffers, utilities and acceptance targets. | Tray, film or carton pack format |
RFQ and acceptance checklist
- Send current product data, container and closure drawings, plus representative samples when available.
- State net saleable output for every SKU and define the efficiency formula used to convert rated speed into accepted production.
- Mark the supply boundary for process equipment, utilities, inspection, conveyors, packaging, coding and pallet handling.
- Agree the FAT material quantity, test duration, sampling plan, reject definitions and documented results before manufacturing is complete.
- Confirm installation responsibilities, operator and maintenance training, spare parts, manuals and after-sales communication.
Frequently asked questions
What information is required for a reliable quotation?
At minimum, provide product properties, package drawings, closure details, net output, factory layout, utilities and the desired line boundary. Physical samples are strongly recommended before change parts or handling components are finalized.
Is catalog speed the same as daily production?
No. Daily output also depends on changeovers, cleaning, upstream supply, downstream stops, rejects and operator practices. The proposal should distinguish rated speed, test speed and the efficiency target used for line acceptance.
Can one system handle several products or container sizes?
Often yes, but the range must be reviewed. Product risk, filling method, cleaning needs, container geometry and closure type determine whether change parts, additional circuits or separate equipment are required.
Discuss your project with HZM
Send the application data above for a configuration and quotation tied to your actual production plan. Get Quotes And Specifications
Talk to our engineering team
Need help planning your packaging line?
Share your product, bottle and capacity requirements for a practical equipment recommendation.
Equipment
Aluminum Can Filling Machine
This Aluminum Can Filling Machine is configured for carbonated Beverage, Beer, COLA, Gas Water at 4000–36000 Bottles Per Hour; final scope follows the approved…
Learn more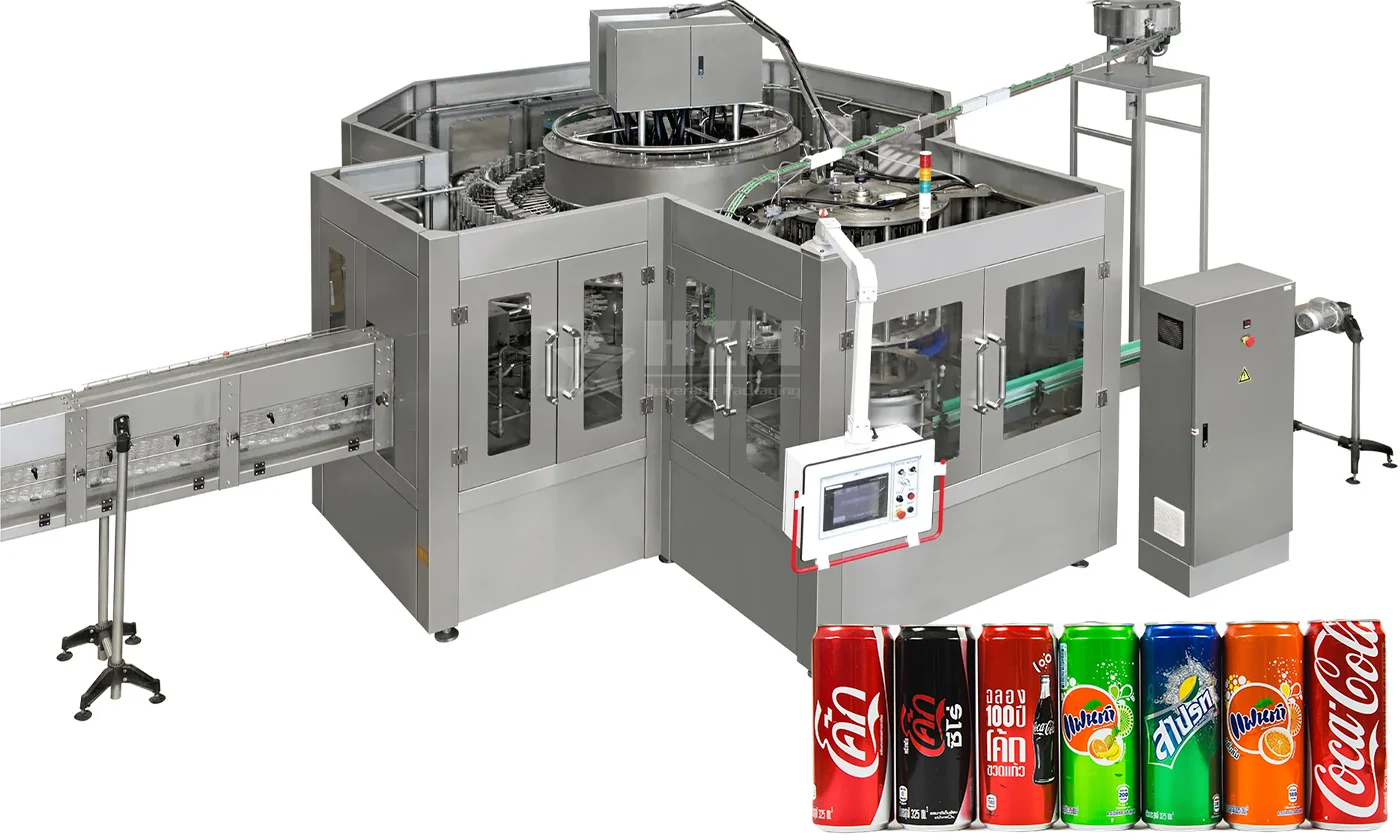
Equipment
Carbonated Beverage Can Filling Machine
This Carbonated Beverage Can Filling Machine is configured for carbonated Beverage, Beer, Soft Drink; final scope follows the approved process, package and plant layout.
Learn more
Equipment
Beverage Filling Machine & Turnkey Filling Line for Juice, Soft Drinks and Cans
This Beverage Filling Machine & Turnkey Filling Line for Juice is configured for juice, tea, carbonated soft drinks, energy drinks, water and beer at…
Learn more
Equipment
Bottled Water Filling Machine & Turnkey Water Bottling Line
This Bottled Water Filling Machine & Turnkey Bottling Line is configured for purified water, mineral water and still drinking water at 5,000–42,000 bottles/hour; final…
Learn more
2026-09-04
RO Differential Pressure Keeps Rising: Fouling Location Matters
Locate the stage where pressure loss is increasing and relate it to normalized flow and salt passage. A first-stage rise often points to particulate or biological fouling; a later-stage rise can indicate scale, but feed analysis is required. Follow this practical fault-isolation, repair and prevention guide for bottling-line operators and maintenance teams.
Learn more
2026-09-02
Custom Plastic and Hardware Components Used in Beverage Packaging Machinery
Learn how plastic injection molded parts and custom hardware components are selected, manufactured and inspected for beverage filling and packaging machinery.
Learn more
2026-09-02
How to Plan Safe Access for Beverage Production Line Installation and Maintenance
Practical guidance on planning operating platforms, walkways and temporary access for beverage production line installation, inspection, cleaning and maintenance.
Learn more
2026-09-02
Why Do Filling Valves Drip After the Bottle Leaves?
Dripping usually comes from contamination on the valve seat, worn or swollen seals, trapped pressure, incorrect closing timing or product viscosity outside the setup window. Identify whether the leak follows one valve or the entire filler. Follow this practical fault-isolation, repair and prevention guide for bottling-line operators and maintenance teams.
Learn more
2026-08-28
Sleeve Labels Wrinkle After the Shrink Tunnel
Determine whether the sleeve was straight before entering the tunnel. Then check film shrink curve, tunnel-zone temperature, airflow or steam distribution, bottle moisture, conveyor speed and container geometry. Follow this practical fault-isolation, repair and prevention guide for bottling-line operators and maintenance teams.
Learn more
2026-08-23
Bottle Rinser Has Low Spray Pressure: Causes and Repair Steps
Check whether the loss affects the entire rinser or only several nozzles. System-wide loss points to supply, pump, filter or valve problems; a local pattern points to blocked nozzles, damaged tubing or a misaligned bottle. Follow this practical fault-isolation, repair and prevention guide for bottling-line operators and maintenance teams.
Learn more