CSD Production Line Pressure Oscillates from Mixer to Filler
Pressure instability across a carbonated beverage line is easiest to solve while the original evidence is still available. Keep affected samples, record the operating state and resist making several adjustments at once.
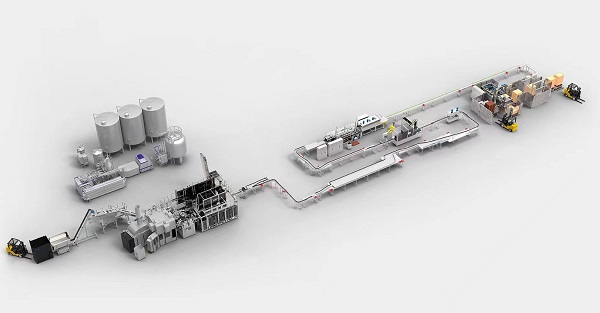
A complete production line is a chain of dependent processes: treatment or preparation, container making, filling, closure, labelling, packing, conveying and utilities. The line output is set by the slowest unstable constraint, not by the nameplate speed of one machine. The objective is not merely to clear the alarm for pressure instability across a carbonated beverage line, but to recover a repeatable, verifiable process.
Quick answer: Trend mixer, buffer, filler and gas-supply pressures with flow and tank levels. Control loops can fight each other when pump capacity, valve sizing, buffer volume or setpoints are not coordinated.
What operators usually see
Use the following signs to define the boundary of the problem. A head-by-head, lane-by-lane or time-based pattern is especially valuable: For this case, preserve evidence that shows whether mixer and filler pressures oscillate out of phase.
- Mixer and filler pressures oscillate out of phase
- Foam spikes when tank level corrects
- Pumps cycle or cavitate
- Line speed repeatedly derates on pressure alarms
Make the equipment safe and protect the product
Use the line-wide stop, lockout/tagout and product-hold procedures. A safe diagnosis must include adjacent machines, stored pneumatic and hydraulic energy, hot process circuits, robots and the possibility that equipment can restart from an upstream or downstream command.
Use synchronized timestamps to collect state, speed, fault, starve and block data from every major machine. Add product-quality results and utility pressure, flow, temperature and power so a local alarm can be related to the upstream event that caused it. Explicitly record whether mixer and filler pressures oscillate out of phase.
Most likely causes, in practical checking order
1. Interacting control loops
Fast level, pressure and flow controllers overcorrect the same disturbance To test this explanation without guessing, record all related pressure, level, flow, valve and pump signals on a common trend Record the result before moving to the next cause.
2. Insufficient hydraulic buffer
Small volume and long delays turn normal demand changes into pressure swings A practical confirmation step is to identify which variable moves first. Compare the finding with a known-good run.
3. Pump or valve operates outside stable range
Oversized valves and off-curve pumps respond poorly at partial load Do not compensate for this condition in the recipe. First, check pump suction and operating point Keep the original setting and measured result in the fault record.
4. Gas supply regulator cannot follow demand
Pressure droop or recovery adds another oscillating source Separate this cause from the others with one controlled check: review valve travel and whether control stays near an extreme Use the same product, format and speed for the comparison.
Step-by-step diagnostic procedure
Follow the sequence in order and preserve each result. Stop if any check would require defeating a guard, interlock or validated food-safety control.
- Record all related pressure, level, flow, valve and pump signals on a common trend
- Identify which variable moves first
- Check pump suction and operating point
- Review valve travel and whether control stays near an extreme
- Compare buffer residence and demand-step size
- Test gas-supply stability under controlled load
Corrective actions that address the root cause
The repair must remove the mechanism, not hide its alarm. Use specified hygienic and safety-rated parts and record every change.
- Coordinate validated loop response through qualified controls engineering
- Restore adequate buffer and stable pump operation
- Correct valve sizing or mechanical condition
- Service gas regulation and supply capacity
How to verify the repair before full-speed production
A successful no-load cycle is not enough. Use the actual product and package, sample every relevant head or lane, and verify this condition: Confirm that pressure instability across a carbonated beverage line is absent for multiple consecutive cycles, not only for one sample. Review the alarm history and keep diagnostic product segregated until the site’s quality procedure releases it.
- Confirm that pressure instability across a carbonated beverage line is absent for multiple consecutive cycles, not only for one sample.
- Compare the repaired result for “Mixer and filler pressures oscillate out of phase” with the approved quality limit and the last known-good baseline.
- Check adjacent stations and downstream package quality for side effects associated with interacting control loops.
- For “CSD Production Line Pressure Oscillates from Mixer to Filler”, record the final settings, measurements, parts used and restart authorization.
Prevent the problem from returning
Use the repair evidence to improve the control plan. The following actions make recurrence visible early:
- Keep line-wide trend templates
- Record tuning revisions
- Test controlled demand steps
- Maintain pumps and regulators
- Review control interaction after capacity changes
When to stop troubleshooting and call a specialist
Stop and contact the machine or component supplier when pressure instability across a carbonated beverage line cannot be isolated with non-invasive checks, when it returns after an approved repair, or when calibration requires protected service tools. Escalate immediately for a damaged pressure boundary, uncontrolled motion, food-safety risk, exposed conductor or repeated protective trip. Send the service engineer the fault history, photos, samples, trend data, recipe revision and work already completed.
Relevant equipment for this application
The site example most closely related to pressure instability across a carbonated beverage line is the CSD Filling Production Line. Equipment selection should be checked against samples, quality limits, required sustained output and available utilities.
Frequently asked questions
What should be checked first when pressure instability across a carbonated beverage line?
Trend mixer, buffer, filler and gas-supply pressures with flow and tank levels. Control loops can fight each other when pump capacity, valve sizing, buffer volume or setpoints are not coordinated. Preserve the original settings and take representative samples before repair work begins.
How can we distinguish interacting control loops from insufficient hydraulic buffer?
Fast level, pressure and flow controllers overcorrect the same disturbance In contrast, small volume and long delays turn normal demand changes into pressure swings Compare the two mechanisms under the same operating condition by completing these checks: record all related pressure, level, flow, valve and pump signals on a common trend Then identify which variable moves first
Can production continue while pressure instability across a carbonated beverage line?
Only when the plant’s documented risk assessment and quality procedure allow it. For pressure instability across a carbonated beverage line, stop and segregate production when package integrity, sanitation, validated processing, pressure safety, electrical protection or an uncontrolled reject trend is involved.
What evidence will help the equipment supplier respond faster?
Provide the model and serial number, product and format, target speed, first fault, timestamps, photos or video, affected station pattern and maintenance history. For this issue, also include mixer and filler pressures oscillate out of phase and the measured result from this check: test gas-supply stability under controlled load
Need help planning your packaging line?
Share your product, bottle and capacity requirements for a practical equipment recommendation.
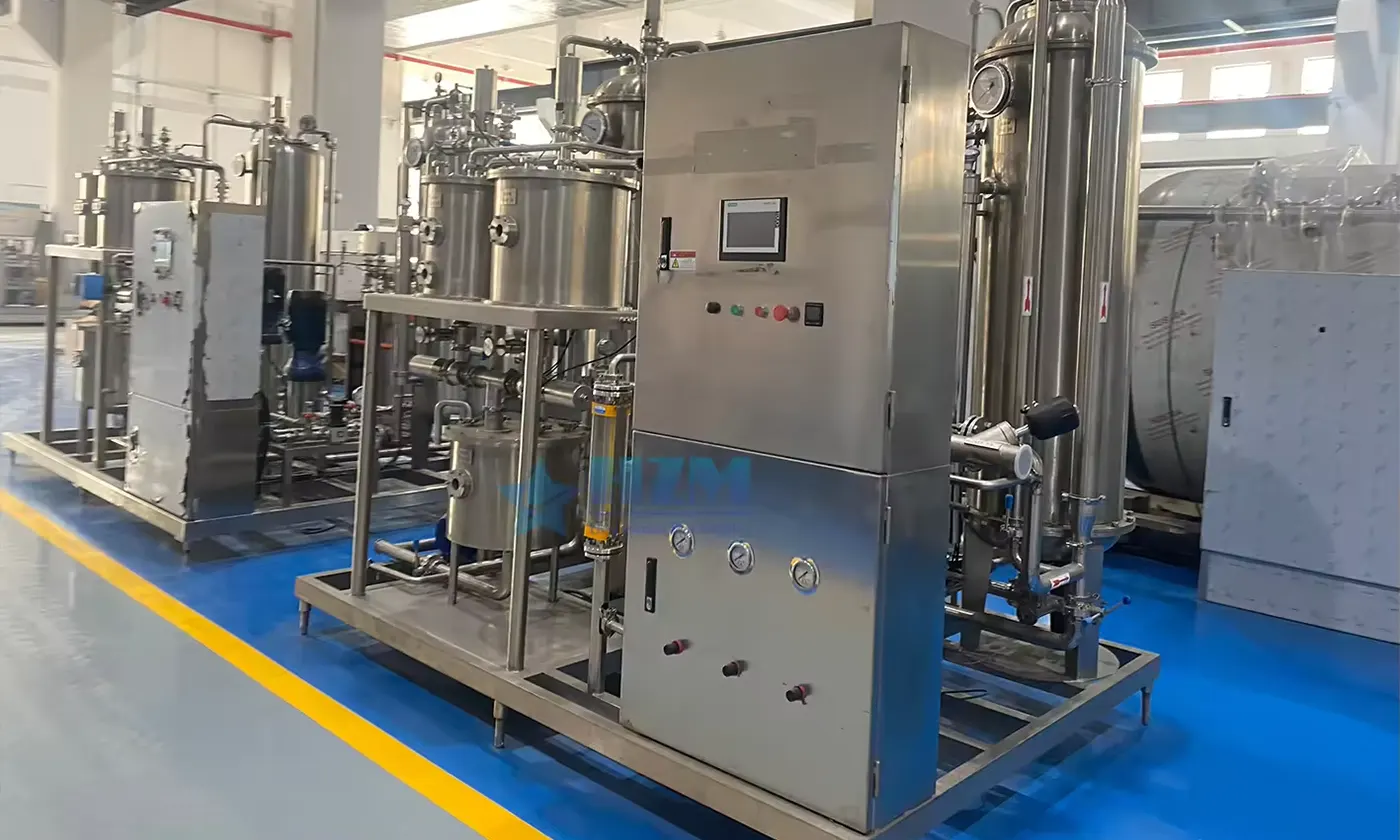
Carbonated Drink Co2 Mixer Machine
The CO2 mixer blends beverage ingredients and carbonates the drink before filling.
Learn more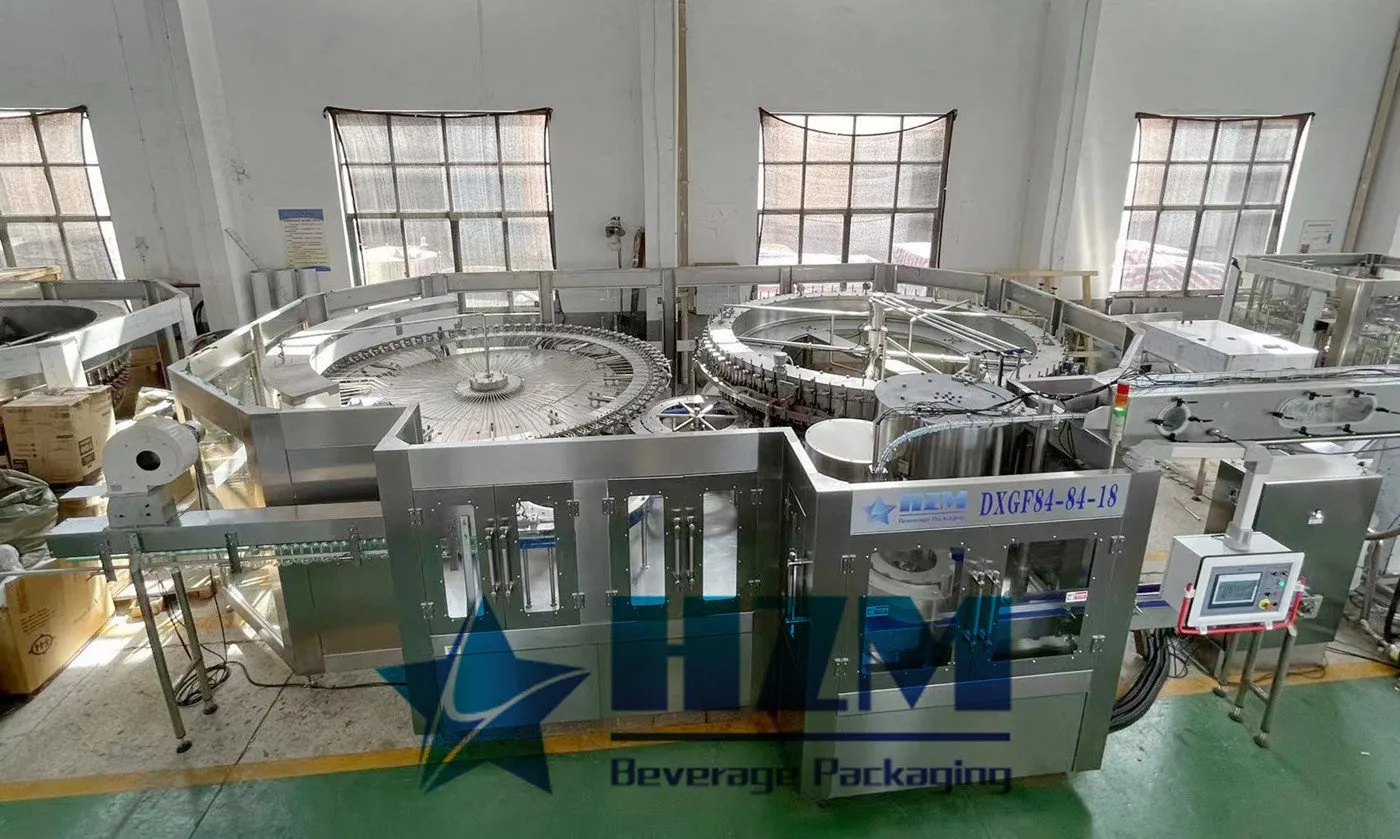
Carbonated Drinks Filling Machine
Carbonated drink rinsing, isobaric filling and capping for PET bottles, with capacities of 4,000–36,000 bottles/hour at 500 ml.
Learn more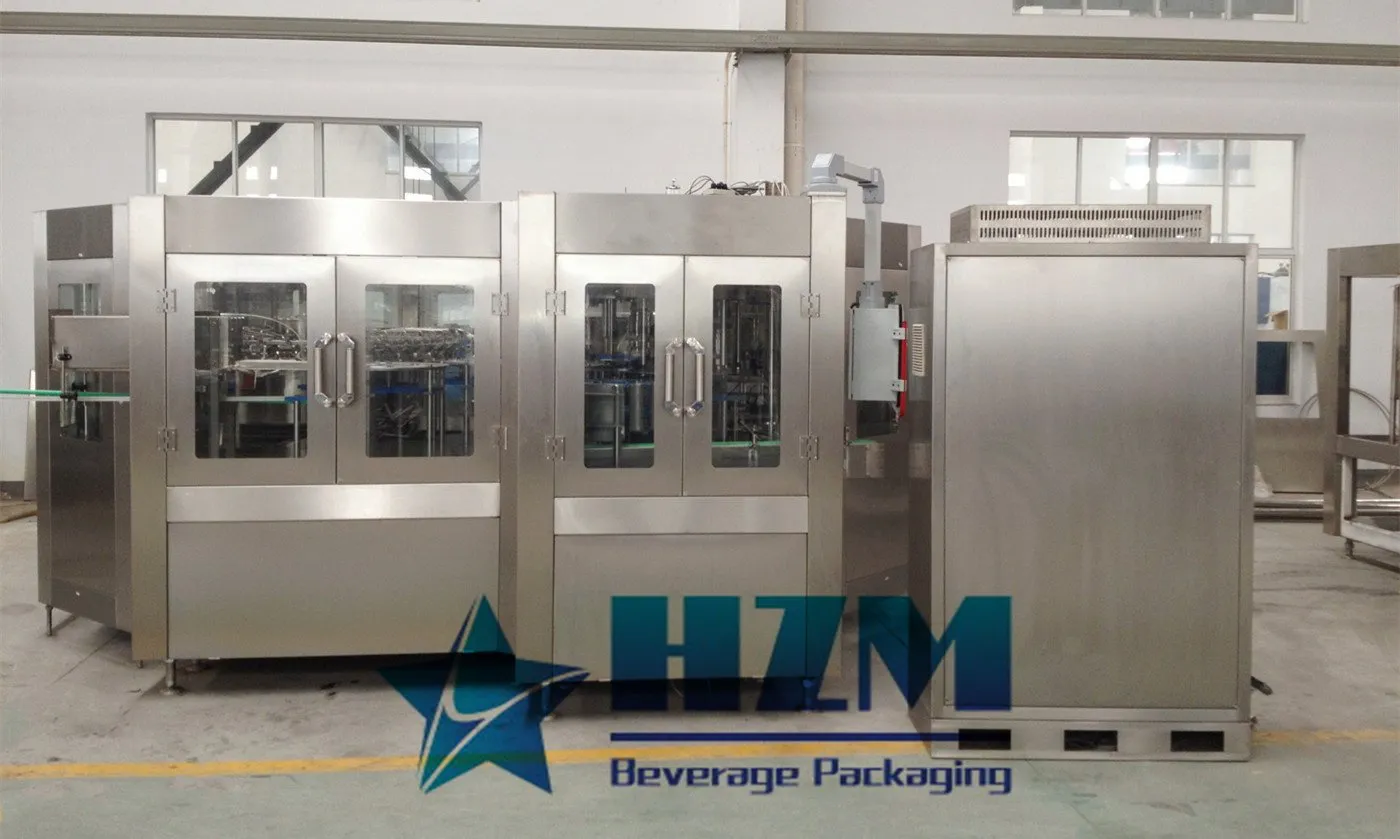
PET Bottle CSD Beverage Filling Machine
Automatic PET bottle rinsing, isobaric filling and capping for cola, soda water and other carbonated soft drinks.
Learn more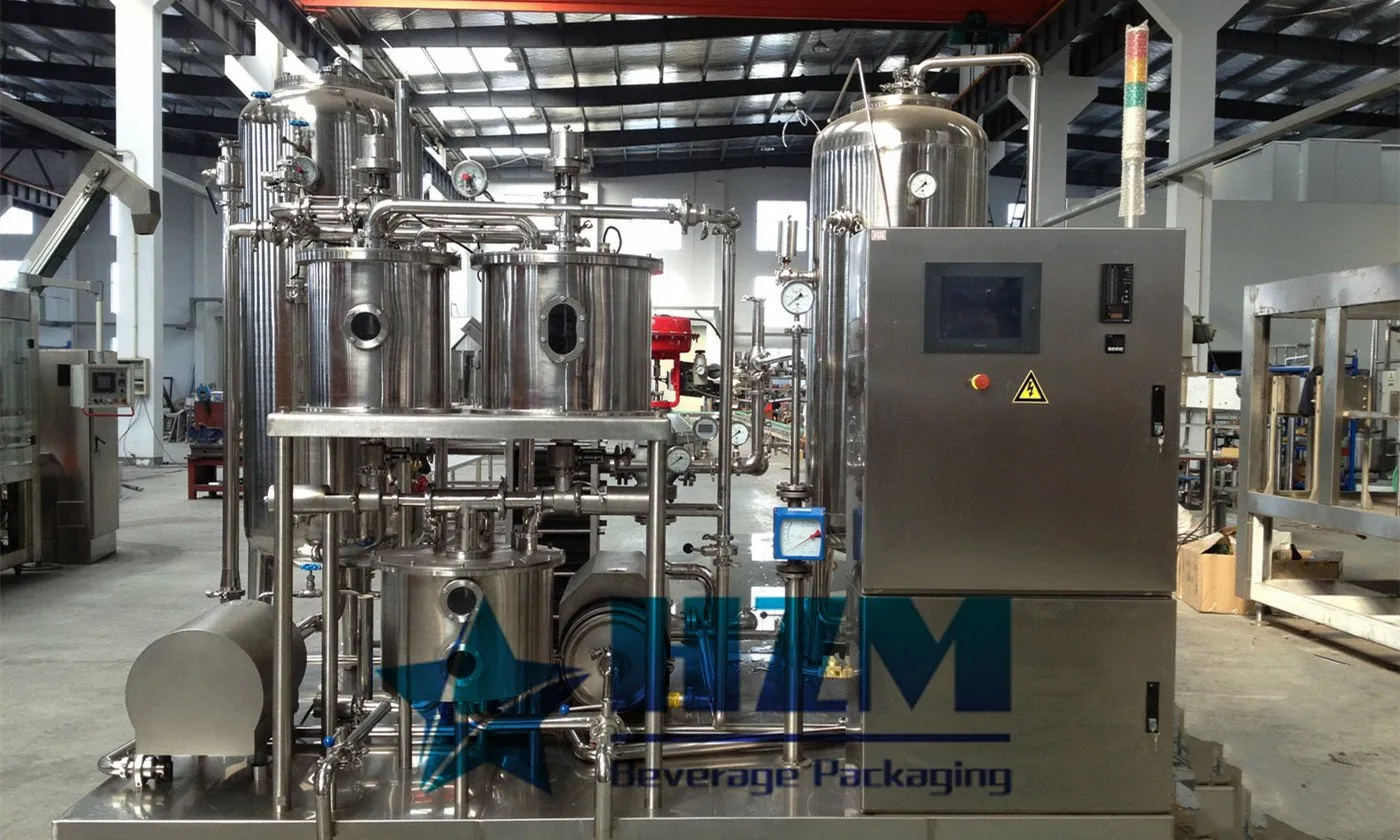
CO2 Saturator | Co2 mixer machine
Five-tank beverage mixing and carbonation system for soda water and soft drinks, with capacities of 4–20 tonnes/hour.
Learn more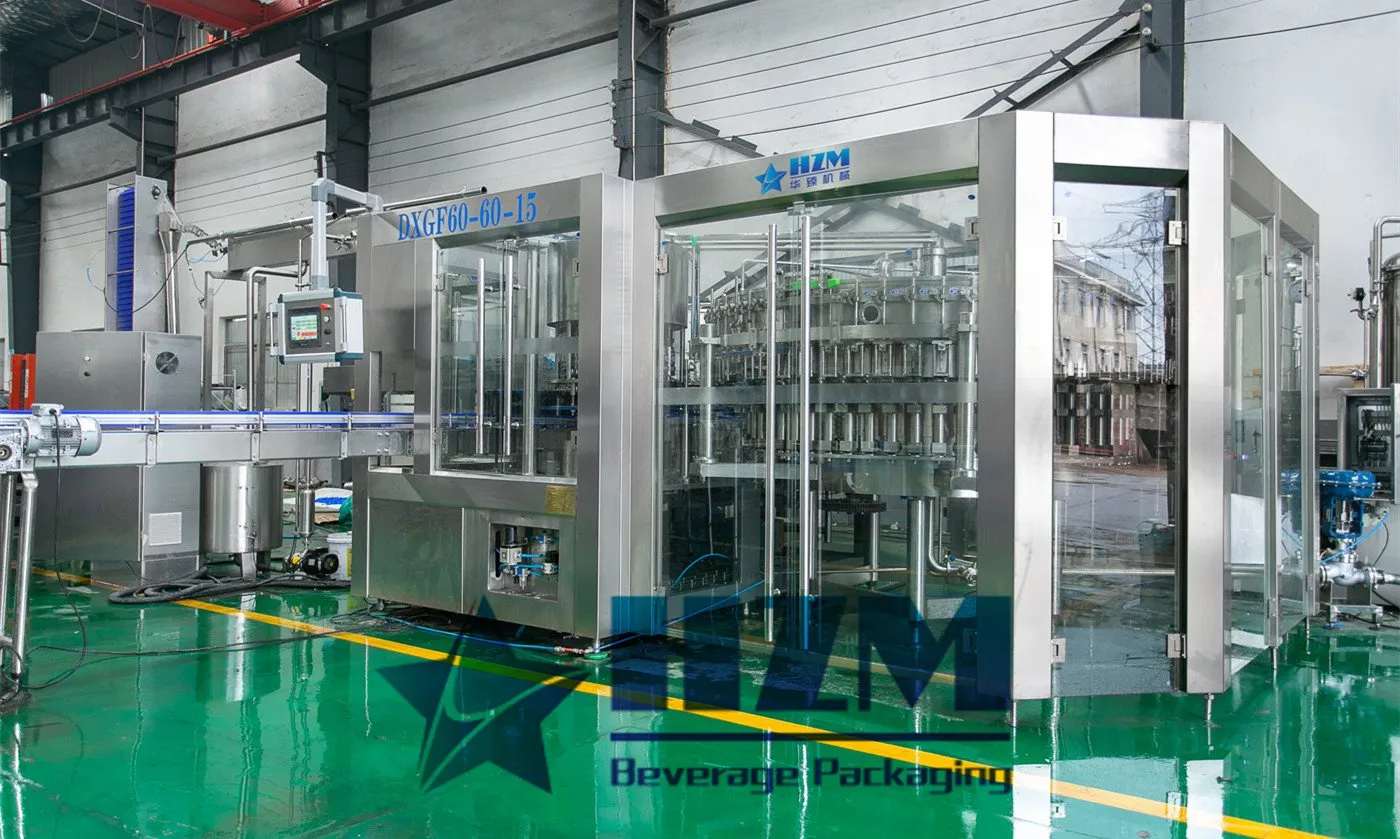
Soda Water Filling Machine
Soda water filling equipment with bottle rinsing, isobaric filling and capping for PET-bottled sparkling water.
Learn more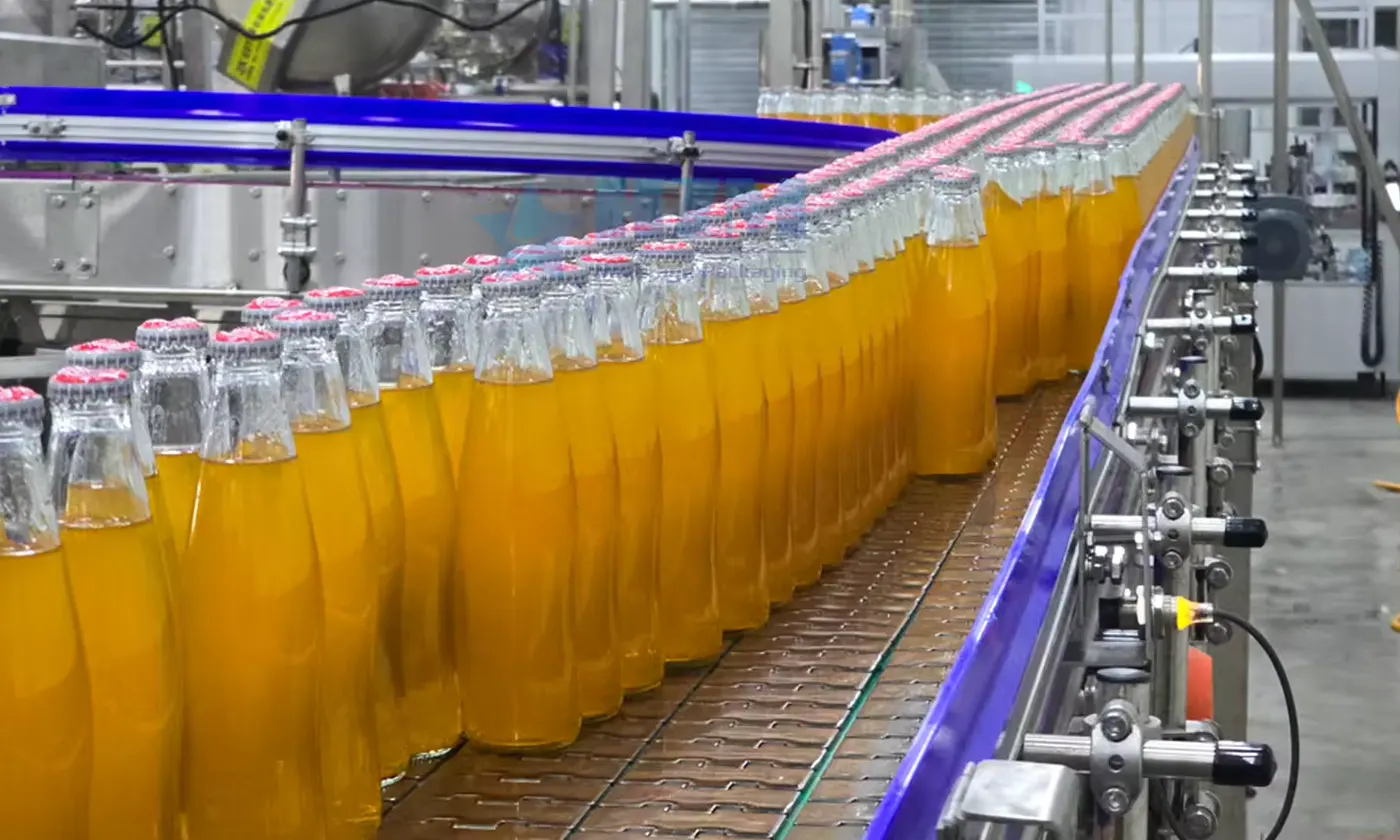
Glass Bottle Carbonated Beverage Filling Bottling Line
This glass bottle carbonated beverage line combines bottle rinsing, isobaric filling and capping with conveying, labelling and packing.
Learn more
CSD Beverage Can Filling Machine
CGS can filling and seaming for carbonated beverages, with capacities of 6,000–36,000 cans/hour at 330 ml.
Learn more
Carbonated Beverage Can Filling Machine
Automatic carbonated beverage can filling and seaming, with CGS capacities of 6,000–36,000 cans/hour at 330 ml.
Learn more
Glass Bottle CSD Beverage Filling Machine
Glass bottle filling for carbonated beverages, with isobaric filling and capacities of 2,000–20,000 bottles/hour at 500 ml.
Learn moreCO2 mixer machine carbonated beverage production line
A CO2 mixer machine is a device used for mixing gases, typically in beverage production lines. It can mix carbon dioxide gas with water or other liquids to produce carbonated drinks
Learn more
CO2 Mixer Machine: The Core Equipment in Carbonated Beverage Production Line
The CO2 mixer machine is a vital piece of equipment in carbonated beverage production lines, featuring a 5-tank design. It offers advantages such as high mixing ratio accuracy, dual carbonation, and a high CO2 content
Learn moreGlass Bottle Filling Line Guide: Pressure Control for Carbonated Beverages
Practical HZM guidance on glass bottle filling line, focused on pressure control for carbonated beverages, line integration, RFQ data and measurable acceptance checks.
Learn more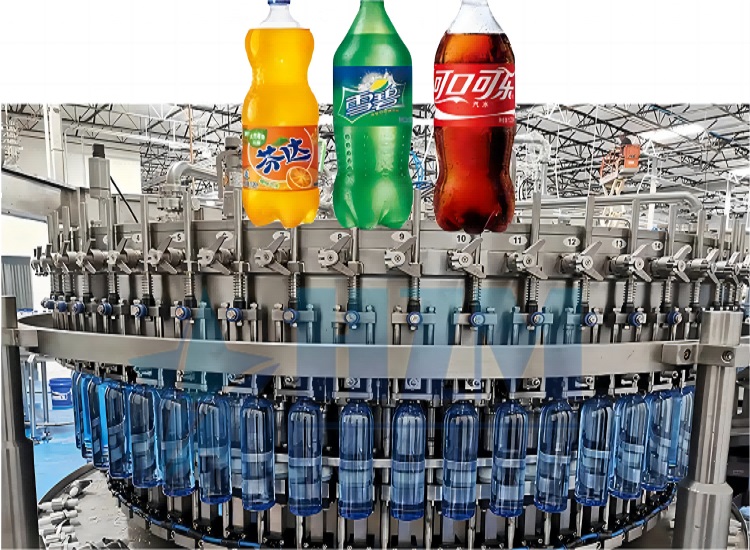
carbonated beverage production equipment solutions
Carbonated beverage production equipment is commonly utilized for the production of carbonated sweetened drinks, commonly known as carbonated beverages or carbonated drinks.
Learn more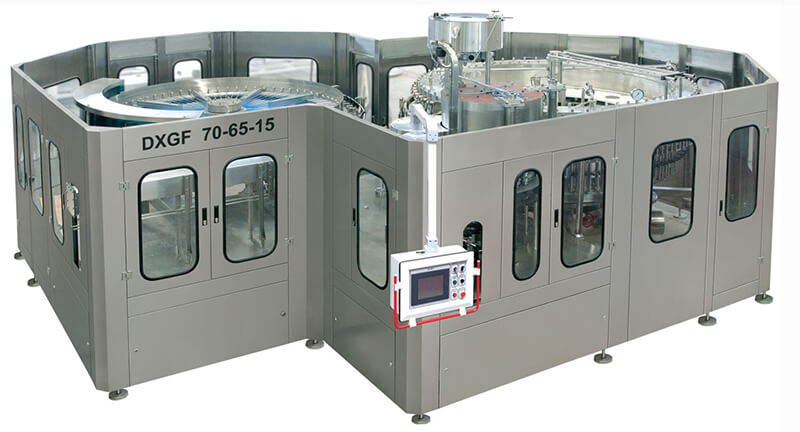
Important Questions To Consider Before Purchasing Carbonated Filling Machine
When it comes to purchasing a carbonated beverage filling machine, making an informed decision is crucial for efficient production. With various options available in the market, considering specific questions can guide you towards selecting the most suitable machine for your needs.
Learn more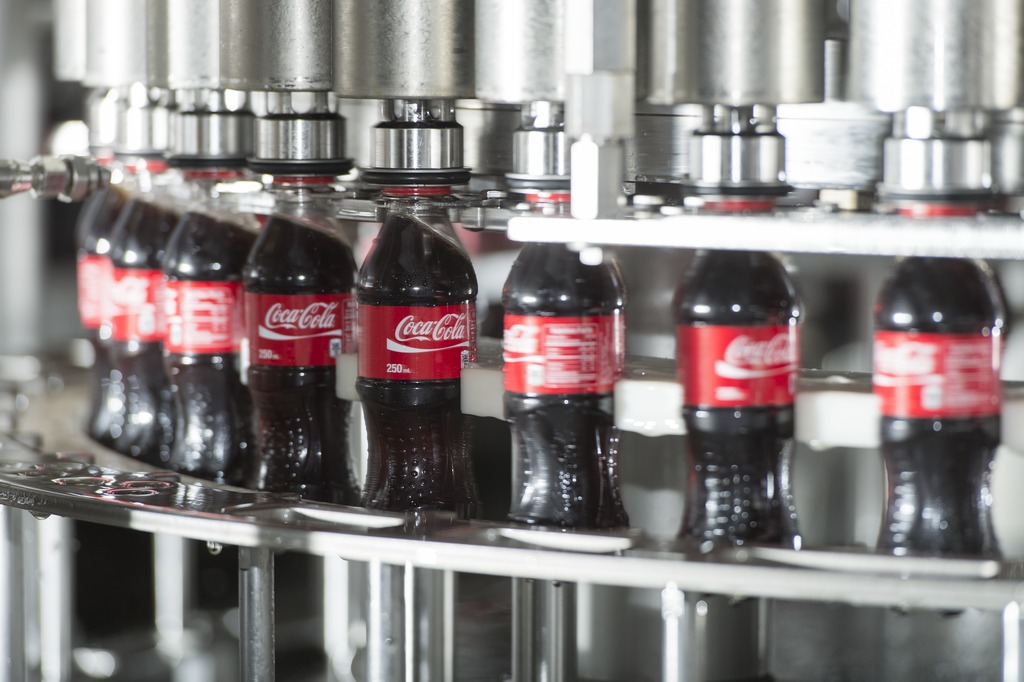
Carbonated Beverage Filling Machine Solution
Carbonated beverage filling equipment is used for filling sweetened drinks containing carbon dioxide, commonly known as carbonated drinks or carbonated beverages. They typically consist of water
Learn more