Insights & Updates
Water Bottling Line Cannot Reach Rated Output: Find the Constraint
When a complete water bottling line running below target output appears, changing the nearest setpoint is tempting but risky. A durable repair starts by retaining samples, capturing the first alarm and separating a local head or lane problem from a line-wide process problem.
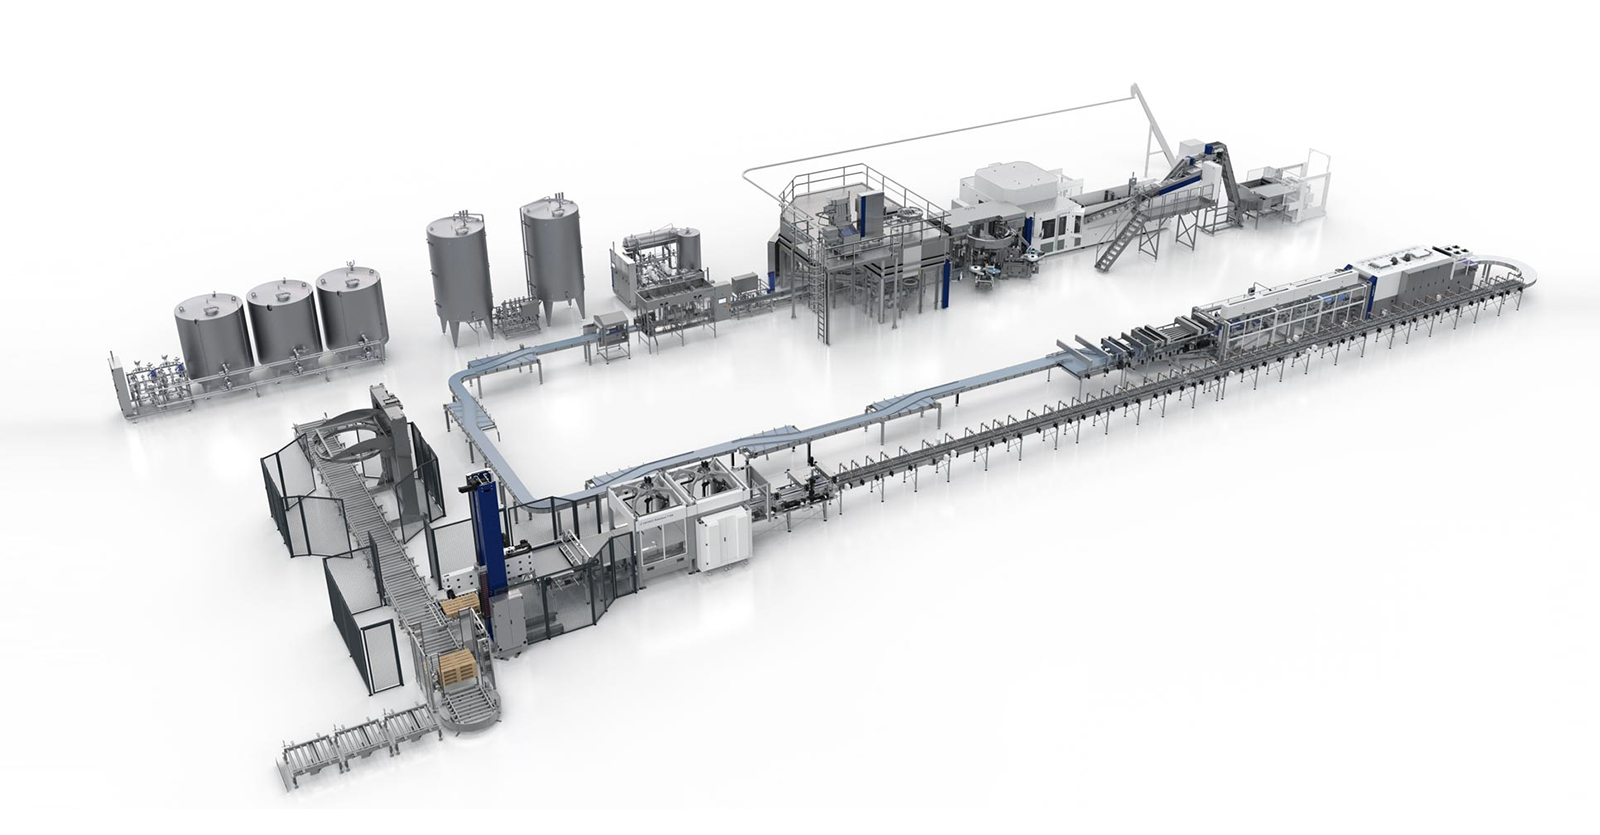
A complete production line is a chain of dependent processes: treatment or preparation, container making, filling, closure, labelling, packing, conveying and utilities. The line output is set by the slowest unstable constraint, not by the nameplate speed of one machine. For this fault, the first distinction is between the nominal bottleneck is unstable and poor line balance and buffering. The procedure below moves from non-invasive checks to controlled repair and restart.
Quick answer: Measure sustained good bottles per hour, then use machine state data to identify the true constraint. Separate starved time, blocked time, faults, quality rejects and planned stops for treatment, blower, filler, labeler, packer and conveyors.
What operators usually see
The failure pattern narrows the search more quickly than replacing parts. Mark samples and record which of these conditions are present: For this case, preserve evidence that shows whether individual machines show high speed but line output is low.
- Individual machines show high speed but line output is low
- The filler alternates between starved and blocked states
- Small stops consume more time than major breakdowns
- Output falls sharply on one bottle format
Make the equipment safe and protect the product
Use the line-wide stop, lockout/tagout and product-hold procedures. A safe diagnosis must include adjacent machines, stored pneumatic and hydraulic energy, hot process circuits, robots and the possibility that equipment can restart from an upstream or downstream command.
Use synchronized timestamps to collect state, speed, fault, starve and block data from every major machine. Add product-quality results and utility pressure, flow, temperature and power so a local alarm can be related to the upstream event that caused it. Explicitly record whether individual machines show high speed but line output is low.
Most likely causes, in practical checking order
1. The nominal bottleneck is unstable
The slowest machine cannot sustain its designed cycle because of microstops, material or maintenance condition To test this explanation without guessing, define the KPI as accepted packaged product over a full representative shift Record the result before moving to the next cause.
2. Poor line balance and buffering
Adjacent machines accelerate and stop each other instead of absorbing normal disturbances A practical confirmation step is to synchronize state and counter timestamps across every major machine. Compare the finding with a known-good run.
3. Quality loss hidden from speed data
Underfills, label rejects, leaks and damaged packs reduce good output after the filler counter Do not compensate for this condition in the recipe. First, calculate run, fault, starved, blocked and planned-stop time by asset Keep the original setting and measured result in the fault record.
4. Utility or material constraint
Water, preforms, caps, labels, film, air or power cannot support simultaneous peak demand Separate this cause from the others with one controlled check: create a Pareto of microstop reason and physical location Use the same product, format and speed for the comparison.
Step-by-step diagnostic procedure
The aim is to eliminate whole groups of causes with each check. Record actual values rather than “normal” or “looks good.”
- Define the KPI as accepted packaged product over a full representative shift
- Synchronize state and counter timestamps across every major machine
- Calculate run, fault, starved, blocked and planned-stop time by asset
- Create a Pareto of microstop reason and physical location
- Compare utility pressure, flow and material replenishment during peak rate
- Repeat the analysis by SKU and speed rather than mixing formats
Corrective actions that address the root cause
A reset is not a repair. Complete the mechanical, process or controls work indicated by the evidence and document the as-left state.
- Stabilize the demonstrated constraint before increasing another machine’s setpoint
- Correct buffer controls and speed hierarchy around the constraint
- Remove the highest-frequency quality and microstop causes
- Upgrade utilities or material logistics only where measured demand proves the gap
How to verify the repair before full-speed production
Restart at reduced speed with normal production materials, then increase output in steps. The first acceptance check is: Confirm that a complete water bottling line running below target output is absent for multiple consecutive cycles, not only for one sample. Review the alarm history and keep diagnostic product segregated until the site’s quality procedure releases it.
- Confirm that a complete water bottling line running below target output is absent for multiple consecutive cycles, not only for one sample.
- Compare the repaired result for “Individual machines show high speed but line output is low” with the approved quality limit and the last known-good baseline.
- Check adjacent stations and downstream package quality for side effects associated with the nominal bottleneck is unstable.
- For “Water Bottling Line Cannot Reach Rated Output: Find the Constraint”, record the final settings, measurements, parts used and restart authorization.
Prevent the problem from returning
The most effective preventive action is an observable limit with a named response, not a general instruction to “check regularly.”
- Review good-output OEE by line and SKU
- Maintain first-fault and state data
- Protect sufficient but not excessive accumulation
- Treat quality rejects as lost capacity
- Recalculate balance before adding faster equipment
When to stop troubleshooting and call a specialist
Stop and contact the machine or component supplier when a complete water bottling line running below target output cannot be isolated with non-invasive checks, when it returns after an approved repair, or when calibration requires protected service tools. Specialist support is also required when the same protective fault returns after an approved repair or structural damage is suspected. Send the service engineer the fault history, photos, samples, trend data, recipe revision and work already completed.
Relevant equipment for this application
For a project-level comparison related to a complete water bottling line running below target output, see HZM Machinery’s Water Filling Production Line. Use actual product, container and utility data when evaluating whether the configuration fits the duty.
Frequently asked questions
What should be checked first when a complete water bottling line running below target output?
Measure sustained good bottles per hour, then use machine state data to identify the true constraint. Separate starved time, blocked time, faults, quality rejects and planned stops for treatment, blower, filler, labeler, packer and conveyors. Preserve the original settings and take representative samples before repair work begins.
How can we distinguish the nominal bottleneck is unstable from poor line balance and buffering?
The slowest machine cannot sustain its designed cycle because of microstops, material or maintenance condition In contrast, adjacent machines accelerate and stop each other instead of absorbing normal disturbances Compare the two mechanisms under the same operating condition by completing these checks: define the KPI as accepted packaged product over a full representative shift Then synchronize state and counter timestamps across every major machine
Can production continue while a complete water bottling line running below target output?
Only when the plant’s documented risk assessment and quality procedure allow it. For a complete water bottling line running below target output, stop and segregate production when package integrity, sanitation, validated processing, pressure safety, electrical protection or an uncontrolled reject trend is involved.
What evidence will help the equipment supplier respond faster?
Provide the model and serial number, product and format, target speed, first fault, timestamps, photos or video, affected station pattern and maintenance history. For this issue, also include individual machines show high speed but line output is low and the measured result from this check: repeat the analysis by SKU and speed rather than mixing formats
Talk to our engineering team
Need help planning your packaging line?
Share your product, bottle and capacity requirements for a practical equipment recommendation.
Equipment
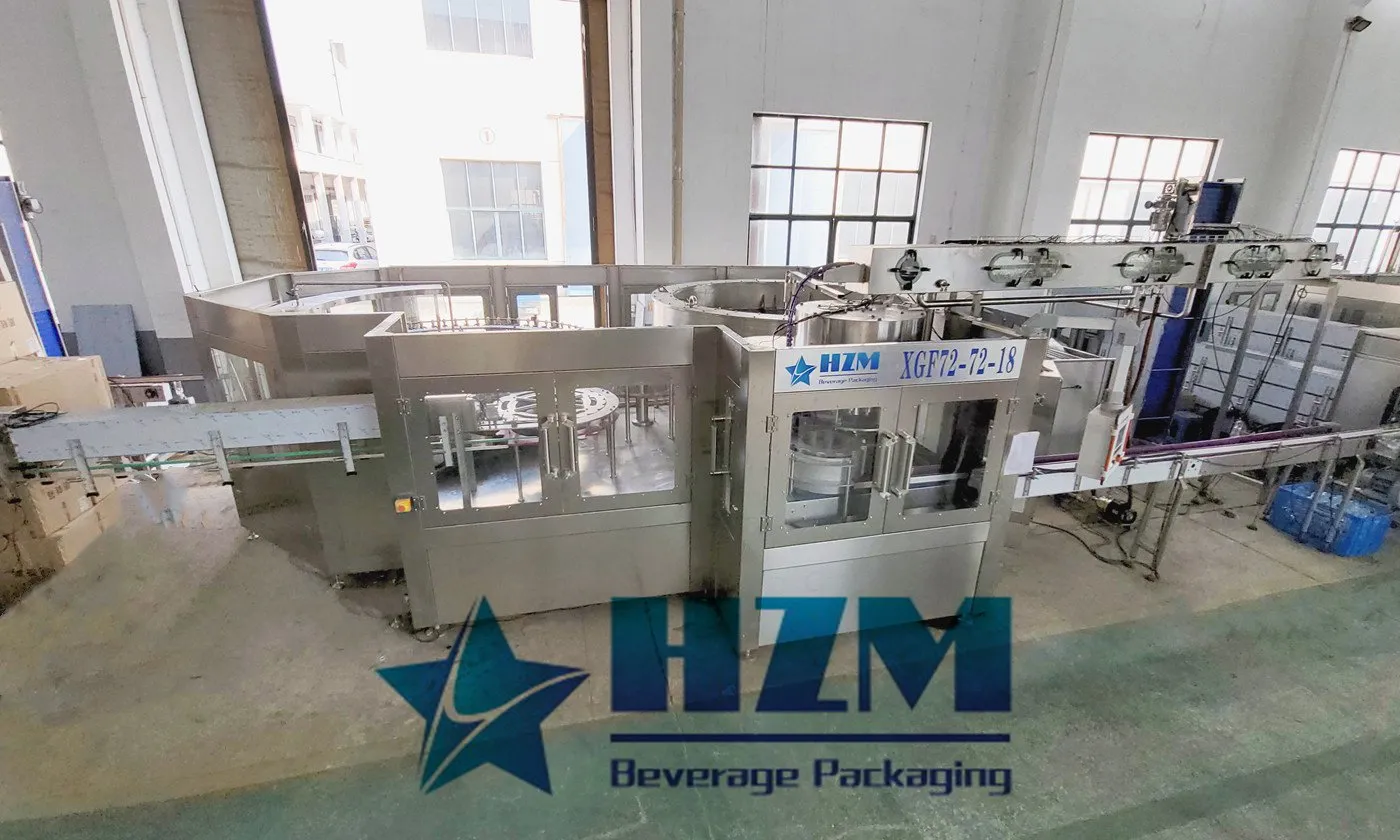
Automatic Water Bottle Filling Machine
Automatic rinsing, filling and capping for purified and mineral water in PET bottles, with capacities of 5,000–42,000 bottles/hour at 500 ml.
Learn more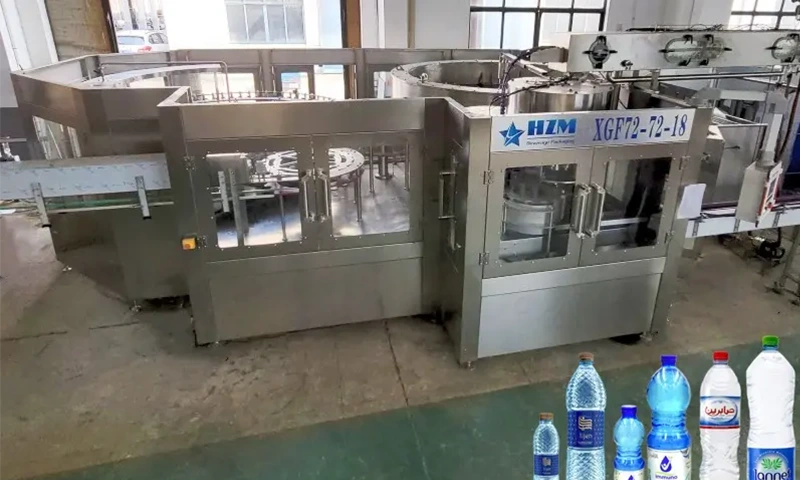
Equipment
3-In-1 Water Bottle Filling Machine
A 3-in-1 PET bottle rinsing, filling and capping machine for drinking water, from 5,000 to 18,000 bottles/hour at 500 ml.
Learn more
Equipment
Automatic Drinking Water Bottling Machine
Drinking-water bottling equipment with automatic rinsing, filling and capping, plus conveying, labelling and packing options.
Learn more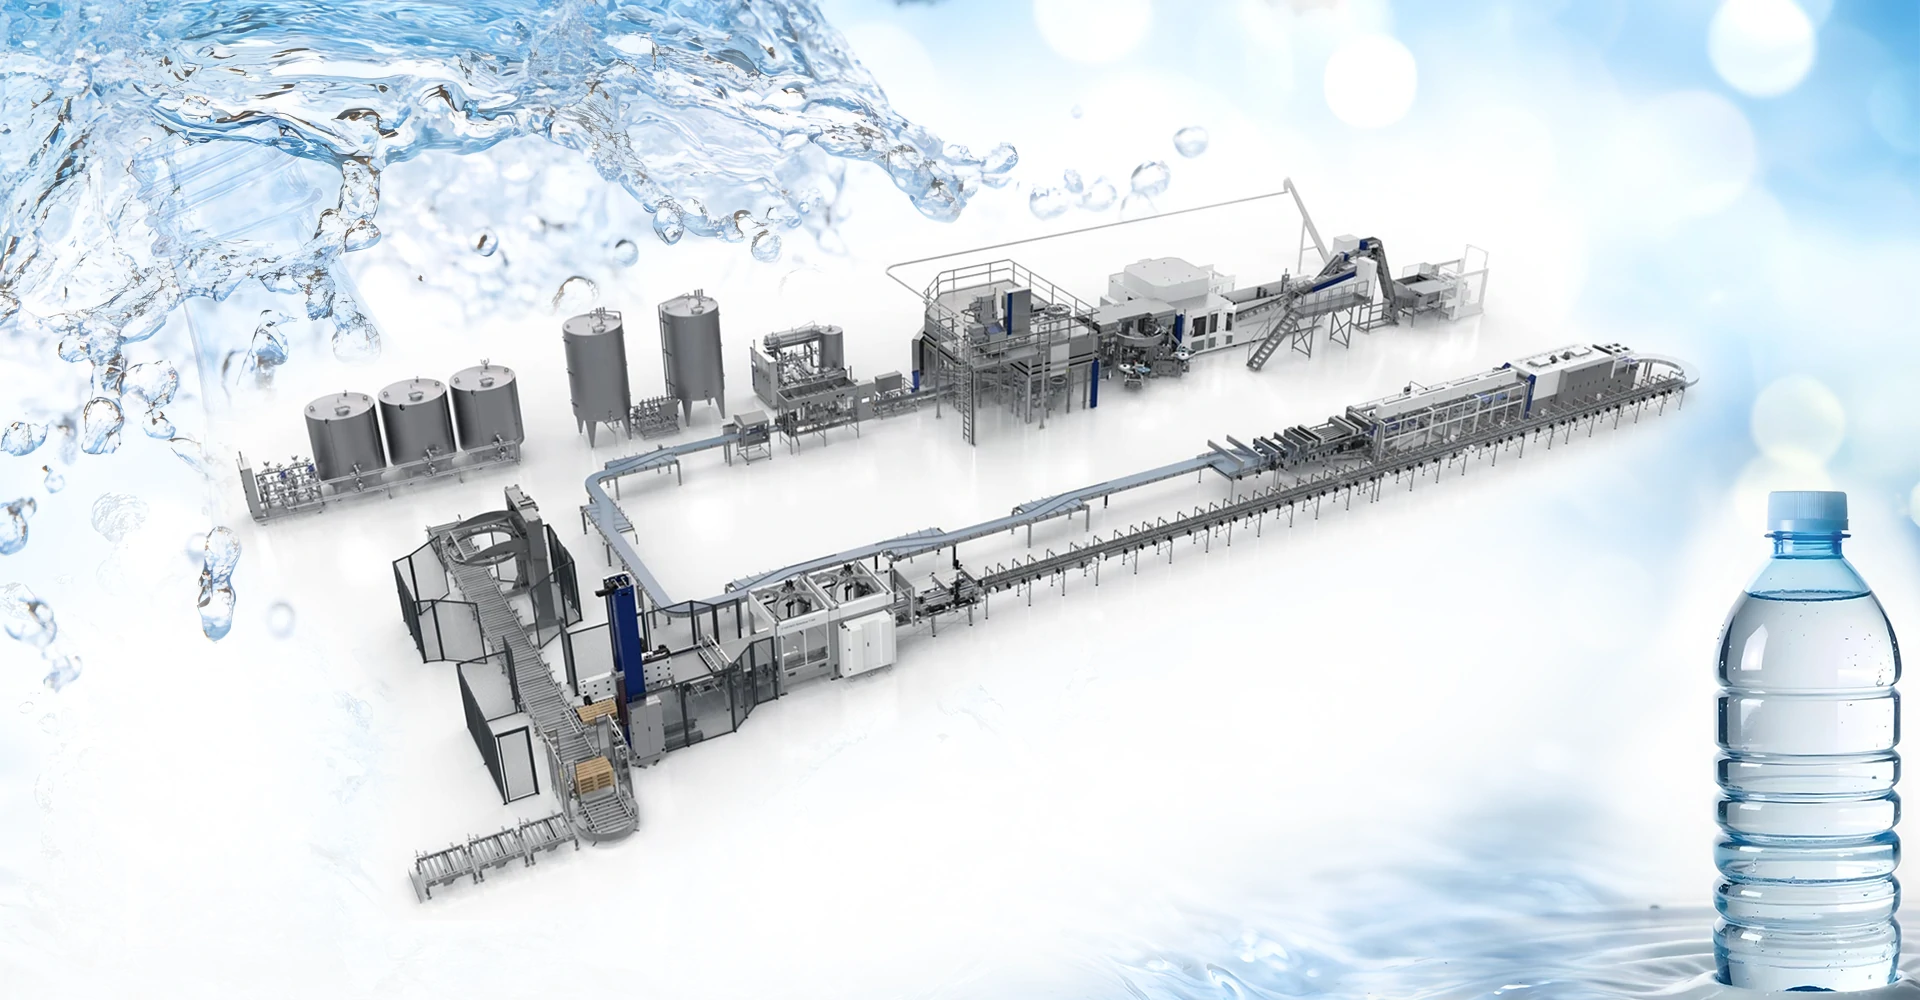
Equipment
Drinking water production line – Bottled Water Filling Machine Manufacturer
PET-bottled drinking-water production with automatic rinsing, filling and capping, plus water treatment and packaging equipment.
Learn more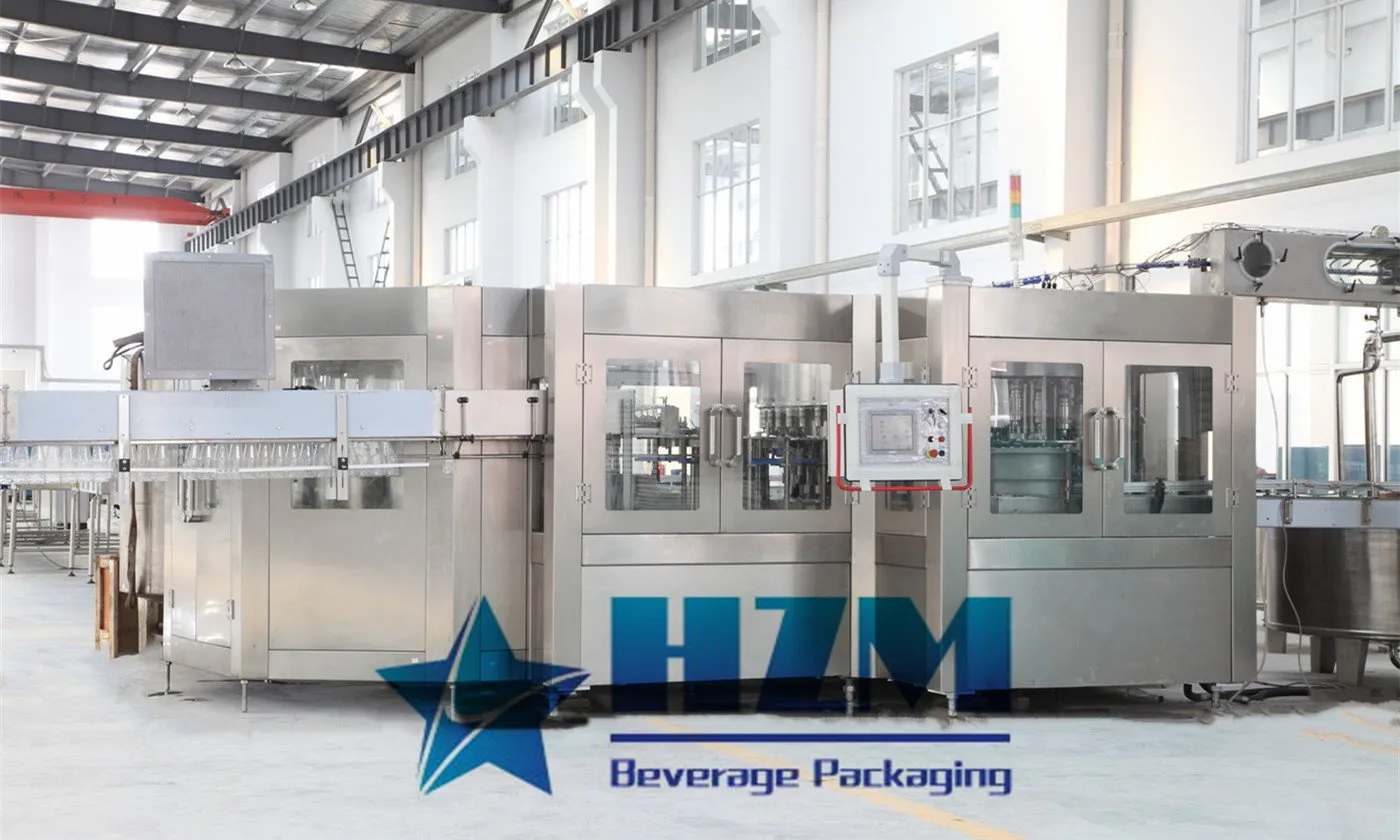
Equipment
PET Bottle Water Filling Machine
PET bottle water filling with automatic rinsing and capping, for purified water, mineral water and still drinking water.
Learn more
Equipment
5L-10L Large Bottle Drinking Water production line
XGF12-12-4 rinsing, filling and capping for 5 L and 10 L water bottles, with stable outputs of 1,200 and 700 bottles/hour respectively.
Learn more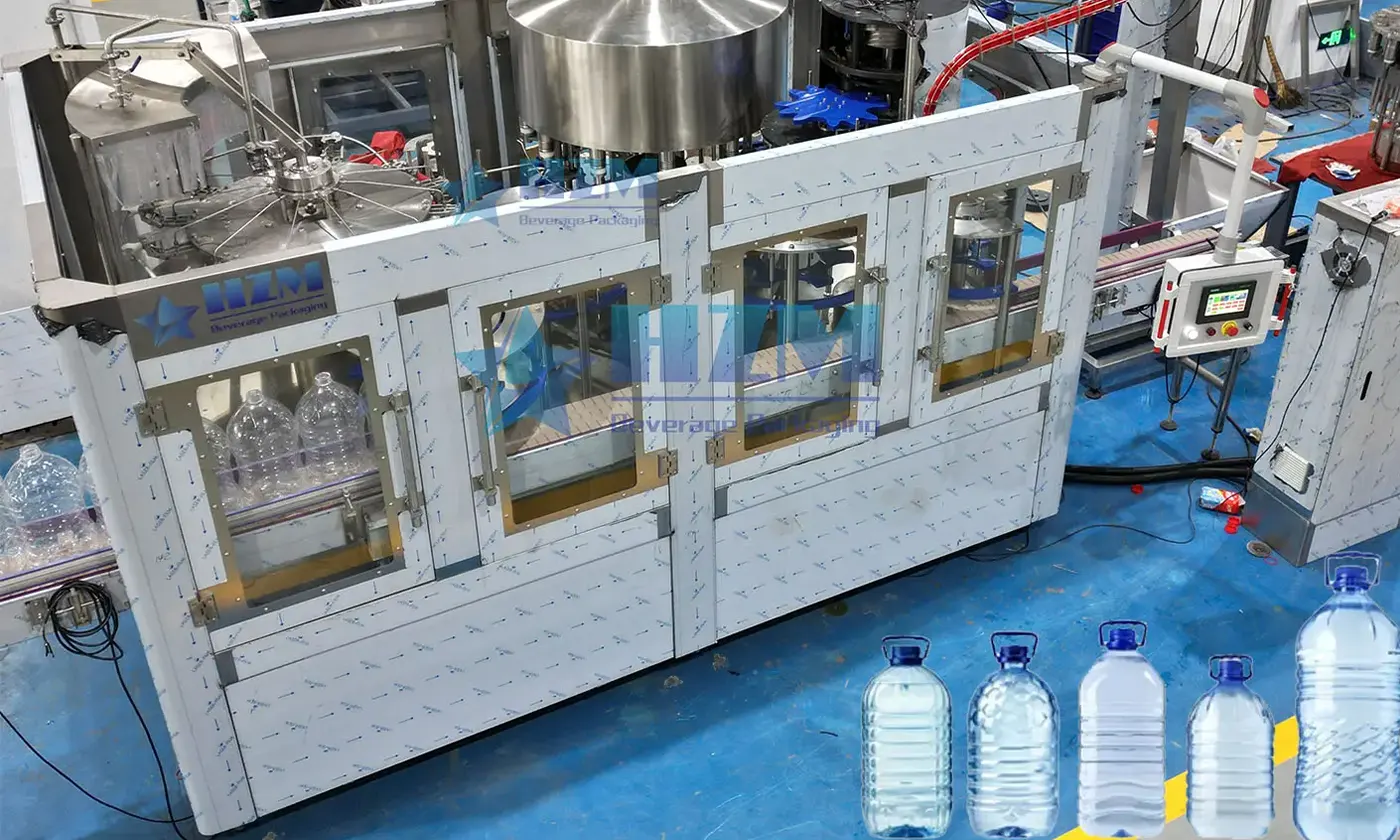
Equipment
Bottled Water Filling Machine & Turnkey Water Bottling Line
Bottled water filling machines and turnkey lines for purified and mineral water, with dedicated small-bottle, large-bottle and gallon-jar systems.
Learn more
Equipment
Automatic Water Bottle Labeling Machine
Automatic hot-glue labelling for water and beverage bottles, with HG models from 8,000 to 24,000 bottles/hour.
Learn more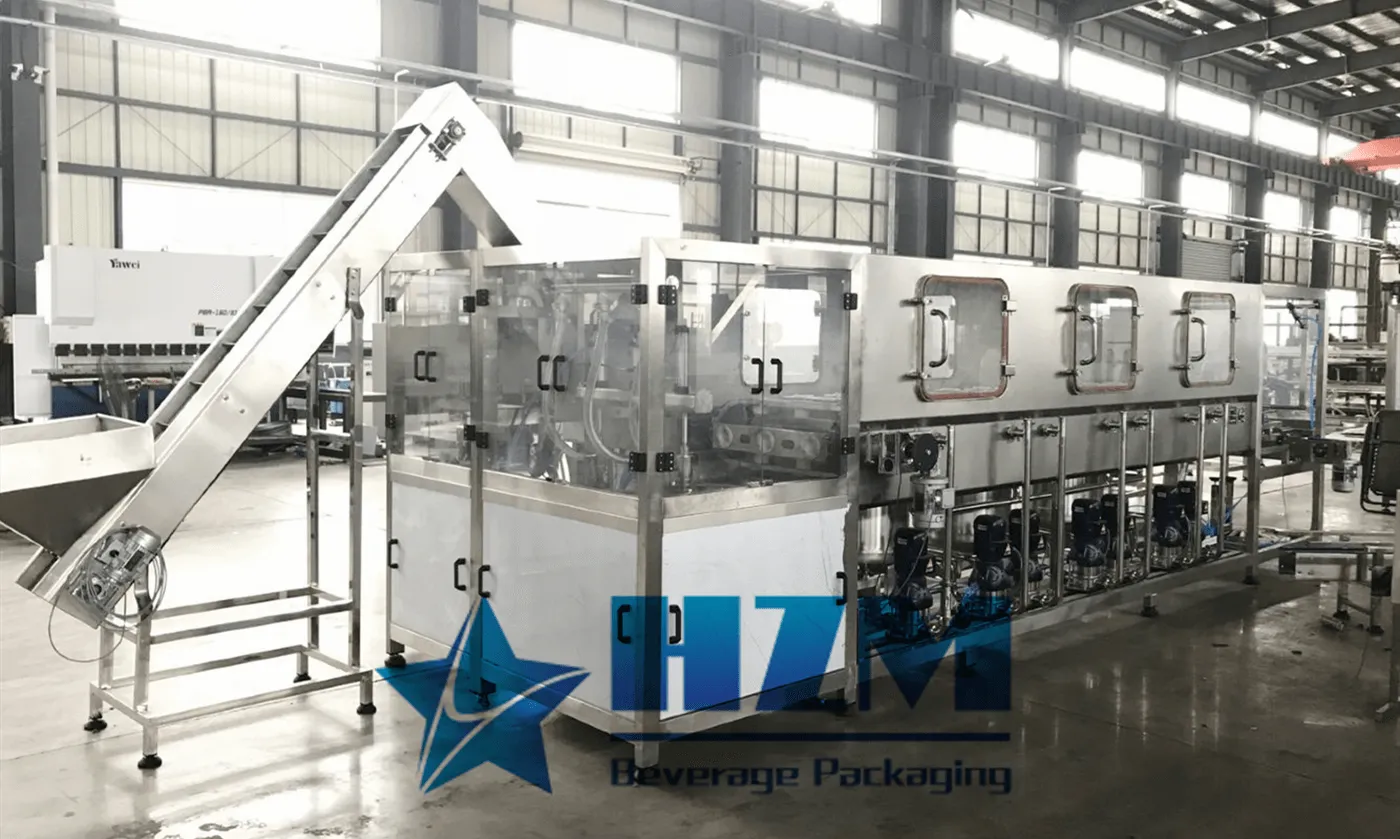
Equipment
3-5 Gallon Water Filling Line
Automatic washing, filling and capping for 3–5 gallon drinking-water jars, with QGF models from 120 to 900 jars/hour at 5 gallons.
Learn more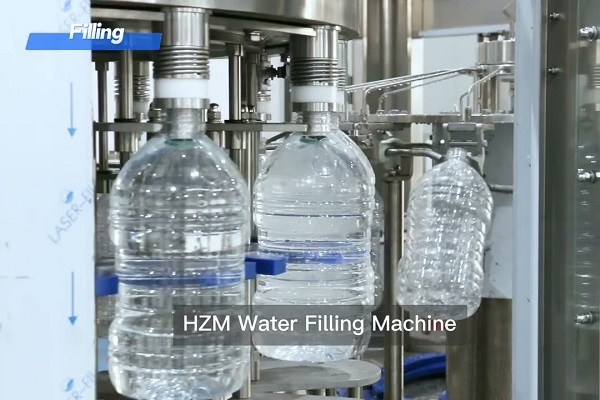
2023-06-09
5-Gallon Water Bottling Line Guide: Output Planning for 3- and 5-Gallon Formats
Practical HZM guidance on 5-gallon water bottling line, focused on output planning for 3- and 5-gallon formats, line integration, RFQ data and measurable acceptance checks.
Learn more
2023-11-21
Bottle Water Filling Machines and Production Line Equipment price
This article will delve into the price range of Bottle Water Filling Machines and the full set of production line equipment provided by HZM Machinery, providing you with a comprehensive understanding and reference.
Learn more
2023-09-14
Water Bottle Filling Machine Prices
Water bottle filling machines are highly automated filling equipment used for various containers, including water bottles, beverage bottles, and wine bottles. The application of this equipment is incredibly diverse, spanning across industries such as food, beverages, and household products
Learn more
2023-11-24
Water Bottle Filling Machine Solutions
Water bottle filling machines come in various configurations, from small-scale, semi-automatic machines suitable for small businesses to fully automated, high-speed machines used in large-scale production facilities. They play a crucial role in ensuring the efficiency and quality of the water bottling process.
Learn more2023-12-15
How to Choose Bottled Water and Beverage Production Line Equipment
Choosing the right bottled water and beverage production equipment is a crucial factor in establishing a successful factory. Simultaneously, a detailed understanding of the production process, market dynamics, and strategic planning is essential for the success of any enterprise.
Learn more2023-06-06
HZM Water Filling Line: Your Reliable Supplier for Complete Equipment Solutions
HZM Water Filling Line is dedicated to offering efficient and reliable equipment and services to water production enterprises.
Learn more