CSD Line Loses Carbonation Between Mixer and Package
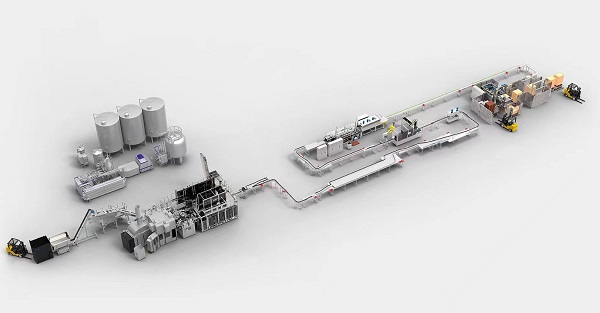
Build a CO2 profile from mixer outlet to finished package while recording temperature and pressure. Check heat gain, pipe pressure loss, pump and tank operation, filler equalization, foaming, snift and closure delay.
Use the line-wide stop, lockout/tagout and product-hold procedures. A safe diagnosis must include adjacent machines, stored pneumatic and hydraulic energy, hot process circuits, robots and the possibility that equipment can restart from an upstream or downstream command.
Locate the fault
- Mixer meets CO2 target but finished product does not
- Loss increases with long pipe runs or warm conditions
- Foam and underfill rise together
- Results worsen after stops
Inspection sequence
- Verify one carbonation method and sample procedure
- Take synchronized samples at mixer, filler inlet and package
- Trend product temperature and pressure through each segment
- Compare mixer stability with filler speed
- Map foam and CO2 by filling head
- Measure fill-to-close time and closure quality
Corrective work
- Reduce heat gain and pressure loss
- Stabilize mixer flow, cooling and gas control
- Repair filler equalization and restore validated timing
- Correct closure transfer and application
Operating records and follow-up
- Trend CO2 pickup and loss by segment
- Insulate or cool transfer as designed
- Calibrate related instruments
- Sample stops and restarts
- Maintain closure quality
Need help planning your packaging line?
Share your product, bottle and capacity requirements for a practical equipment recommendation.
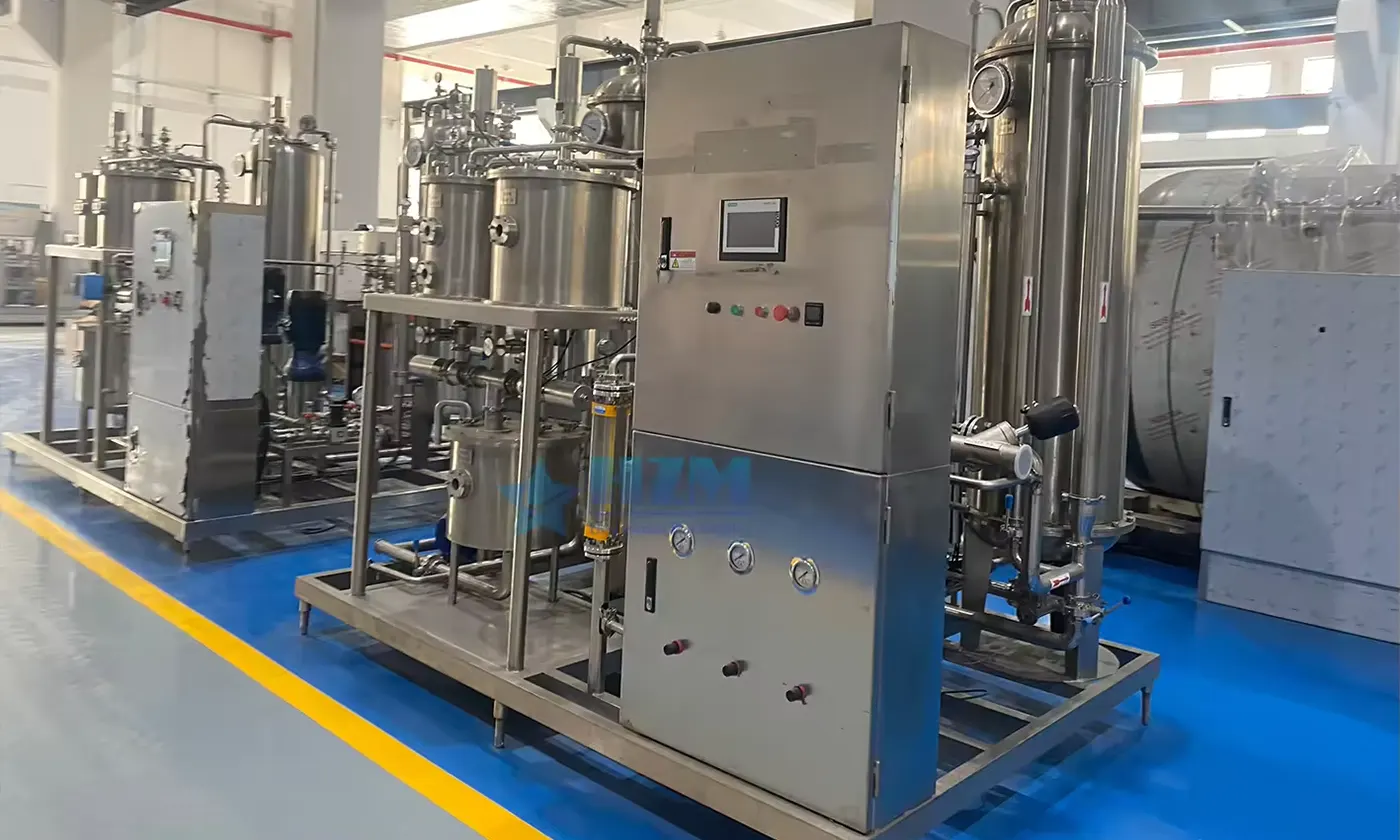
Carbonated Drink Co2 Mixer Machine
The CO2 mixer blends beverage ingredients and carbonates the drink before filling.
Learn more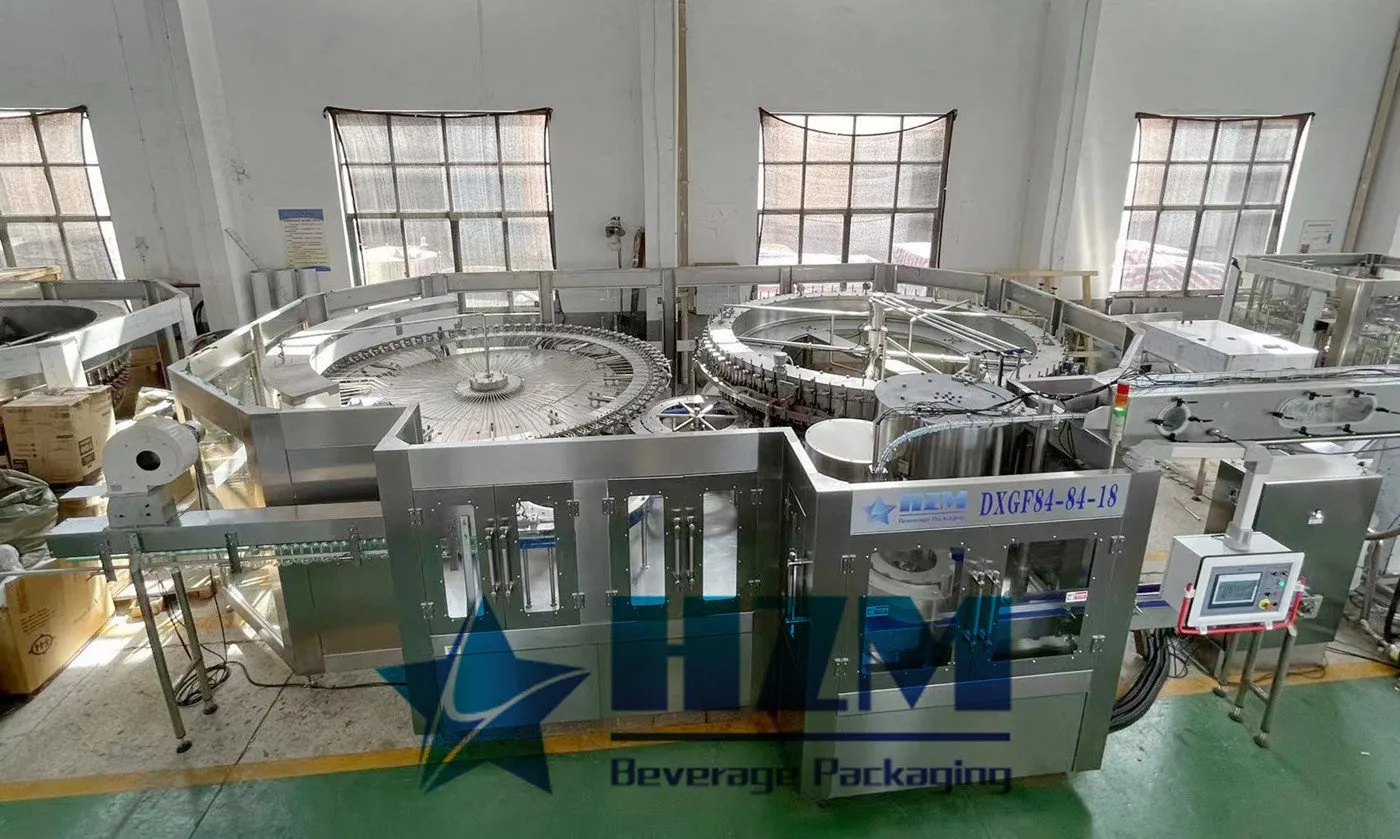
Carbonated Drinks Filling Machine
Carbonated drink rinsing, isobaric filling and capping for PET bottles, with capacities of 4,000–36,000 bottles/hour at 500 ml.
Learn more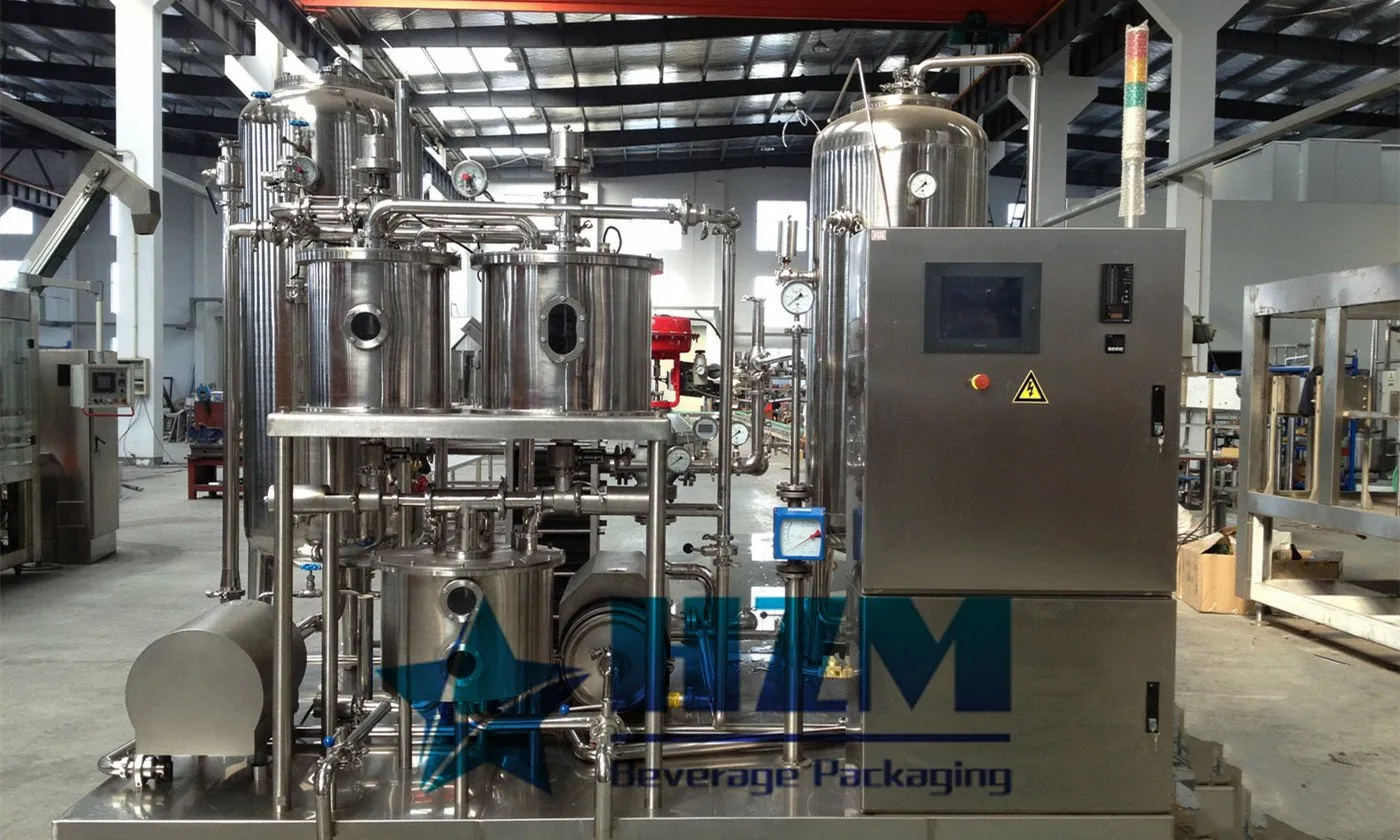
CO2 Saturator | Co2 mixer machine
Five-tank beverage mixing and carbonation system for soda water and soft drinks, with capacities of 4–20 tonnes/hour.
Learn more
PET Bottle CSD Beverage Filling Machine
Automatic PET bottle rinsing, isobaric filling and capping for cola, soda water and other carbonated soft drinks.
Learn more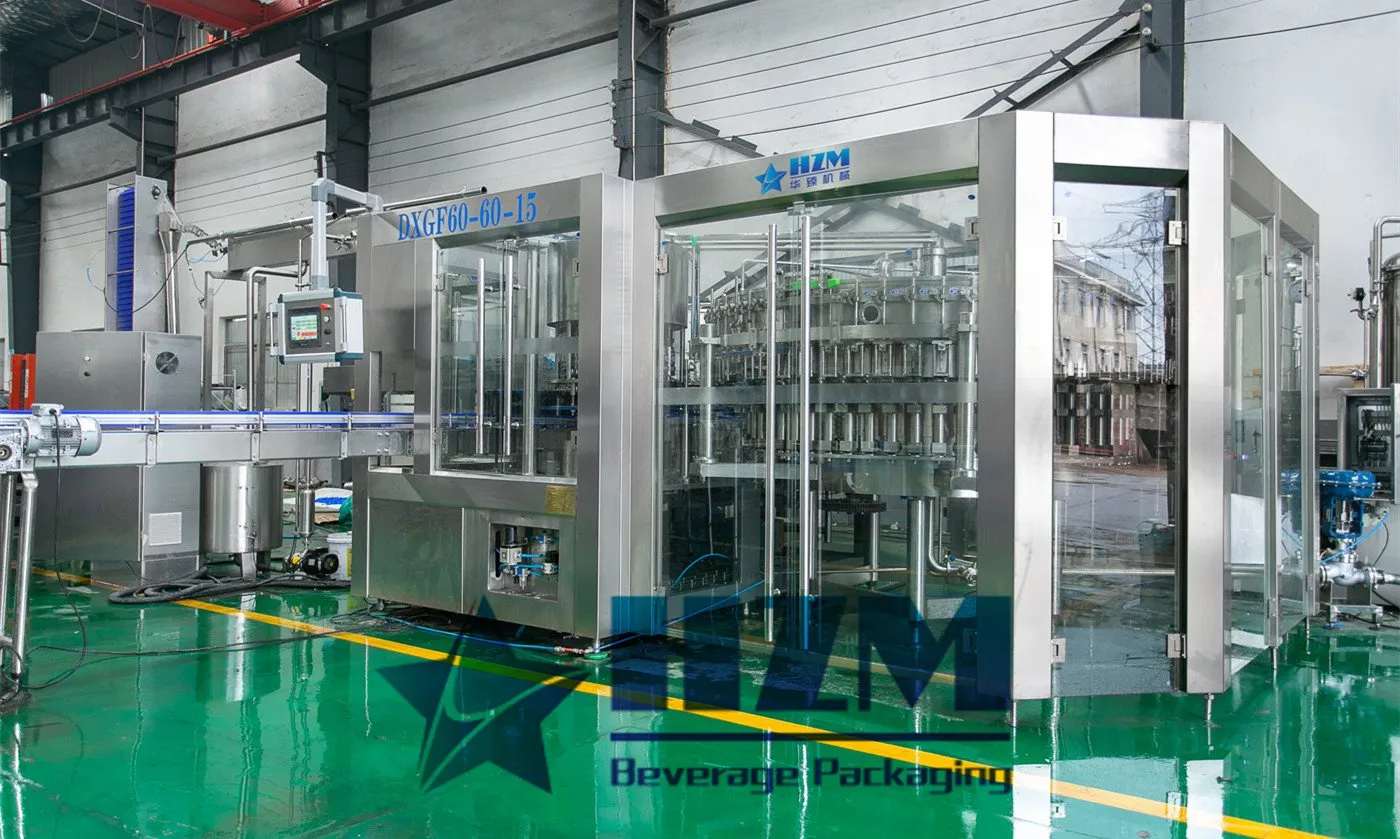
Soda Water Filling Machine
Soda water filling equipment with bottle rinsing, isobaric filling and capping for PET-bottled sparkling water.
Learn more
Glass Bottle Carbonated Beverage Filling Bottling Line
This glass bottle carbonated beverage line combines bottle rinsing, isobaric filling and capping with conveying, labelling and packing.
Learn more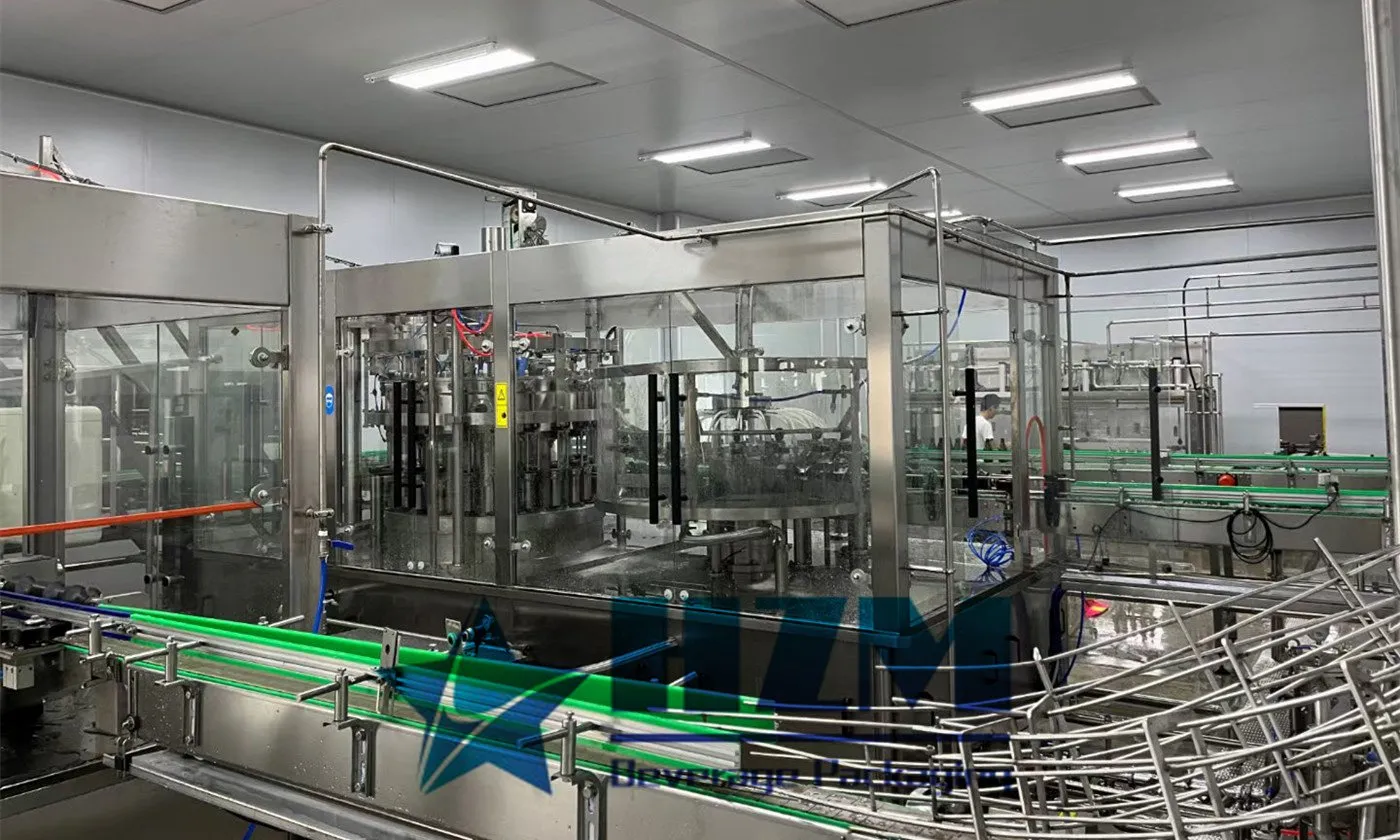
CSD Beverage Can Filling Machine
CGS can filling and seaming for carbonated beverages, with capacities of 6,000–36,000 cans/hour at 330 ml.
Learn more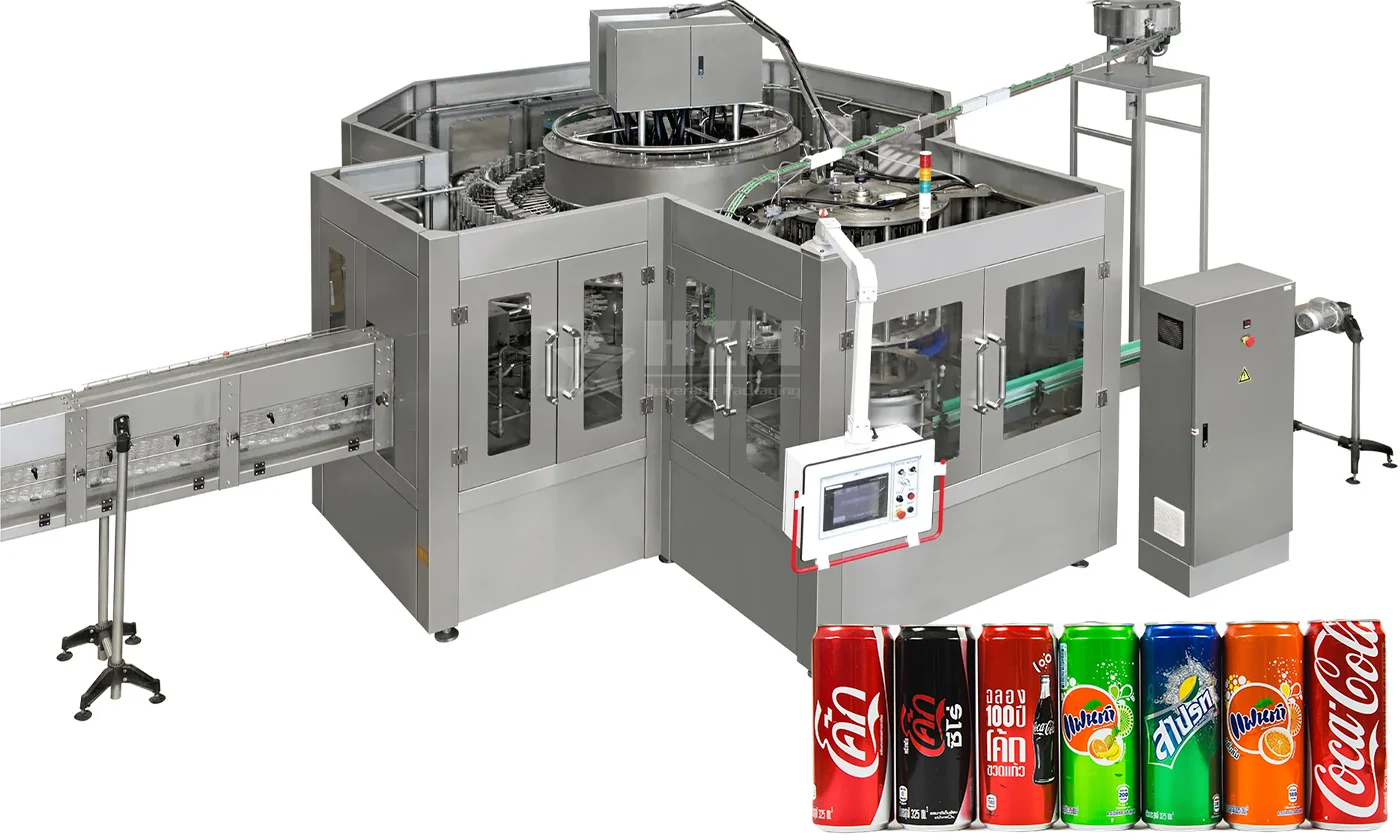
Carbonated Beverage Can Filling Machine
Automatic carbonated beverage can filling and seaming, with CGS capacities of 6,000–36,000 cans/hour at 330 ml.
Learn more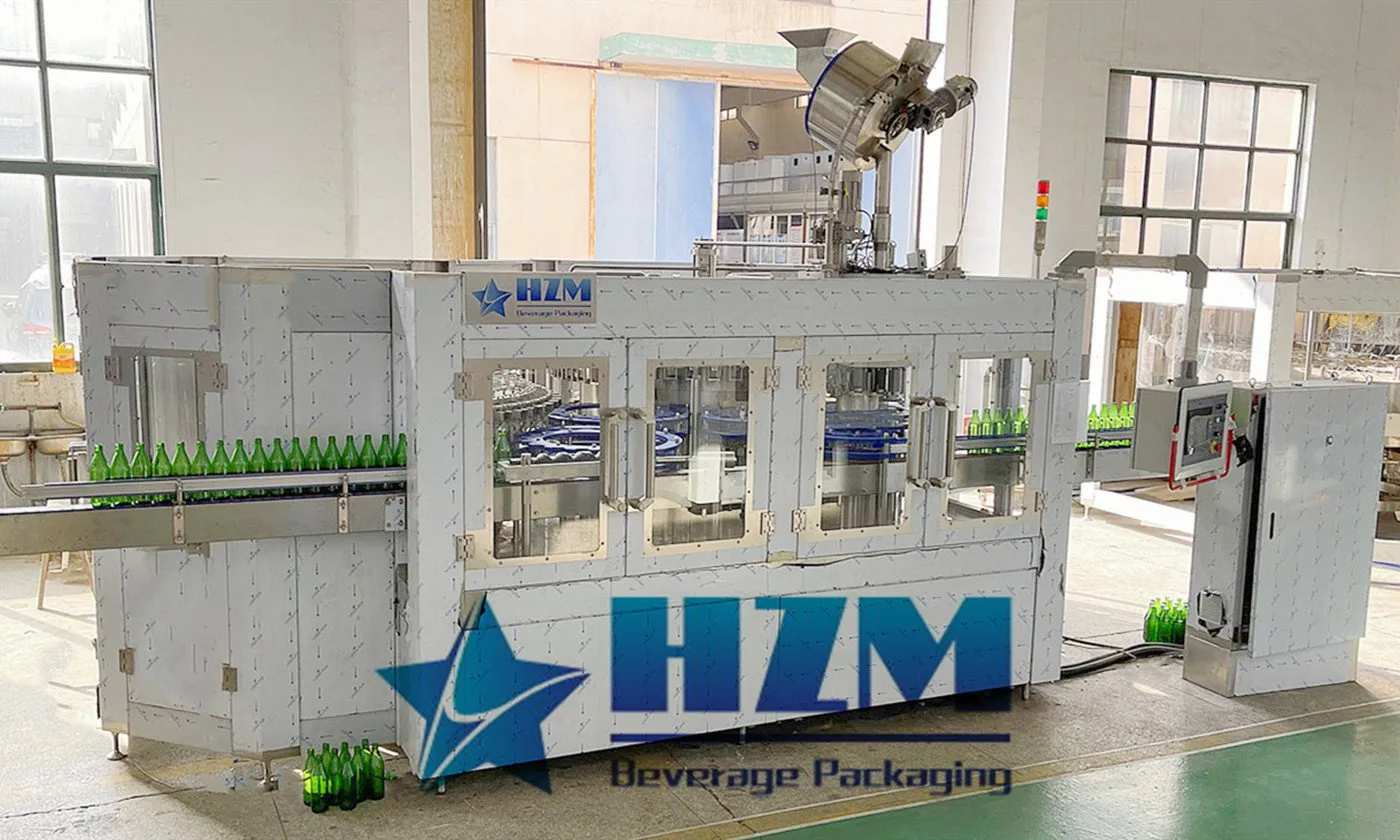
Glass Bottle CSD Beverage Filling Machine
Glass bottle filling for carbonated beverages, with isobaric filling and capacities of 2,000–20,000 bottles/hour at 500 ml.
Learn moreCO2 Mixer Operation in a Carbonated Beverage Line
Understand where carbonation occurs, which conditions control dissolved CO2, and how to separate mixer problems from losses during filling.
Learn more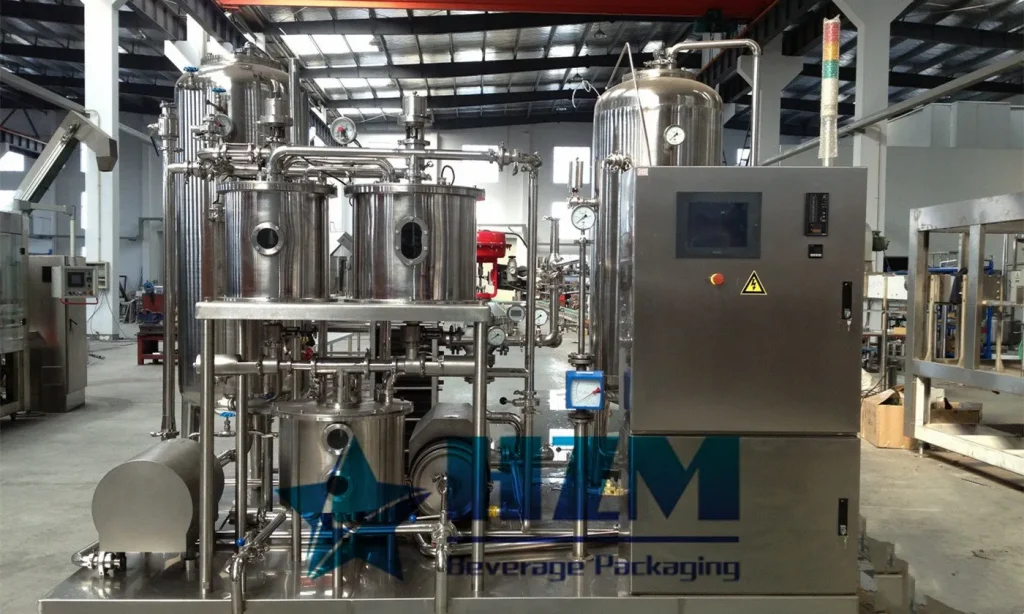
What to Monitor on a Carbonated Beverage Mixer
Monitor liquid ratio, product temperature and carbonation as separate results.
Learn moreCSD Production Line Pressure Oscillates from Mixer to Filler
Trend mixer, buffer, filler and gas-supply pressures with flow and tank levels. Control loops can fight each other when pump capacity, valve sizing, buffer volume or setpoints are not coordinated. Follow this practical fault-isolation, repair and prevention guide for bottling-line operators and maintenance teams.
Learn more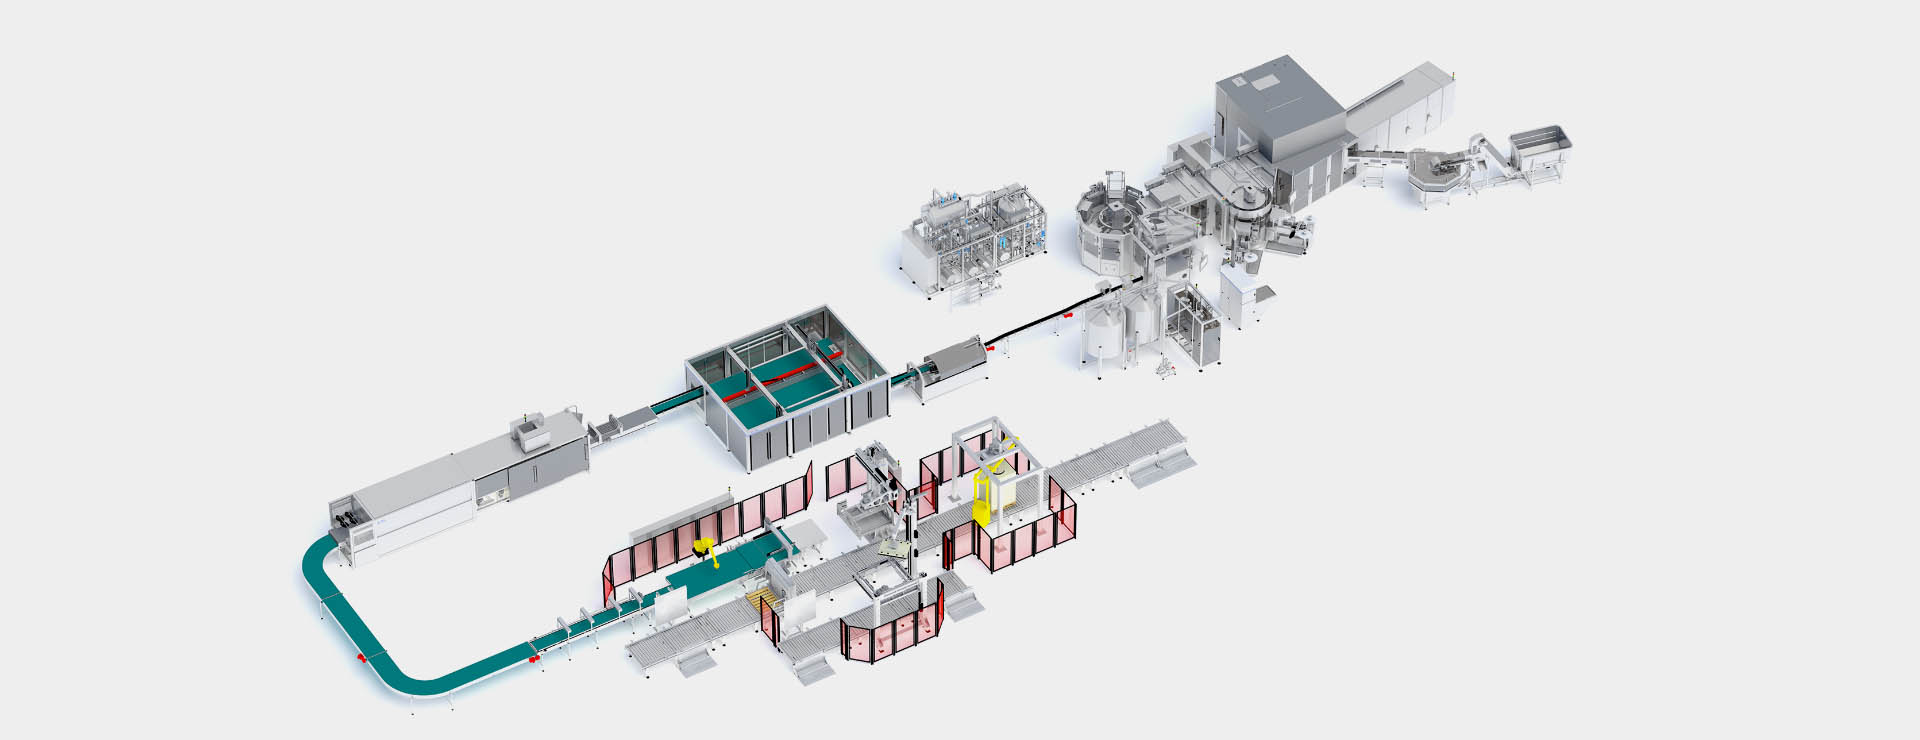
Carbonated Beverage Packaging Machine Solutions
the specific configuration and capabilities of a carbonated beverage packaging machine solution will depend on production scale, packaging type, container size, and other specific requirements. In general, these machines should be carefully selected, configured, and maintained to ensure an efficient carbonated beverage packaging production process.
Learn more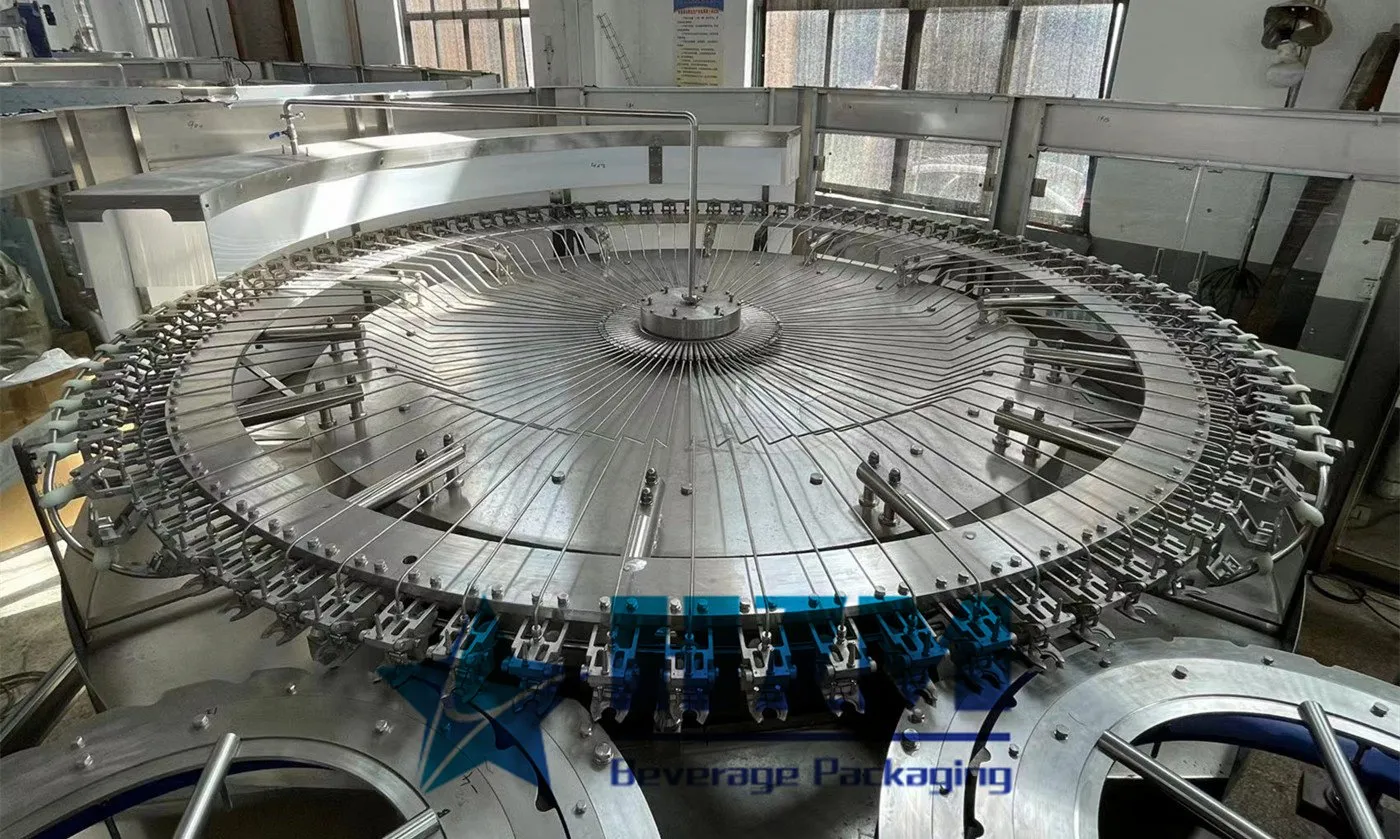
Enhancing Beverage Carbonation Equipment
Beverage carbonation equipment plays a pivotal role in producing both large and small bottled carbonated beverages. Through processes like sugar blending, it crafts preliminary beverages, which are then treated in a soda blending machine. Here, the beverage undergoes deoxygenation, followed by proportional mixing of the original syrup and water. The resulting mixture is then atomized […]
Learn more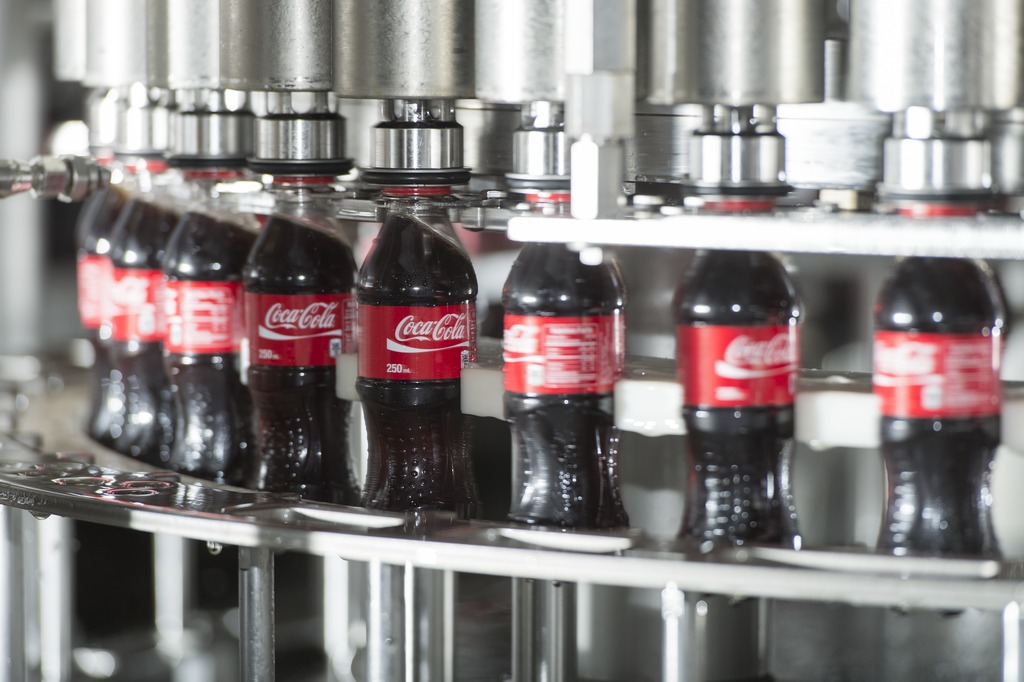
Carbonated Beverage Filling Machine Solution
Carbonated beverage filling equipment is used for filling sweetened drinks containing carbon dioxide, commonly known as carbonated drinks or carbonated beverages. They typically consist of water
Learn more