Insights & Updates
Juice Line Loses Too Much Product During CIP and Changeover
When high product loss and long recovery on a juice filling line appears, changing the nearest setpoint is tempting but risky. A durable repair starts by retaining samples, capturing the first alarm and separating a local head or lane problem from a line-wide process problem.
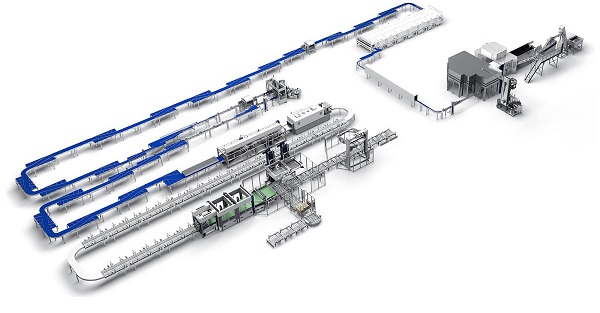
A complete production line is a chain of dependent processes: treatment or preparation, container making, filling, closure, labelling, packing, conveying and utilities. The line output is set by the slowest unstable constraint, not by the nameplate speed of one machine. The objective is not merely to clear the alarm for high product loss and long recovery on a juice filling line, but to recover a repeatable, verifiable process.
Quick answer: Measure product, water and waste around every transition. Identify mixing zones, tank heel, pipe hold-up, valve leakage, interface detection and late operator decisions before changing the validated sanitation process.
What operators usually see
Use the following signs to define the boundary of the problem. A head-by-head, lane-by-lane or time-based pattern is especially valuable: For this case, preserve evidence that shows whether large volumes go to drain at product start and end.
- Large volumes go to drain at product start and end
- Brix takes a long time to reach target
- CIP water appears in finished product risk samples
- Loss varies greatly by operator
Make the equipment safe and protect the product
Use the line-wide stop, lockout/tagout and product-hold procedures. A safe diagnosis must include adjacent machines, stored pneumatic and hydraulic energy, hot process circuits, robots and the possibility that equipment can restart from an upstream or downstream command.
Use synchronized timestamps to collect state, speed, fault, starve and block data from every major machine. Add product-quality results and utility pressure, flow, temperature and power so a local alarm can be related to the upstream event that caused it. Explicitly record whether large volumes go to drain at product start and end.
Most likely causes, in practical checking order
1. Poor interface detection
Time-only switching ignores actual concentration and flow variation To test this explanation without guessing, install or use calibrated flow and concentration measurements at key transitions Record the result before moving to the next cause.
2. Large trapped and mixed volumes
Tank heels, dead legs and low points hold product or rinse water A practical confirmation step is to build a mass balance for product, recovery and drain. Compare the finding with a known-good run.
3. Valve leakage or wrong sequence
Product and water paths communicate during transition Do not compensate for this condition in the recipe. First, map piping hold-up, drainability and valve sequence Keep the original setting and measured result in the fault record.
4. Conservative but undocumented operation
Operators add delay because previous endpoint data is not trusted Separate this cause from the others with one controlled check: review conductivity, Brix or turbidity endpoint trends Use the same product, format and speed for the comparison.
Step-by-step diagnostic procedure
Follow the sequence in order and preserve each result. Stop if any check would require defeating a guard, interlock or validated food-safety control.
- Install or use calibrated flow and concentration measurements at key transitions
- Build a mass balance for product, recovery and drain
- Map piping hold-up, drainability and valve sequence
- Review conductivity, Brix or turbidity endpoint trends
- Perform approved valve-seat checks
- Compare operator actions with actual interface arrival
Corrective actions that address the root cause
The repair must remove the mechanism, not hide its alarm. Use specified hygienic and safety-rated parts and record every change.
- Use validated measurement-based interface control
- Improve drainability and sequence before considering piping changes
- Repair leaking valves
- Create controlled transition standards with quality approval
How to verify the repair before full-speed production
A successful no-load cycle is not enough. Use the actual product and package, sample every relevant head or lane, and verify this condition: Confirm that high product loss and long recovery on a juice filling line is absent for multiple consecutive cycles, not only for one sample. Review the alarm history and keep diagnostic product segregated until the site’s quality procedure releases it.
- Confirm that high product loss and long recovery on a juice filling line is absent for multiple consecutive cycles, not only for one sample.
- Compare the repaired result for “Large volumes go to drain at product start and end” with the approved quality limit and the last known-good baseline.
- Check adjacent stations and downstream package quality for side effects associated with poor interface detection.
- For “Juice Line Loses Too Much Product During CIP and Changeover”, record the final settings, measurements, parts used and restart authorization.
Prevent the problem from returning
Use the repair evidence to improve the control plan. The following actions make recurrence visible early:
- Trend product loss per changeover
- Verify endpoint instruments
- Review hold-up in modifications
- Train from data
- Do not shorten food-safety cleaning requirements without revalidation
When to stop troubleshooting and call a specialist
Stop and contact the machine or component supplier when high product loss and long recovery on a juice filling line cannot be isolated with non-invasive checks, when it returns after an approved repair, or when calibration requires protected service tools. Specialist support is also required when the same protective fault returns after an approved repair or structural damage is suspected. Send the service engineer the fault history, photos, samples, trend data, recipe revision and work already completed.
Relevant equipment for this application
For a project-level comparison related to high product loss and long recovery on a juice filling line, see HZM Machinery’s Juice Filling Production Line. Use actual product, container and utility data when evaluating whether the configuration fits the duty.
Frequently asked questions
What should be checked first when high product loss and long recovery on a juice filling line?
Measure product, water and waste around every transition. Identify mixing zones, tank heel, pipe hold-up, valve leakage, interface detection and late operator decisions before changing the validated sanitation process. Preserve the original settings and take representative samples before repair work begins.
How can we distinguish poor interface detection from large trapped and mixed volumes?
Time-only switching ignores actual concentration and flow variation In contrast, tank heels, dead legs and low points hold product or rinse water Compare the two mechanisms under the same operating condition by completing these checks: install or use calibrated flow and concentration measurements at key transitions Then build a mass balance for product, recovery and drain
Can production continue while high product loss and long recovery on a juice filling line?
Only when the plant’s documented risk assessment and quality procedure allow it. For high product loss and long recovery on a juice filling line, stop and segregate production when package integrity, sanitation, validated processing, pressure safety, electrical protection or an uncontrolled reject trend is involved.
What evidence will help the equipment supplier respond faster?
Provide the model and serial number, product and format, target speed, first fault, timestamps, photos or video, affected station pattern and maintenance history. For this issue, also include large volumes go to drain at product start and end and the measured result from this check: compare operator actions with actual interface arrival
Talk to our engineering team
Need help planning your packaging line?
Share your product, bottle and capacity requirements for a practical equipment recommendation.
Equipment
CIP System
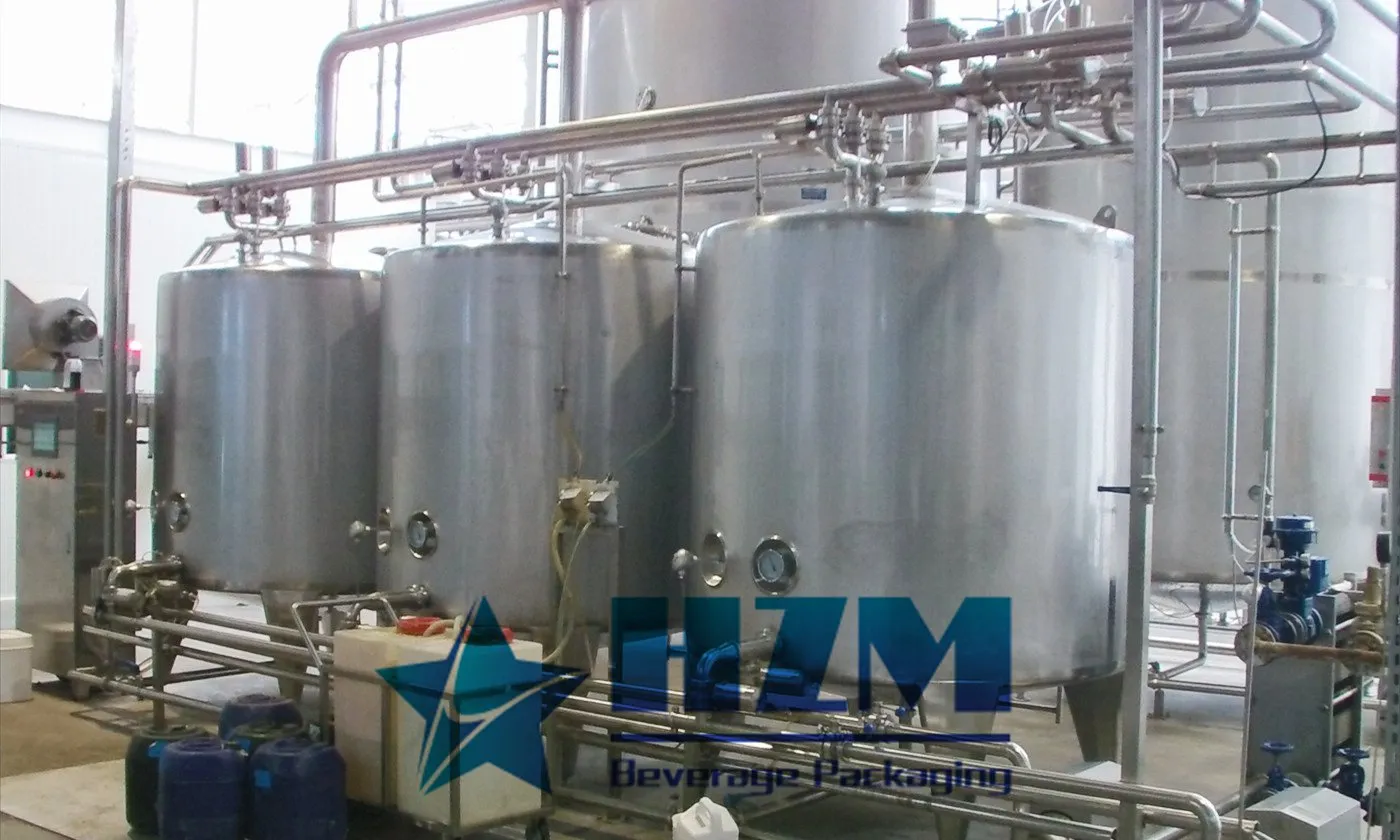
The CIP system cleans the internal surfaces of beverage tanks, pipelines and filling equipment without routine disassembly.
Learn more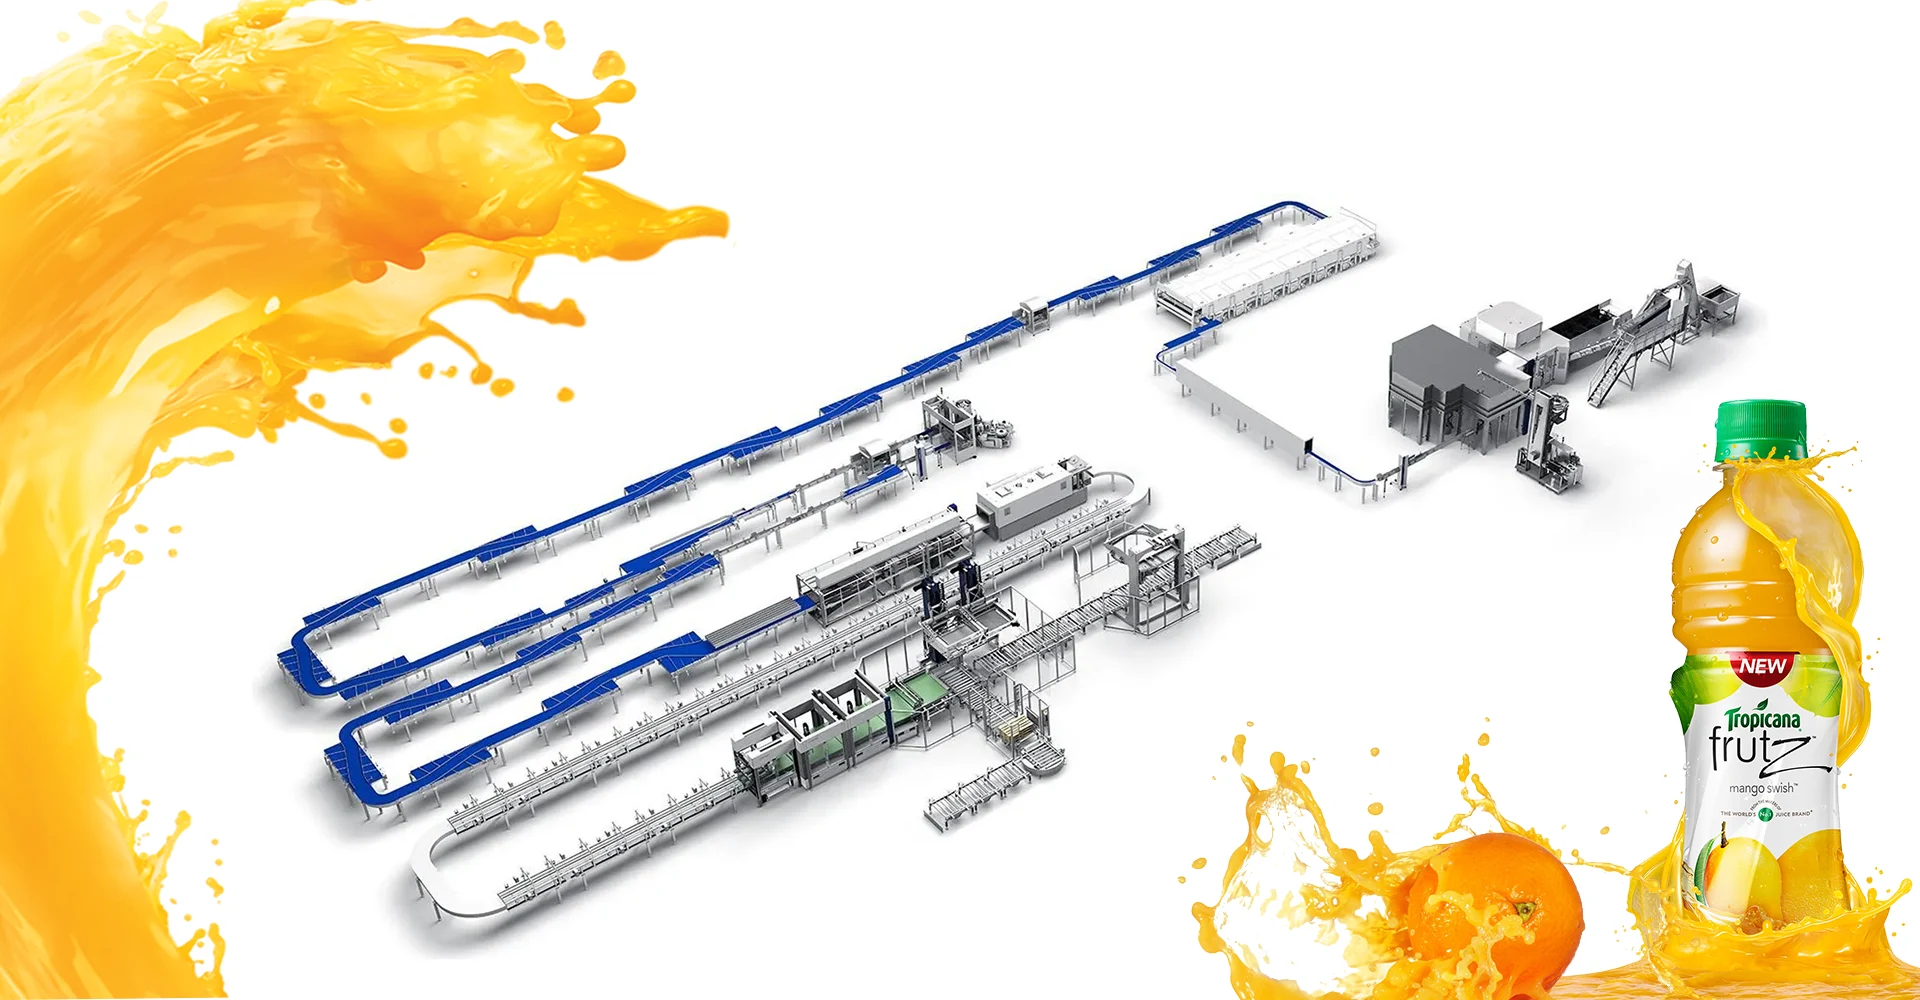
Equipment
Juice beverage bottling line
The juice beverage bottling line connects beverage preparation and thermal processing with bottle filling, capping, labelling and packing.
Learn more
Equipment
Bottled Juice Packaging Machine
Bottled juice filling equipment with rinsing and capping, from 6,000 to 18,000 bottles/hour at 500 ml.
Learn more
Equipment
PET Bottle Juice Beverage Filling Machine
PET bottle juice filling with automatic rinsing and capping, for juice, tea and still beverages.
Learn more
Equipment
Glass Bottle Juice Beverage Filling Machine
Glass bottle juice filling with rinsing and capping, for juice, tea and other still beverages.
Learn more
Equipment
juice Pulp Filling Machine 4 in 1
RXGGF16-16-5 pulp juice filling with separate pulp and liquid dosing, rinsing and capping at 5,000 bottles/hour for 250 ml bottles.
Learn more
Equipment
Automatic Pulp Juice Filling Machine
Pulp juice filling with separate pulp and liquid dosing, bottle rinsing and capping for beverages containing fruit particles.
Learn more
Equipment
PET Bottle juice Beverage Hot Filling Machine
Hot filling for juice and tea in heat-compatible PET bottles, with automatic rinsing, filling and capping.
Learn more
Equipment
Automatic Beverage Packaging Machines – Juice, Soda & Soft Drinks
HZM beverage packaging equipment connects juice, soda and soft drink filling with labelling, coding and secondary packaging.
Learn more
2024-05-14
What is a CIP cleaning system?
CIP cleaning system, also known as Clean In Place system, refers to a safe and automatic cleaning system that can be achieved through simple operation methods without dismantling production equipment.
Learn more2025-03-28
Principle and Application of CIP Cleaning System
The CIP cleaning system is an essential hygiene solution in water and beverage production. By providing an efficient and convenient cleaning process, it ensures equipment sanitation, improves production efficiency, extends equipment lifespan, and reduces energy consumption
Learn more
2025-03-02
The Role of the CIP Cleaning System in Water and Beverage Production Lines
The CIP system effectively removes these residues from the inner walls of pipelines, tanks, valves, and other equipment through powerful cleaning and sterilization, preventing microbial contamination and ensuring that products meet hygiene standards.
Learn more2023-06-09
CIP Cleaning for Juice Filling Machines: Process and System Selection
A practical guide to planning CIP cleaning for juice tanks, pipelines and filling machines, including circuit design, cycle control and verification.
Learn more
2023-12-04
Why Beverage Filling Machines Must Have CIP Cleaning Systems?
CIP (Cleaning In Place) cleaning systems are essential in the realm of food and beverage production, particularly for dairy processing equipment and pipelines. Over time, these components accumulate deposits that, if not cleaned thoroughly and promptly, can directly impact product quality and result in various issues such as substandard packaged foods.
Learn more2023-06-09
Juice and Tea Filling Line Guide: Formula Changeover and Product Recovery
Practical HZM guidance on juice and tea filling line, focused on formula changeover and product recovery, line integration, RFQ data and measurable acceptance checks.
Learn more