Insights & Updates
PET Bottle Wall Thickness Is Uneven: How to Read the Defect
When uneven material distribution in stretch-blown PET bottles appears, changing the nearest setpoint is tempting but risky. A durable repair starts by retaining samples, capturing the first alarm and separating a local head or lane problem from a line-wide process problem.
A PET bottle defect can originate in preform quality, heating, stretching, pre-blow, final blow, mould cooling or transfer. The location and symmetry of the defect usually reveal which process window moved. The objective is not merely to clear the alarm for uneven material distribution in stretch-blown PET bottles, but to recover a repeatable, verifiable process.
Quick answer: Map thickness by bottle section and blow cavity, then check preform centering, oven profile, stretch timing, pre-blow curve, final pressure and mould cooling. The location of excess and missing material identifies which step moved.
What operators usually see
Use the following signs to define the boundary of the problem. A head-by-head, lane-by-lane or time-based pattern is especially valuable: For this case, preserve evidence that shows whether one sidewall is thin while the opposite side is heavy.
- One sidewall is thin while the opposite side is heavy
- Base and shoulder weights change between cavities
- Bottles fail top-load or burst tests intermittently
- The defect follows a heating spindle or blowing station
Make the equipment safe and protect the product
Isolate high-pressure air, electrical power, heating circuits and motion energy before entering the guarded area. Treat hot oven components and pressurized blowing circuits as stored-energy hazards.
Keep samples by cavity and timestamp. Record preform lot, resin or rPET content, oven profile, pre-blow timing and pressure, final pressure, stretch-rod position, mould temperature and cooling-water conditions. Explicitly record whether one sidewall is thin while the opposite side is heavy.
Most likely causes, in practical checking order
1. Asymmetric preform heating
Lamp condition, reflector contamination or spindle rotation leaves one side hotter and easier to stretch To test this explanation without guessing, retain cavity-coded bottles and preforms from the same time window Record the result before moving to the next cause.
2. Preform or stretch-rod miscentering
Material is pulled off-axis during axial stretch A practical confirmation step is to measure sectional weight or thickness using the plant’s approved method. Compare the finding with a known-good run.
3. Incorrect pre-blow timing or pressure
Radial expansion begins too early or too late relative to stretch Do not compensate for this condition in the recipe. First, check preform surface-temperature profile and spindle rotation by channel Keep the original setting and measured result in the fault record.
4. Cavity-specific pneumatic or mechanical drift
Pressure curve, valve response or worn components differ at one station Separate this cause from the others with one controlled check: verify neck support, preform centering and stretch-rod alignment Use the same product, format and speed for the comparison.
Step-by-step diagnostic procedure
Follow the sequence in order and preserve each result. Stop if any check would require defeating a guard, interlock or validated food-safety control.
- Retain cavity-coded bottles and preforms from the same time window
- Measure sectional weight or thickness using the plant’s approved method
- Check preform surface-temperature profile and spindle rotation by channel
- Verify neck support, preform centering and stretch-rod alignment
- Compare pre-blow and final-blow pressure curves by cavity
- Inspect mechanical wear and calibration at the repeating station
Corrective actions that address the root cause
The repair must remove the mechanism, not hide its alarm. Use specified hygienic and safety-rated parts and record every change.
- Clean and balance the heating channel and replace failed lamps or reflectors
- Align the preform path and stretch rod
- Restore the validated stretch and pre-blow relationship
- Service the cavity-specific valve, seal or mechanism and recalibrate
How to verify the repair before full-speed production
A successful no-load cycle is not enough. Use the actual product and package, sample every relevant head or lane, and verify this condition: Confirm that uneven material distribution in stretch-blown pet bottles is absent for multiple consecutive cycles, not only for one sample. Review the alarm history and keep diagnostic product segregated until the site’s quality procedure releases it.
- Confirm that uneven material distribution in stretch-blown pet bottles is absent for multiple consecutive cycles, not only for one sample.
- Compare the repaired result for “One sidewall is thin while the opposite side is heavy” with the approved quality limit and the last known-good baseline.
- Check adjacent stations and downstream package quality for side effects associated with asymmetric preform heating.
- For “PET Bottle Wall Thickness Is Uneven: How to Read the Defect”, record the final settings, measurements, parts used and restart authorization.
Prevent the problem from returning
Use the repair evidence to improve the control plan. The following actions make recurrence visible early:
- Trend sectional weight by cavity
- Clean reflectors and verify spindle rotation
- Inspect stretch rods for alignment and wear
- Record pressure curves after maintenance
- Qualify preform or rPET changes with full bottle tests
When to stop troubleshooting and call a specialist
Stop and contact the machine or component supplier when uneven material distribution in stretch-blown pet bottles cannot be isolated with non-invasive checks, when it returns after an approved repair, or when calibration requires protected service tools. Specialist support is also required when the same protective fault returns after an approved repair or structural damage is suspected. Send the service engineer the fault history, photos, samples, trend data, recipe revision and work already completed.
Relevant equipment for this application
For a project-level comparison related to uneven material distribution in stretch-blown PET bottles, see HZM Machinery’s Automatic PET Stretch Blow Molding Machine. Use actual product, container and utility data when evaluating whether the configuration fits the duty.
Frequently asked questions
What should be checked first when uneven material distribution in stretch-blown PET bottles?
Map thickness by bottle section and blow cavity, then check preform centering, oven profile, stretch timing, pre-blow curve, final pressure and mould cooling. The location of excess and missing material identifies which step moved. Preserve the original settings and take representative samples before repair work begins.
How can we distinguish asymmetric preform heating from preform or stretch-rod miscentering?
Lamp condition, reflector contamination or spindle rotation leaves one side hotter and easier to stretch In contrast, material is pulled off-axis during axial stretch Compare the two mechanisms under the same operating condition by completing these checks: retain cavity-coded bottles and preforms from the same time window Then measure sectional weight or thickness using the plant’s approved method
Can production continue while uneven material distribution in stretch-blown PET bottles?
Only when the plant’s documented risk assessment and quality procedure allow it. For uneven material distribution in stretch-blown PET bottles, stop and segregate production when package integrity, sanitation, validated processing, pressure safety, electrical protection or an uncontrolled reject trend is involved.
What evidence will help the equipment supplier respond faster?
Provide the model and serial number, product and format, target speed, first fault, timestamps, photos or video, affected station pattern and maintenance history. For this issue, also include one sidewall is thin while the opposite side is heavy and the measured result from this check: inspect mechanical wear and calibration at the repeating station
Talk to our engineering team
Need help planning your packaging line?
Share your product, bottle and capacity requirements for a practical equipment recommendation.
Equipment
Automatic Blow Molding Machine
Automatic PET bottle blowing for water and beverage packaging, with capacities of 12,000–24,000 bottles/hour at 500 ml.
Learn more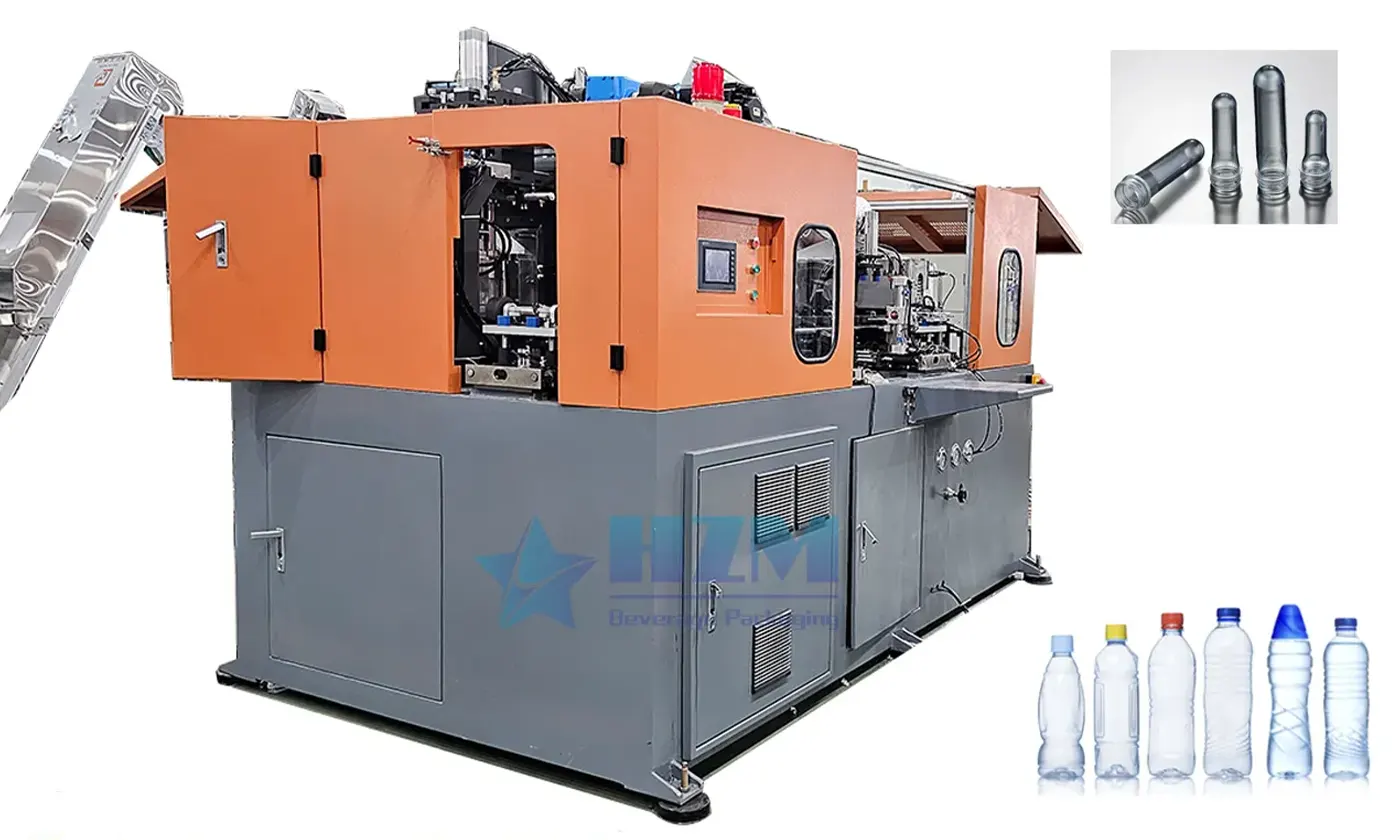
Equipment
PET Bottle Blow Molding Machine
PET bottle blow moulding with 6–12 cavities and capacities of 12,000–21,600 bottles/hour at 500 ml.
Learn more
Equipment
Full Electric Servo Type Blow Molding Machine
Full-electric servo PET blow moulding with 4, 6, 9 or 10 cavities and capacities of 5,400–13,000 bottles/hour at 500 ml.
Learn more
Equipment
Automatic Water Bottle Blowing Molding Machine
Automatic water bottle blowing from PET preforms, with 6–12 cavities and capacities up to 21,600 bottles/hour at 500 ml.
Learn moreEquipment
Automatic PET Stretch Blow Molding Machine
Automatic PET stretch blow moulding with 2, 4 or 6 cavities and HZM-ECO model capacities of 1,800–7,000 bottles/hour.
Learn more
Equipment
Automatic Rotary Blow Molding Machine
Rotary PET bottle blow moulding for water and beverage packaging, with 6–24 cavities and capacities up to 48,000 bottles/hour at 500 ml.
Learn more
Equipment
Blowing-Filling-Capping Machine
A PET combiblock that combines preform heating, bottle blowing, filling and capping at 12,000–48,000 bottles/hour at 500 ml.
Learn more
Equipment
5 Gallon Bottle Blow Molding Machine
This blow moulding machine produces large PET water bottles, including 5-gallon containers.
Learn more
Equipment
Automatic Oil Bottle Wide Neck PET Bottle Blowing Machine
PET blow moulding equipment for large edible-oil, drinking-water and wide-neck bottles, with bottle sizes up to 5–10 L by model.
Learn more2023-06-09
Solutions for Blow Molding Plastic Bottles
This article will discuss the price, HZM manufacturer, functions, applicable industries, solutions, procurement considerations, and maintenance techniques related to blow molding machines.
Learn more2023-06-09
PET Blow Molding System Guide: Preform Heating and Bottle Wall Distribution
Practical HZM guidance on pet blow molding system, focused on preform heating and bottle wall distribution, line integration, RFQ data and measurable acceptance checks.
Learn more2023-06-07
How Much Does a Blow Molding Machine Cost?
we will explore the various factors that influence the cost of a blow molding machine and provide insights into the pricing range.
Learn more2023-06-08
how does a blow molding machine work
How Does a Blow Molding Machine Work? Exploring the Process with HZM Blow Molding Machine Manufacturer
Learn more2023-06-09
High Efficiency 28000 BPH Automatic Pet Blow Molding Machine
High quality High Efficiency 28000 BPH Automatic Pet Blow Molding Machine from China, China's leading 28000 BPH Automatic Pet Blow Molding Machine product, with strict quality control 28000 BPH Auto Pet Blow Molding Machine factories, producing high quality 800 BPH Blow Molding Machine products.
Learn more
2023-11-23
User What are the three types of blow moulding?
Blow molding is a manufacturing process used to produce hollow plastic parts. There are three main types of blow molding: 1、Extrusion Blow Molding (EBM) This is the most common type of blow molding. In EBM, a continuous tube of plastic, called a parison, is extruded (pushed out) from an extruder. The parison is then enclosed […]
Learn more