Insights & Updates
RO Membrane Scaling: How to Confirm It Before Cleaning
The cost of mineral scaling in a reverse-osmosis membrane system is not limited to the visible reject. It can include product giveaway, rework, unstable downstream operation and hours spent correcting the wrong variable.
Water-treatment performance must be evaluated with normalized operating data. Raw-water changes, temperature, recovery, pressure, flow and conductivity interact; a single gauge reading is not enough to identify membrane damage or fouling. The objective is not merely to clear the alarm for mineral scaling in a reverse-osmosis membrane system, but to recover a repeatable, verifiable process.
Quick answer: Do not identify scale from low flow alone. Use feed analysis, recovery, pH, concentrate chemistry, stage location and deposit analysis to distinguish carbonate, sulfate, silica or other scale before choosing a cleaner.
What operators usually see
Use the following signs to define the boundary of the problem. A head-by-head, lane-by-lane or time-based pattern is especially valuable: For this case, preserve evidence that shows whether tail-stage pressure drop or salt passage increases.
- Tail-stage pressure drop or salt passage increases
- Normalized permeate flow declines
- A hard mineral deposit appears on concentrate-end elements
- The problem follows higher recovery or antiscalant interruption
Make the equipment safe and protect the product
Use the plant chemical-handling procedure, suitable PPE and lockout/tagout. Depressurize housings and verify that cleaning chemicals have been displaced before opening a pump, filter or membrane vessel.
Trend feed, concentrate and permeate flows; stage pressures; differential pressure; conductivity; temperature; pH; oxidant residual; and recovery. Compare normalized values with the accepted commissioning baseline. Explicitly record whether tail-stage pressure drop or salt passage increases.
Most likely causes, in practical checking order
1. Recovery above design
Excess water removal concentrates sparingly soluble salts beyond their limit To test this explanation without guessing, obtain a current complete feed-water analysis and compare with design values Record the result before moving to the next cause.
2. Incorrect antiscalant dose or selection
Pump loss of prime, empty chemical tank or unsuitable chemistry removes scale protection A practical confirmation step is to calculate actual recovery from calibrated flows. Compare the finding with a known-good run.
3. Feed pH or composition change
Alkalinity, hardness, sulfate, silica or temperature differs from the design analysis Do not compensate for this condition in the recipe. First, verify antiscalant tank level, pump stroke, calibration and injection point Keep the original setting and measured result in the fault record.
4. Poor concentrate flow distribution
Restriction or element condition creates local supersaturation Separate this cause from the others with one controlled check: review pH and concentrate conductivity trends Use the same product, format and speed for the comparison.
Step-by-step diagnostic procedure
Follow the sequence in order and preserve each result. Stop if any check would require defeating a guard, interlock or validated food-safety control.
- Obtain a current complete feed-water analysis and compare with design values
- Calculate actual recovery from calibrated flows
- Verify antiscalant tank level, pump stroke, calibration and injection point
- Review pH and concentrate conductivity trends
- Identify the affected stage and collect deposit for suitable analysis
- Select cleaning chemistry only after confirming material compatibility and likely scale type
Corrective actions that address the root cause
The repair must remove the mechanism, not hide its alarm. Use specified hygienic and safety-rated parts and record every change.
- Return recovery and concentrate flow to the calculated design condition
- Restore and calibrate antiscalant dosing and correct injection mixing
- Adjust pH control only under the approved water-treatment design
- Perform a manufacturer-approved staged cleaning and replace irreversibly damaged elements
How to verify the repair before full-speed production
A successful no-load cycle is not enough. Use the actual product and package, sample every relevant head or lane, and verify this condition: Confirm that mineral scaling in a reverse-osmosis membrane system is absent for multiple consecutive cycles, not only for one sample. Review the alarm history and keep diagnostic product segregated until the site’s quality procedure releases it.
- Confirm that mineral scaling in a reverse-osmosis membrane system is absent for multiple consecutive cycles, not only for one sample.
- Compare the repaired result for “Tail-stage pressure drop or salt passage increases” with the approved quality limit and the last known-good baseline.
- Check adjacent stations and downstream package quality for side effects associated with recovery above design.
- For “RO Membrane Scaling: How to Confirm It Before Cleaning”, record the final settings, measurements, parts used and restart authorization.
Prevent the problem from returning
Use the repair evidence to improve the control plan. The following actions make recurrence visible early:
- Reassess scale projection when source water changes seasonally
- Interlock RO operation to confirmed chemical dose where appropriate
- Calibrate chemical pumps and flows
- Trend tail-stage performance
- Keep cleaning pH, temperature and exposure within membrane limits
When to stop troubleshooting and call a specialist
Stop and contact the machine or component supplier when mineral scaling in a reverse-osmosis membrane system cannot be isolated with non-invasive checks, when it returns after an approved repair, or when calibration requires protected service tools. Stop local work when safe diagnosis requires protected service tools, energized access or a change to a validated process. Send the service engineer the fault history, photos, samples, trend data, recipe revision and work already completed.
Relevant equipment for this application
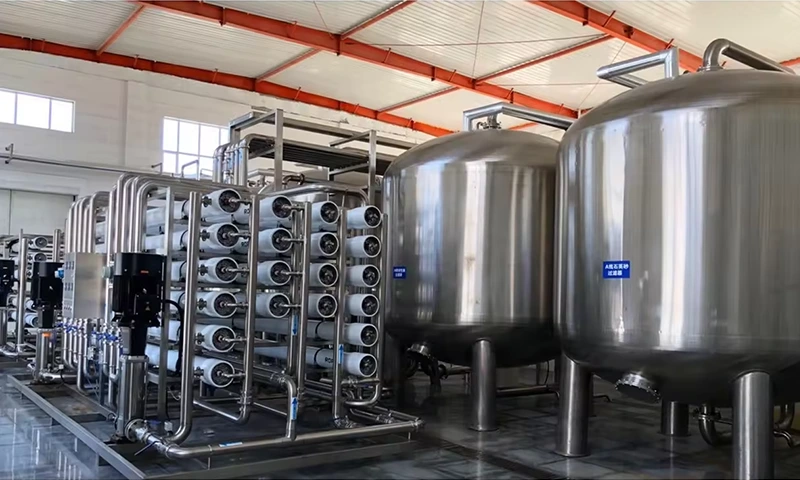
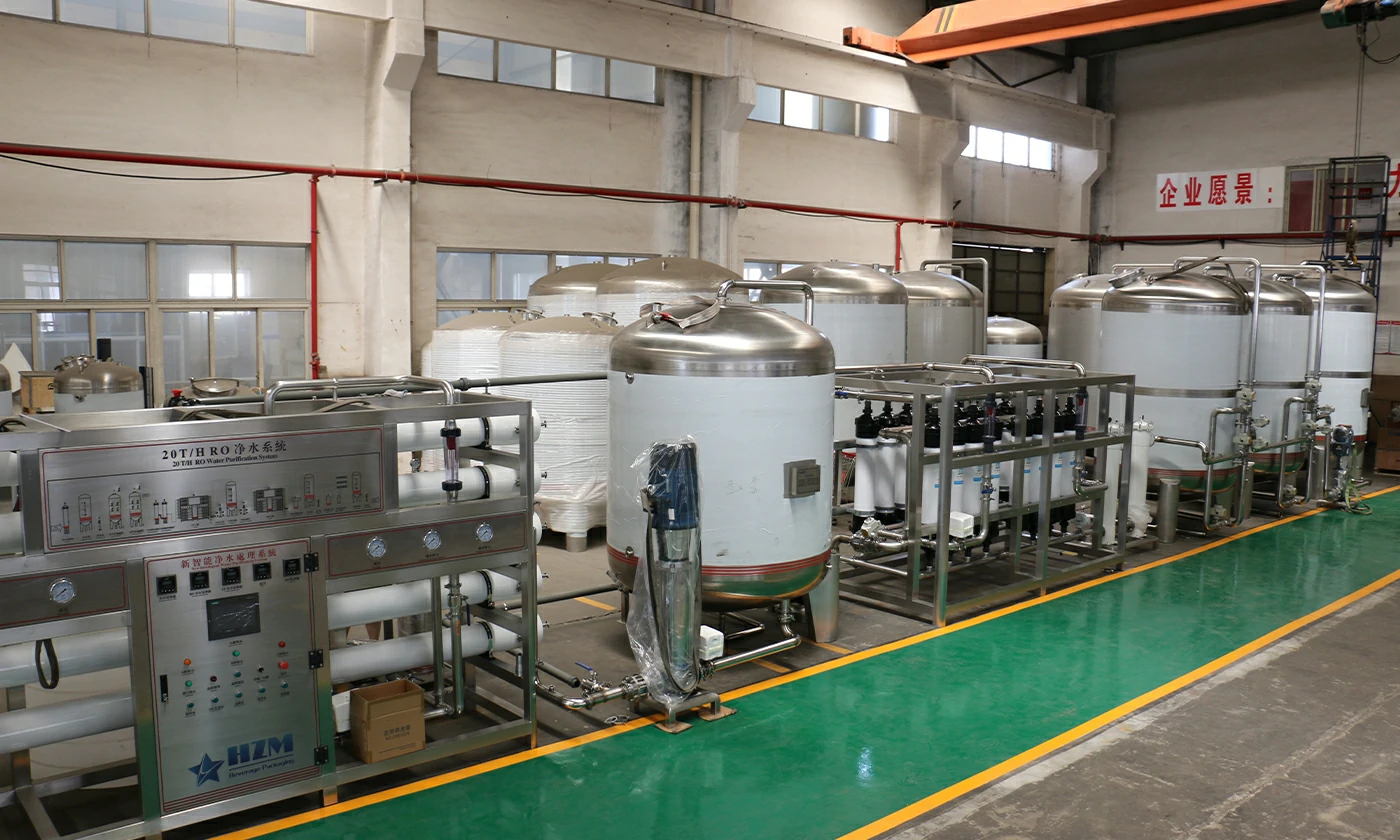
Where mineral scaling in a reverse-osmosis membrane system reveals an application mismatch rather than a maintenance fault, review the Industrial food water treatment equipment – 10T/H RO Water Treatment System. A useful technical discussion includes the real bottle, closure, product properties, pack format and site conditions.
Frequently asked questions
What should be checked first when mineral scaling in a reverse-osmosis membrane system?
Do not identify scale from low flow alone. Use feed analysis, recovery, pH, concentrate chemistry, stage location and deposit analysis to distinguish carbonate, sulfate, silica or other scale before choosing a cleaner. Preserve the original settings and take representative samples before repair work begins.
How can we distinguish recovery above design from incorrect antiscalant dose or selection?
Excess water removal concentrates sparingly soluble salts beyond their limit In contrast, pump loss of prime, empty chemical tank or unsuitable chemistry removes scale protection Compare the two mechanisms under the same operating condition by completing these checks: obtain a current complete feed-water analysis and compare with design values Then calculate actual recovery from calibrated flows
Can production continue while mineral scaling in a reverse-osmosis membrane system?
Only when the plant’s documented risk assessment and quality procedure allow it. For mineral scaling in a reverse-osmosis membrane system, stop and segregate production when package integrity, sanitation, validated processing, pressure safety, electrical protection or an uncontrolled reject trend is involved.
What evidence will help the equipment supplier respond faster?
Provide the model and serial number, product and format, target speed, first fault, timestamps, photos or video, affected station pattern and maintenance history. For this issue, also include tail-stage pressure drop or salt passage increases and the measured result from this check: select cleaning chemistry only after confirming material compatibility and likely scale type
Talk to our engineering team
Need help planning your packaging line?
Share your product, bottle and capacity requirements for a practical equipment recommendation.
Equipment
Industrial RO Drinking Water Treatment Plant – Reverse Osmosis Equipment for Beverage & Bottled Water
1,000 litres/hour reverse osmosis water treatment for bottled-water, beverage and food production.
Learn more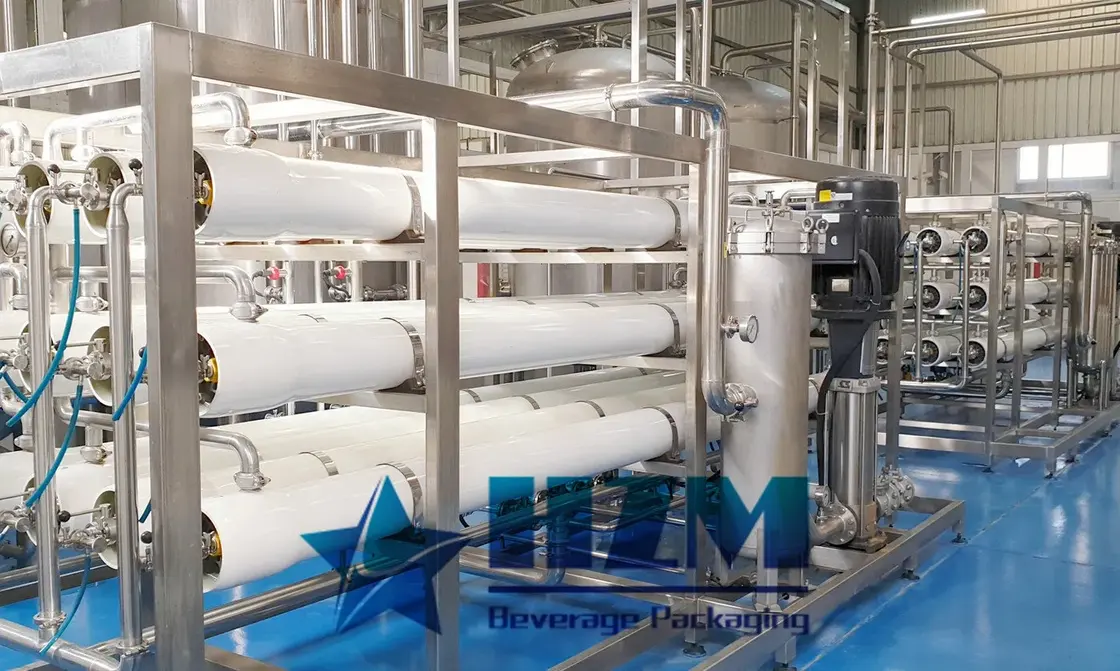
Equipment
Water Treatment System
HZM water treatment systems prepare process water for bottled water, beverages and brewing.
Learn moreEquipment
reverse osmosis water treatment
The reverse osmosis system treats water for bottled-water and beverage production.
Learn more
Equipment
Water Treatment Machine Purification System
HZM water purification equipment combines filtration, membrane treatment and final treatment in one process.
Learn more
Equipment
RO System Water Treatment Plant
The RO water treatment plant produces purified water through feed-water pretreatment and reverse-osmosis membrane separation.
Learn moreEquipment
RO Water Treatment Machine for Bottled Water Production
10 T/H reverse osmosis water treatment for purified-water bottling, with pretreatment, storage and filler-supply connections.
Learn moreEquipment
Water Treatment for the Food & Beverage Industry – RO Water Treatment Equipment
10 T/H RO water treatment for ingredient, process and rinse water in food and beverage plants.
Learn moreEquipment
Industrial food water treatment equipment – 10T/H RO Water Treatment System
10 T/H reverse osmosis water treatment for food and beverage production, with pretreatment and stainless-steel equipment options.
Learn more
Equipment
Industrial Drinking Water Treatment System
This industrial drinking-water treatment system supplies treated water to bottling and beverage plants.
Learn more2026-08-25
RO Permeate Conductivity Is High: Membrane, O-Ring or Process?
Confirm the conductivity instrument and temperature compensation, then determine whether the change affects one vessel, one stage or the whole train. Check recovery, oxidation, membrane damage, interconnector O-rings and permeate backpressure. Follow this practical fault-isolation, repair and prevention guide for bottling-line operators and maintenance teams.
Learn more2024-07-04
Commercial industrial reverse osmosis machine
Industrial reverse osmosis equipment is primarily used for producing pure water for industrial production. Depending on customer requirements, different process flows are employed to produce pure water that meets the specified standards. The equipment is widely used in the food and beverage industry, laboratories, pharmaceuticals, chemicals, and other sectors. Our equipment is factory-direct, and it is exported to more than 50 countries, including South Africa, North Africa, Sudan, the United States, Europe, and Southeast Asia.
Learn more2026-09-04
RO Differential Pressure Keeps Rising: Fouling Location Matters
Locate the stage where pressure loss is increasing and relate it to normalized flow and salt passage. A first-stage rise often points to particulate or biological fouling; a later-stage rise can indicate scale, but feed analysis is required. Follow this practical fault-isolation, repair and prevention guide for bottling-line operators and maintenance teams.
Learn more2026-08-15
RO System Produces Too Little Permeate: A Data-Driven Diagnosis
Normalize flow for temperature and pressure before declaring the membranes fouled. Then check feed availability, filter differential pressure, pump performance, recovery, concentrate restriction, scaling and biological or organic fouling. Follow this practical fault-isolation, repair and prevention guide for bottling-line operators and maintenance teams.
Learn more
2026-07-25
Raw Water Analysis for a Bottling Plant: What to Test Before Buying RO Equipment
Learn which raw-water test results an equipment supplier needs to design pretreatment and RO capacity for a reliable bottled-water or beverage plant.
Learn more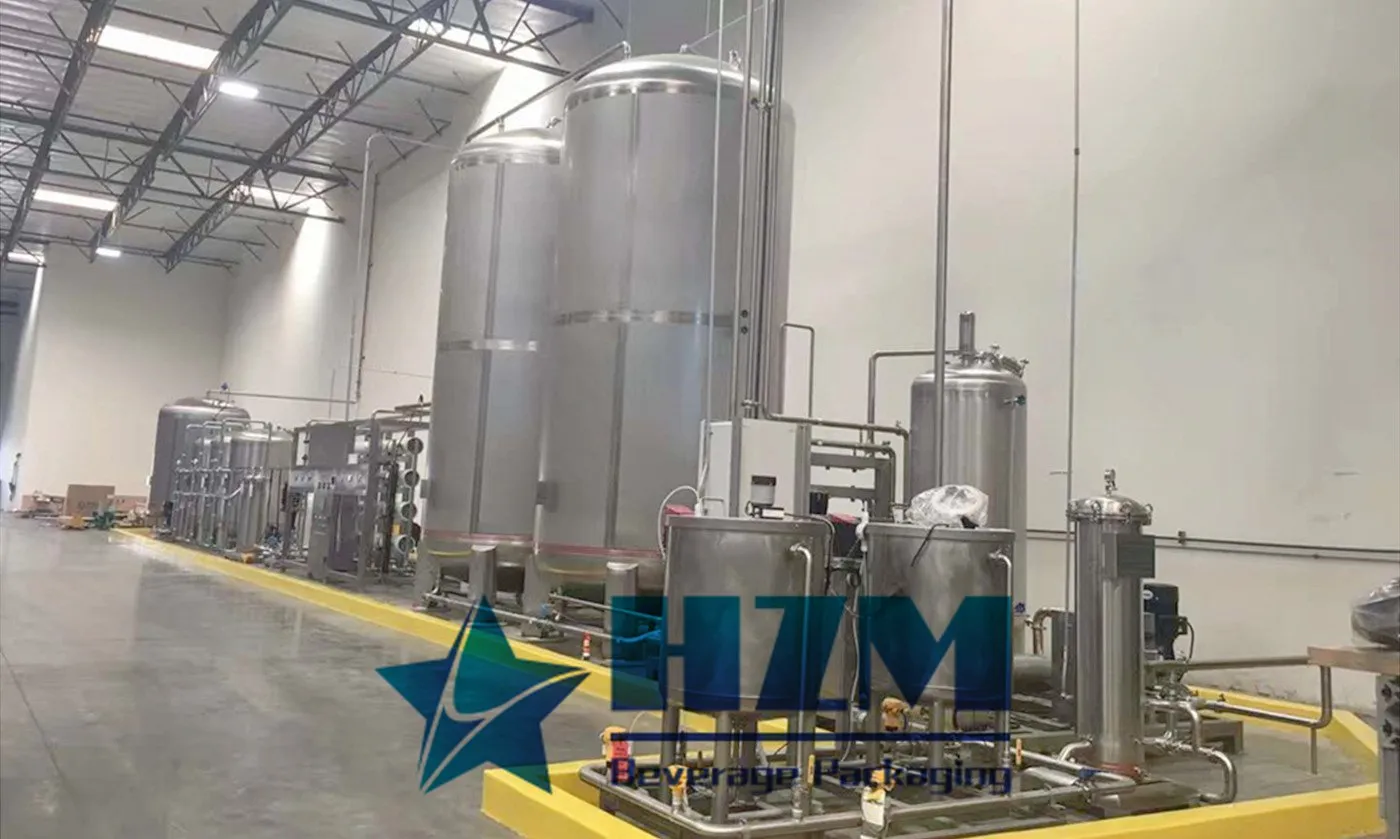
2024-03-16
Creating Healthy and Clean Drinking Water with Reverse Osmosis Purification Lines
As demands for the quality of drinking water continue to rise, reverse osmosis purification lines, as an advanced water purification technology, are gradually becoming the mainstream approach to water treatment for drinking purposes.
Learn more