Translating a PET Filler Rate into Case-Packer Demand
A case packer is usually assessed in packs per minute, while a filler is often quoted in bottles per hour. Convert between them using the actual bottles per case before comparing capacities.

Use an explicit calculation
For example, 20,000 bottles per hour packed twelve per case creates about 27.8 cases per minute before losses and interruptions. This arithmetic is a demand example, not a machine rating. A different pack count changes the required case rate.
Test the packaging cycle
Include case supply, bottle collation, closure and discharge. Inspect pack quality during replenishment and restart. A touch screen or PLC does not establish that the complete mechanism can sustain the calculated output.
Account for unavailable time
If an illustrative packer can operate for only 50 minutes in each scheduled hour, it must produce 20,000 ÷ 12 ÷ 50, or about 33.3 twelve-bottle cases per running minute, to meet the same hourly demand. Include the actual replenishment and stop history rather than applying an unexplained speed margin.
Need help planning your packaging line?
Share your product, bottle and capacity requirements for a practical equipment recommendation.
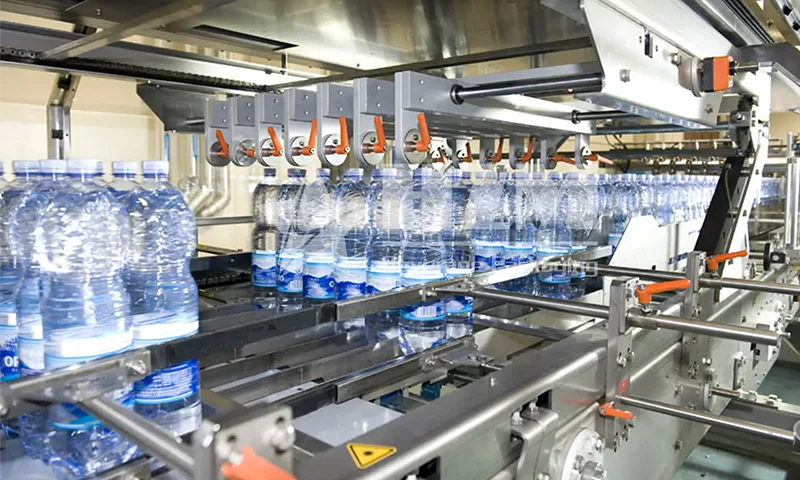
Mineral Water Bottle Packaging Machine
Automatic drinking-water production equipment with PET bottle rinsing, filling and capping, plus downstream packaging options.
Learn more
PET Bottle Water Filling Machine
PET bottle water filling with automatic rinsing and capping, for purified water, mineral water and still drinking water.
Learn more
3-in-1 PET Bottle Filling Machine , Mono-block filling machine
3-in-1 PET water bottle rinsing, filling and capping at 20,000 bottles/hour for 500 ml bottles with PCO3025 necks.
Learn more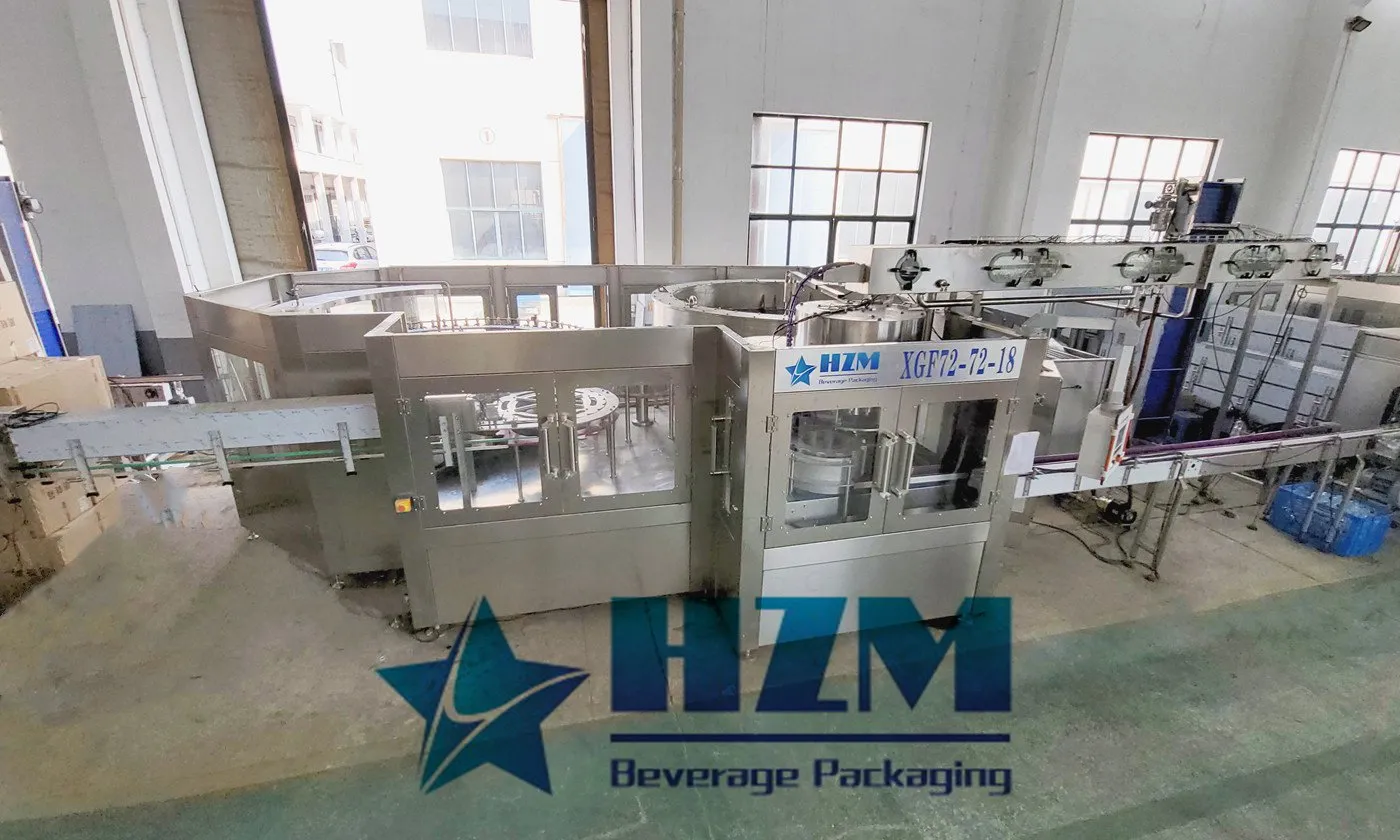
Automatic Water Bottle Filling Machine
Automatic rinsing, filling and capping for purified and mineral water in PET bottles, with capacities of 5,000–42,000 bottles/hour at 500 ml.
Learn more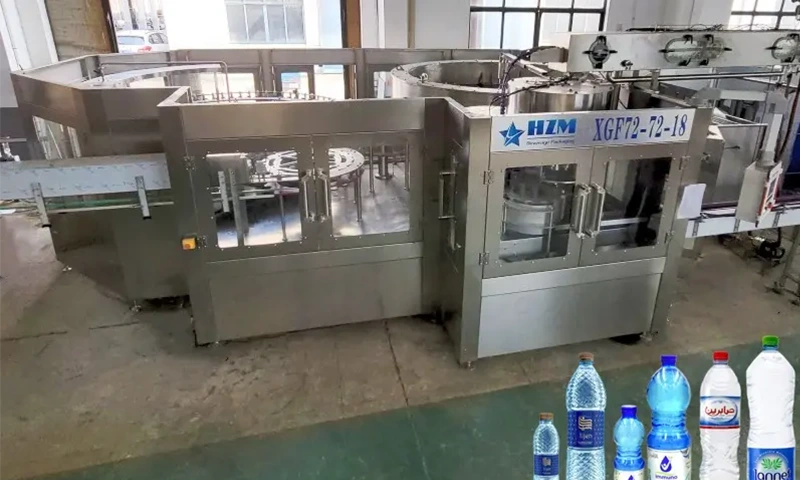
3-In-1 Water Bottle Filling Machine
A 3-in-1 PET bottle rinsing, filling and capping machine for drinking water, from 5,000 to 18,000 bottles/hour at 500 ml.
Learn more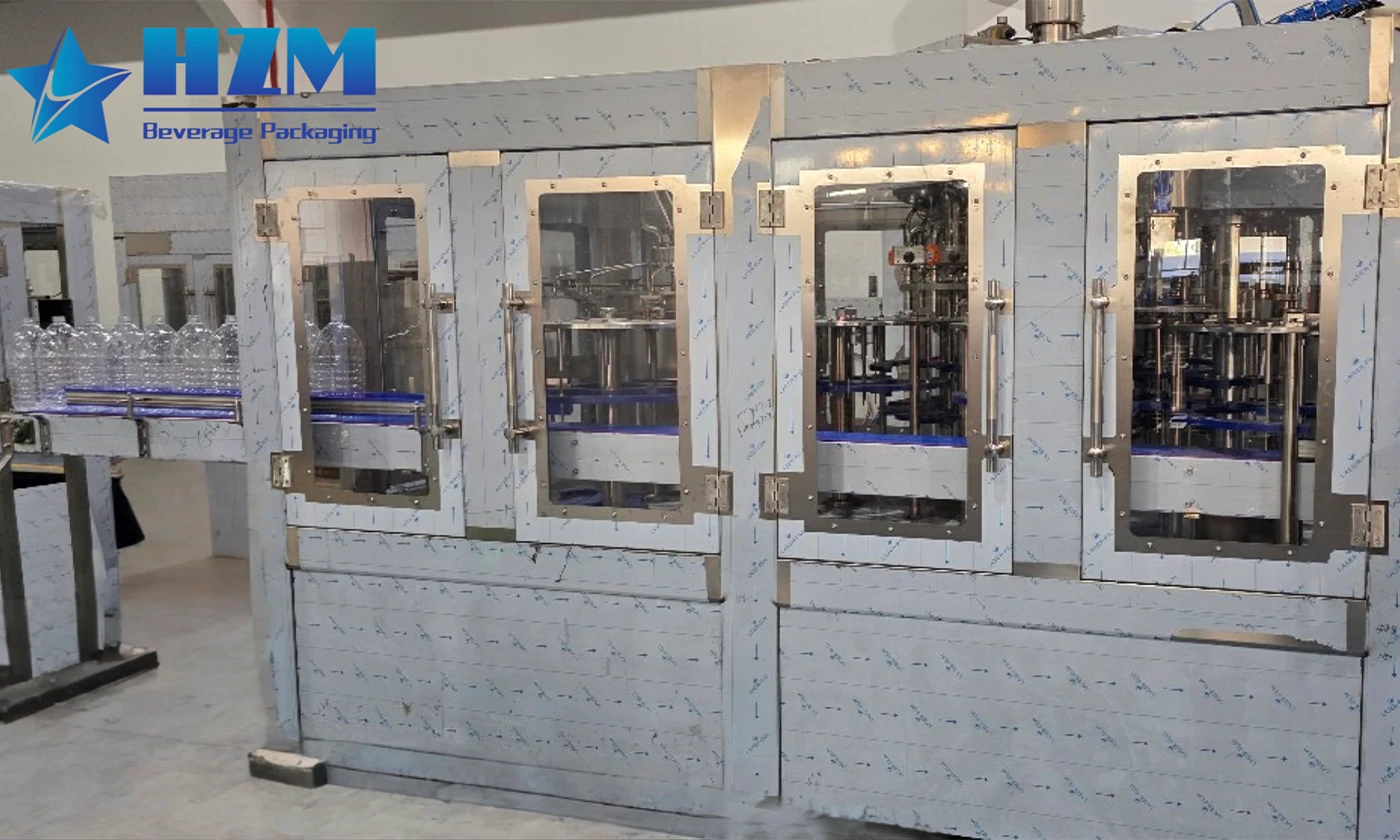
5L PET bottle flowmeter filling machine
Flowmeter water filling for 5 L PET bottles, with 12 rinsing heads, 12 filling heads and 4 capping heads.
Learn more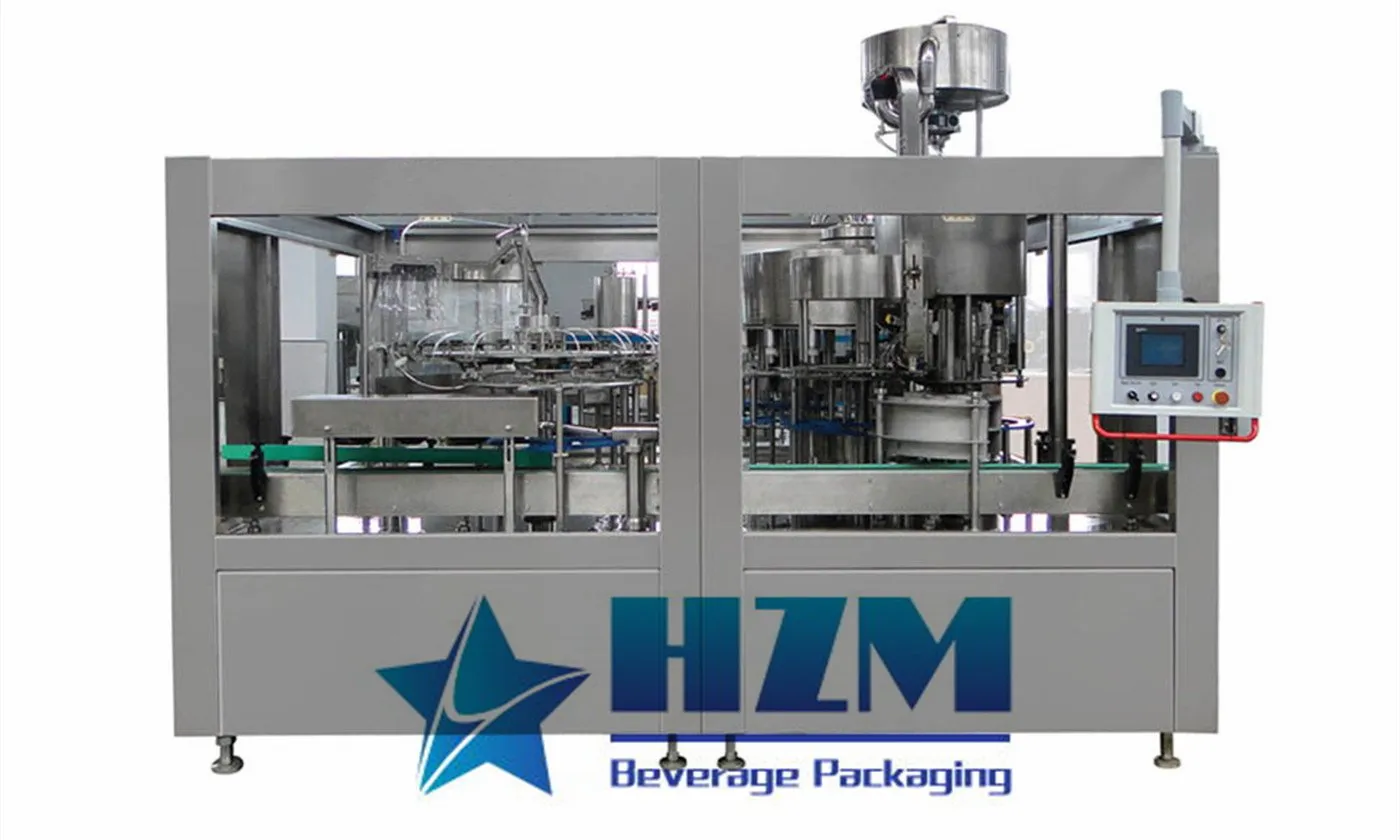
3-10L Big PET Bottle Water Filling Machine
Large PET bottle water filling equipment for 3–10 L containers, combining rinsing, filling and capping.
Learn more
Drinking water production line – Bottled Water Filling Machine Manufacturer
PET-bottled drinking-water production with automatic rinsing, filling and capping, plus water treatment and packaging equipment.
Learn more
Automatic Drinking Water Bottling Machine
Drinking-water bottling equipment with automatic rinsing, filling and capping, plus conveying, labelling and packing options.
Learn more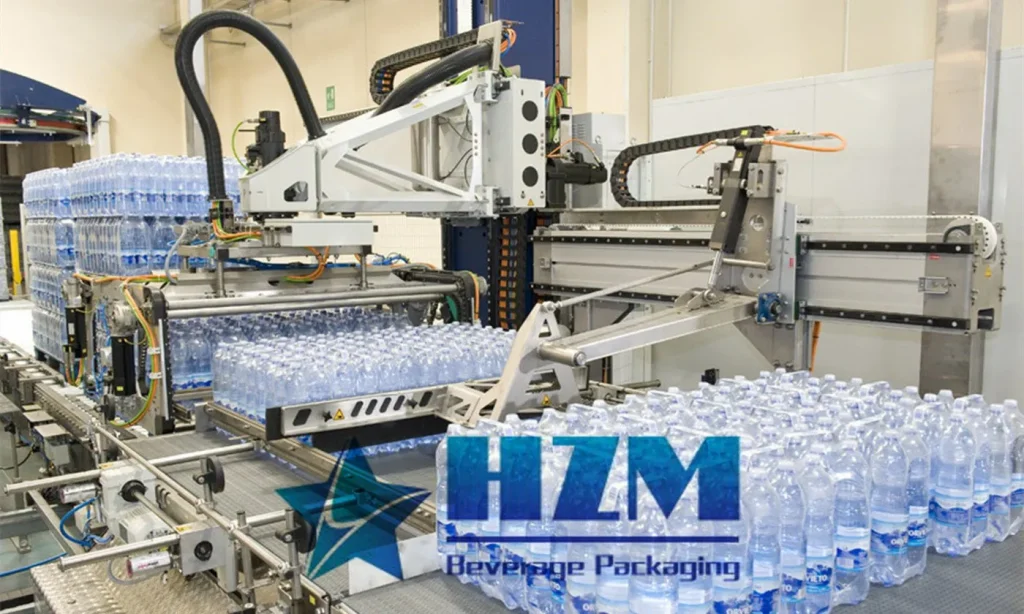
What an Automatic Palletizer Does After Case Packing
Identify palletizer infeed, layer formation or robot picking, pallet supply and discharge, then assess pack stability and the complete operating cycle.
Learn more
Inaccurate Filling or Overflow in Automatic Water Bottle Filling Machine
When using the automatic quantitative water bottle filling machine for an extended period, issues such as inaccurate filling, failure to discharge, or overflow may occur. This doesn't necessarily indicate a problem with the manufacturer's product quality, as any equipment used for an extended period can develop minor faults.
Learn more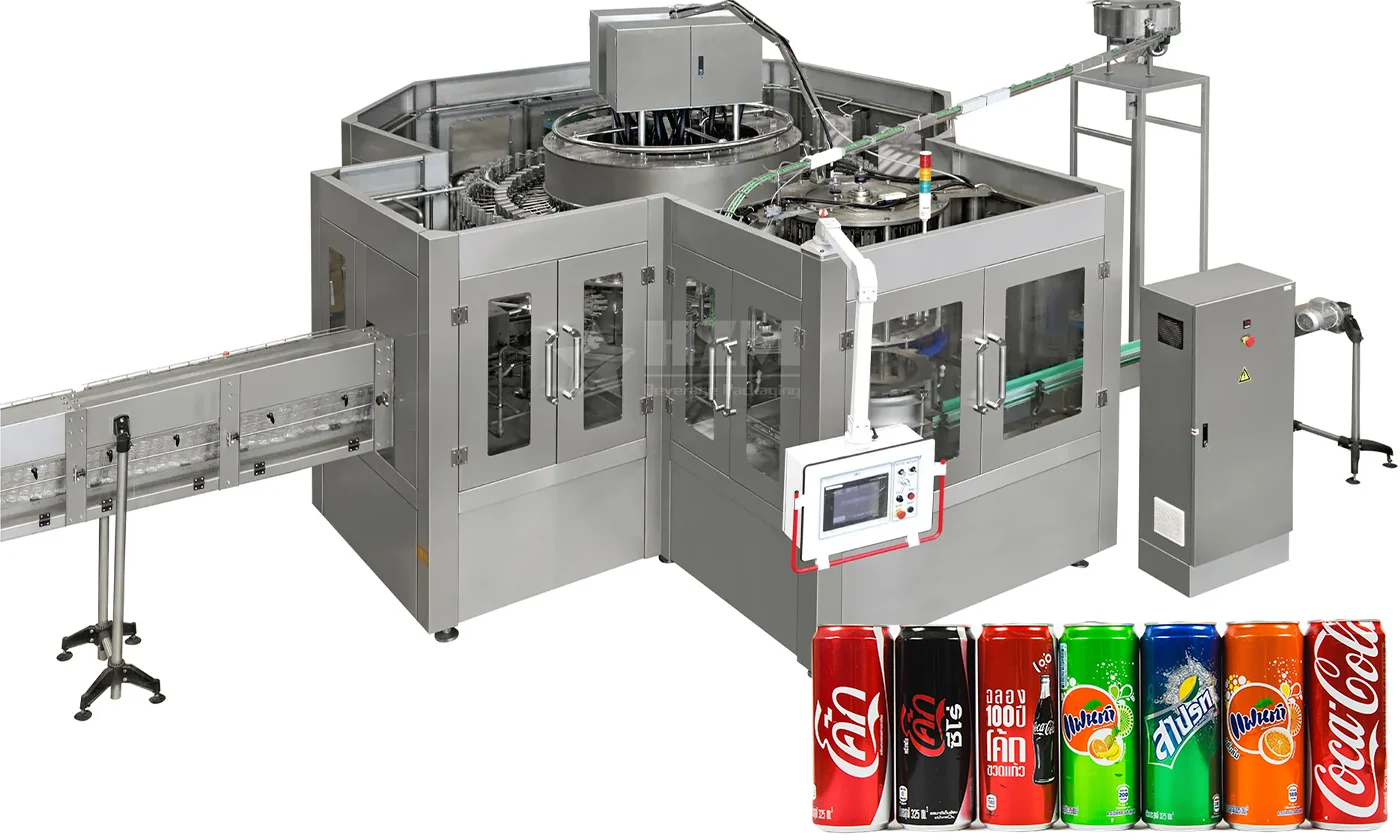
Canned CSD Filling Machine Is In High Demand
Our company is a comprehensive professional supplier of canned CSD filling machines integrating R&D, manufacturing and sales. We can provide turnkey projects and have professional after-sales service engineers.
Learn more
Accepting a Carton Packer for More Than One Beverage Pack
Each carton-packing format has a bottle group, case dimensions, closure method and required rate.
Learn moreWhy 72 Filling Valves Do Not Establish a Universal Bottle Rate
Filling-valve count is one part of a rotary filler specification. Accepted output also depends on bottle volume, filling time, handling and the complete operating sequence.
Learn more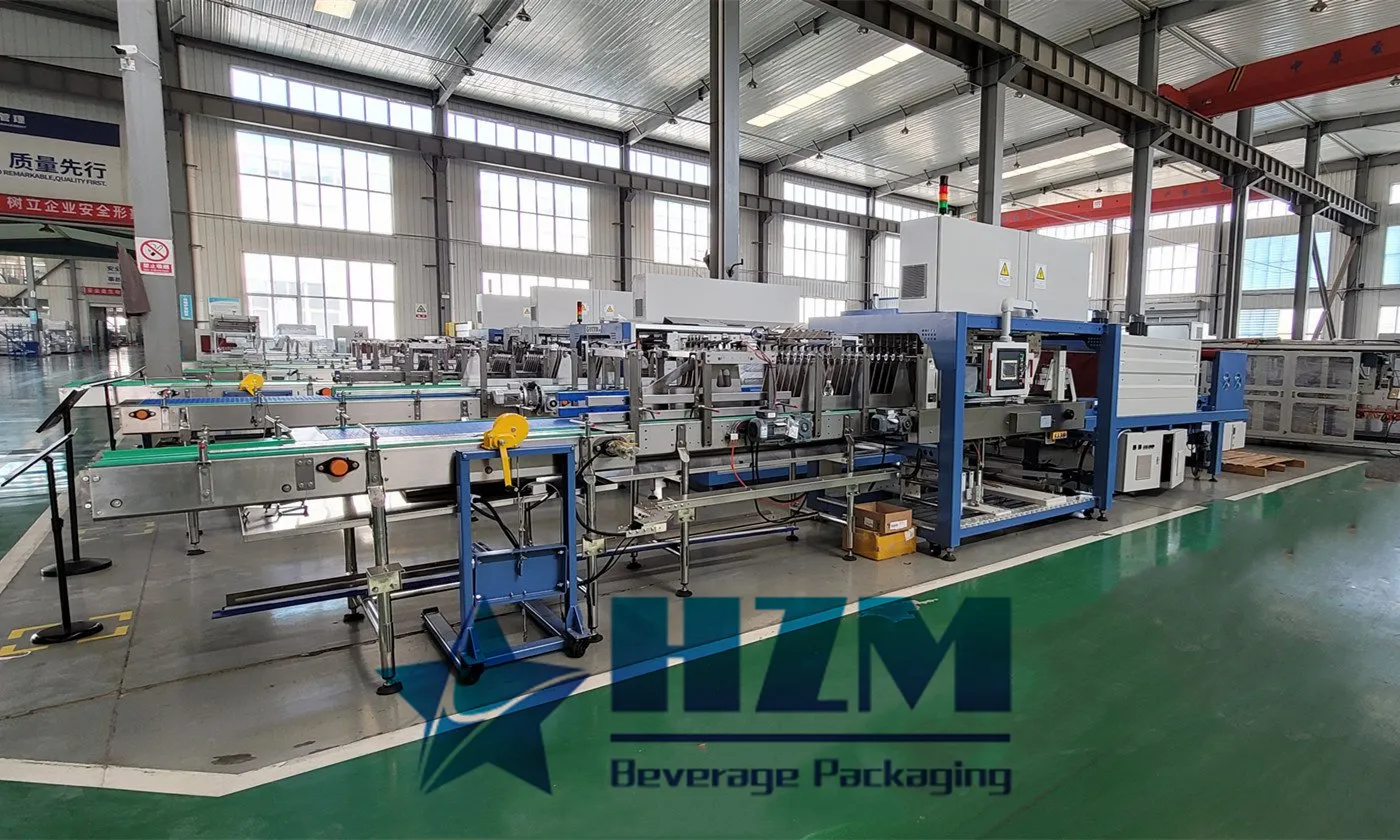
Stabilizing Bottle Infeed Before Case Packing
Packing faults often begin before the packing head. Watch the transfer from single-file bottles to the required group and identify where a bottle first rotates, tips or loses spacing.
Learn more