Insights & Updates
Capping, Sterilization, and Labeling in Beer Bottling Systems
Capping
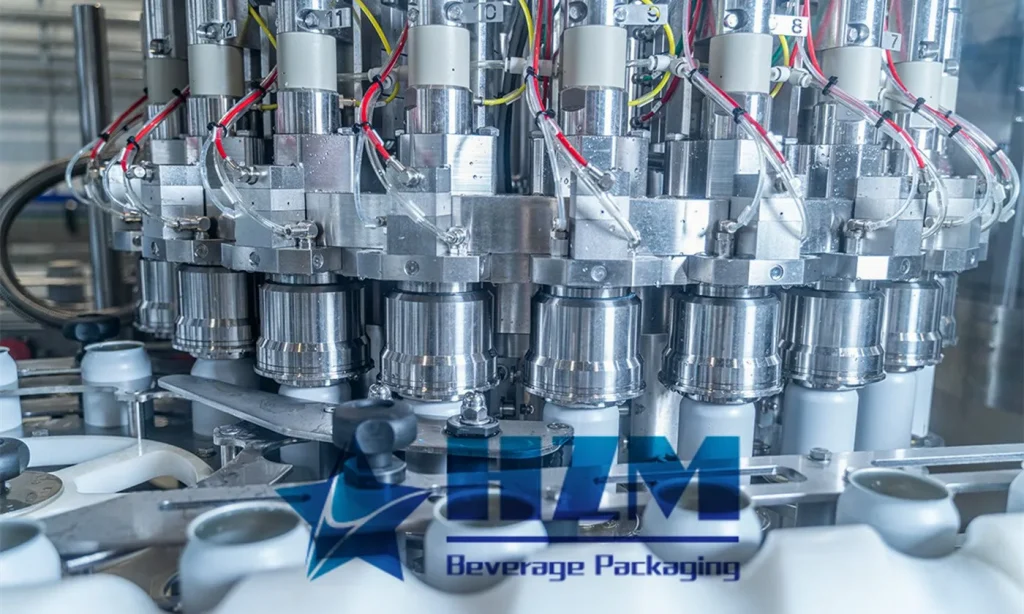
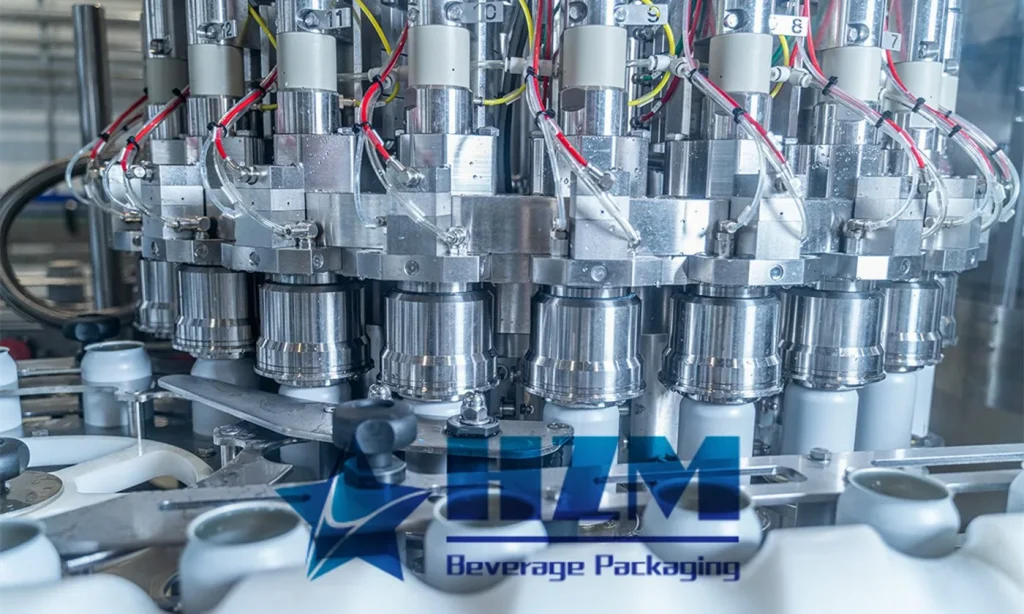
Filled beer bottles should be capped promptly, ensuring there is no air in the bottle neck during capping. Glass bottles used for beer are typically sealed with crown caps, which have 21 serrations that seal the bottle when pressed together during capping. A PVC plastic film inside the cap serves as a sealing liner. The capping machine and filling machine are installed together and driven by the same drive unit to ensure synchronized operation. The capping machine is also a rotary machine and operates much faster than the filling machine.
(1) Process Requirements:
- The size of the bottle cap must match the beer bottle, and there should be no burrs around the cap. The cap should undergo dust removal with sterile air.
- The horizontal level at the bottom of the cap-falling groove should be 0.5mm higher than the entrance to the capping head to facilitate cap insertion.
- The spring pressure should be adjusted uniformly based on the properties of the cap.
- After capping, the cap should be tightly and properly sealed without any unilateral protrusion. The capped cap should not pass through a circular hole of φ28.6mm but should pass through a φ29.1mm hole. Over-tightening can lead to bottle neck breakage, while being too loose can result in air leakage during sterilization.
(2) Capping Operation
- Measure the travel between each capping element and control the interval to achieve the best capping effect.
- Adjust the capping mold stroke and spring pressure based on the cap’s properties. Thicker crown caps or bottle liners require higher pressure.
- Control the outer diameter of the capped cap to be between φ28.6 and 29.1mm. A pressure sealing tester for caps can be used to measure the cap’s pressure resistance. A dual-needle pressure gauge can automatically display and record the cap’s maximum instantaneous pressure (0.85MPa).
Sterilization
To ensure a longer shelf life for beer, the pasteurization method is often used for sterilization to maintain high biological stability.
(1) Heat Sterilization Methods:
- Heat sterilization can be divided into pre-bottling sterilization and post-bottling sterilization. Pre-bottling sterilization, also known as flash sterilization, is often done using a plate heat exchanger. Post-bottling sterilization is the method adopted by the majority of beer production companies worldwide, and it typically uses tunnel pasteurizers or continuous pasteurization machines.
In 1860, French scientist Louis Pasteur demonstrated that the application of low-temperature sterilization (heating to 60°C and maintaining for a certain time) could kill microbial cells. This method became known as the Pasteurization method. The sterilization effect caused by heating to 60°C for 1 minute is defined as one Pasteurization unit (Pu) and is represented by Pu=T×1.393(t-60), where T is time (minutes) and t is temperature (°C). Experimental Pu values for effective sterilization of beer are typically in the range of 5–6 in the laboratory and controlled at 15–30Pu in production. Pu values at different sterilization temperatures for handling 1 minute are listed in Table 5-2-3.
Recently, instantaneous pasteurization methods such as flash pasteurization and ultra-high-temperature pasteurization (UHT, sterilization temperature between 115°C and 137°C) have been used to extend the shelf life of canned beer.
(2) Sterilization Operation:
- Post-bottling beer sterilization involves the beer to be sterilized entering the sterilization machine from one end. As it moves, the temperature inside the bottles gradually rises, reaching around 62°C (the highest sterilization temperature). It is held at this temperature for a certain period, after which the temperature inside the bottles gradually drops to near room temperature as they exit the sterilization machine and enter the adjacent labeling machine. The entire sterilization process takes about 1 hour. Pre-bottling beer sterilization involves pumping cold beer into the preheating zone for initial heating. Then, it enters the heating zone (up to 71–79°C) for a specific time and subsequently enters the cooling zone, where it is subjected to heat exchange with cold beer from the heat exchanger. This process lowers the temperature to the required level for bottling.
(3) Key Process Conditions:
- Sterilization temperature (inside the bottle) for post-bottling beer: 15°C → 30°C → 45°C → 62°C → 54°C → 45°C → 35°C. Spraying water pressure: 0.2–0.3MPa.
- During heating, the temperature difference between the water and beer should not exceed 30°C, and during cooling, it should not go below 22°C to reduce bottle and beer loss. It is advisable to add appropriate adsorbents, chelating agents, and alkali to the spraying water to maintain a weak alkaline environment. Sterilization process conditions for pre-bottling beer are similar to the described operation, usually controlled at 72–73°C, maintained for 30 seconds, or at 68–72°C, held for 50 seconds. The entire process takes about 2 minutes and has almost no impact on beer quality.
(4) Sterilization Process Requirements:
- Sterilized beer should not have yeast turbidity, and the appearance, flavor, and aroma of the finished beer should not significantly differ from the original beer. There should be no noticeable particles or black rings in the bottle neck.
- The volume of the bottle neck portion of bottled beer should be 3% of the total volume when sterilized at temperatures below 65°C and with a CO2 mass fraction of 0.4%–0.5%. When sterilized at temperatures above 65°C, it should be 4% of the total volume to prevent bottle breakage due to high pressure during sterilization.
- The distribution of spraying water should be uniform. The main sterilization zone should have a temperature of 61–62°C, with a sterilization effect of 15–30Pu.
(5) Operating Key Points:
- Strictly control temperatures and times in each zone. The temperature difference between zones should not exceed 35°C. The rate of temperature increase (decrease) for bottles should be controlled at 2–3°C/min to prevent bottle breakage.
- Monitor temperatures in each zone regularly and maintain temperature variations within ±1°C. Pu values should be measured 1–2 times per shift.
- Clean the machine body and nozzles at the end of each day’s work to keep the nozzles clear. Maintain a spraying water pressure of 0.2–0.3MPa.
- To prevent equipment corrosion due to acidic spraying water resulting from beer bottle breakage, adjust the pH of the spraying water to a neutral level (pH 7.6–8) using 1%–2% NaOH. If necessary, add 5–10mg/L trisodium phosphate to prevent nozzle blockage and the formation of salt deposits when bottles dry.
Labeling
The label of beer directly affects its appearance quality. Process requirements demand that the label used must be consistent with the product, and the production date must be clearly indicated. The label should be neat, well-aligned, not peeling off, and free of defects. The adhesive should be pH neutral, have good initial adhesion, appropriate instantaneous viscosity, and should not fall off during beer storage or become moldy or deteriorate when exposed to moisture. Labeling machines include straight-line vacuum drum labeling machines and rotary labeling machines. After labeling, the bottles can be packaged manually or mechanically (e.g., shrink-wrapped, placed in plastic or cardboard boxes) for sale.
The labeling process includes gluing, label pickup, label clamping, label application, label smoothing, and bottle positioning, bottle entry, bottle pressing, label advance, label pressing, and bottle exit.
Talk to our engineering team
Need help planning your packaging line?
Share your product, bottle and capacity requirements for a practical equipment recommendation.
Equipment
Craft Beer Can Filling Machine
Craft beer can filling and seaming with CGS models from 6,000 to 36,000 cans/hour at 330 ml.
Learn more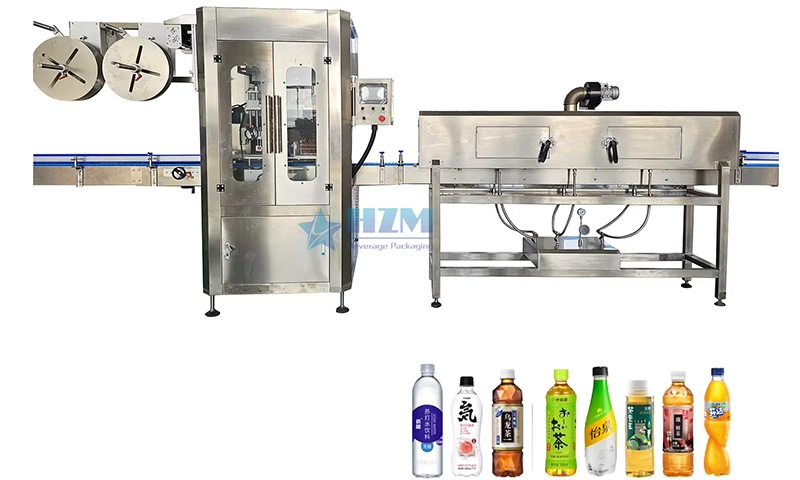
Equipment
Automatic Shrink Sleeve Bottles Labeling Capping Packing Machine
Automatic shrink sleeve application for beverage bottles, with SHB capacities of 9,000–27,000 bottles/hour.
Learn more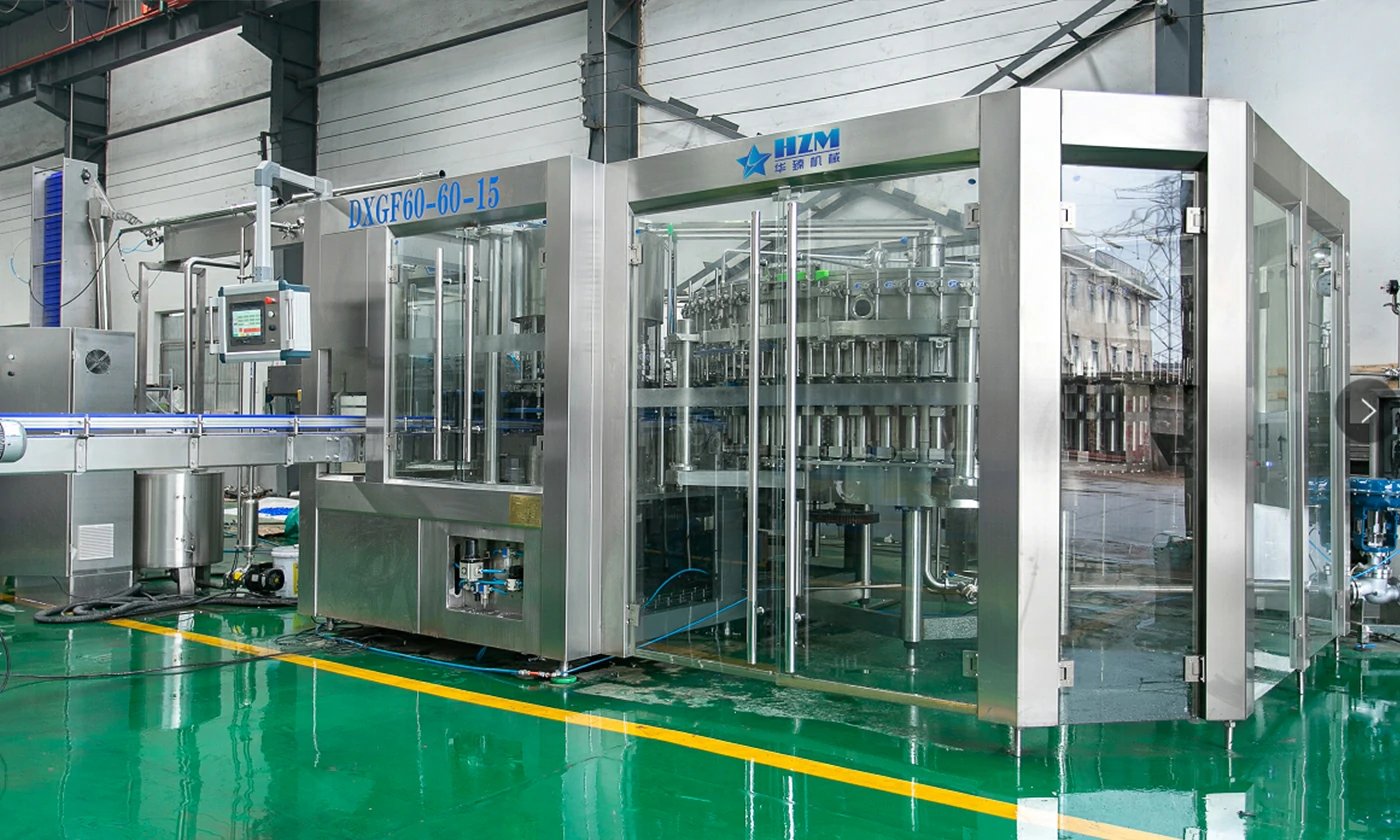
Equipment
Glass Bottle Beer & Beverage Filling Machine
DXGF60-60-15 glass bottle rinsing, isobaric filling and capping for beer and beverages, at 18,000 bottles/hour for 500 ml bottles.
Learn more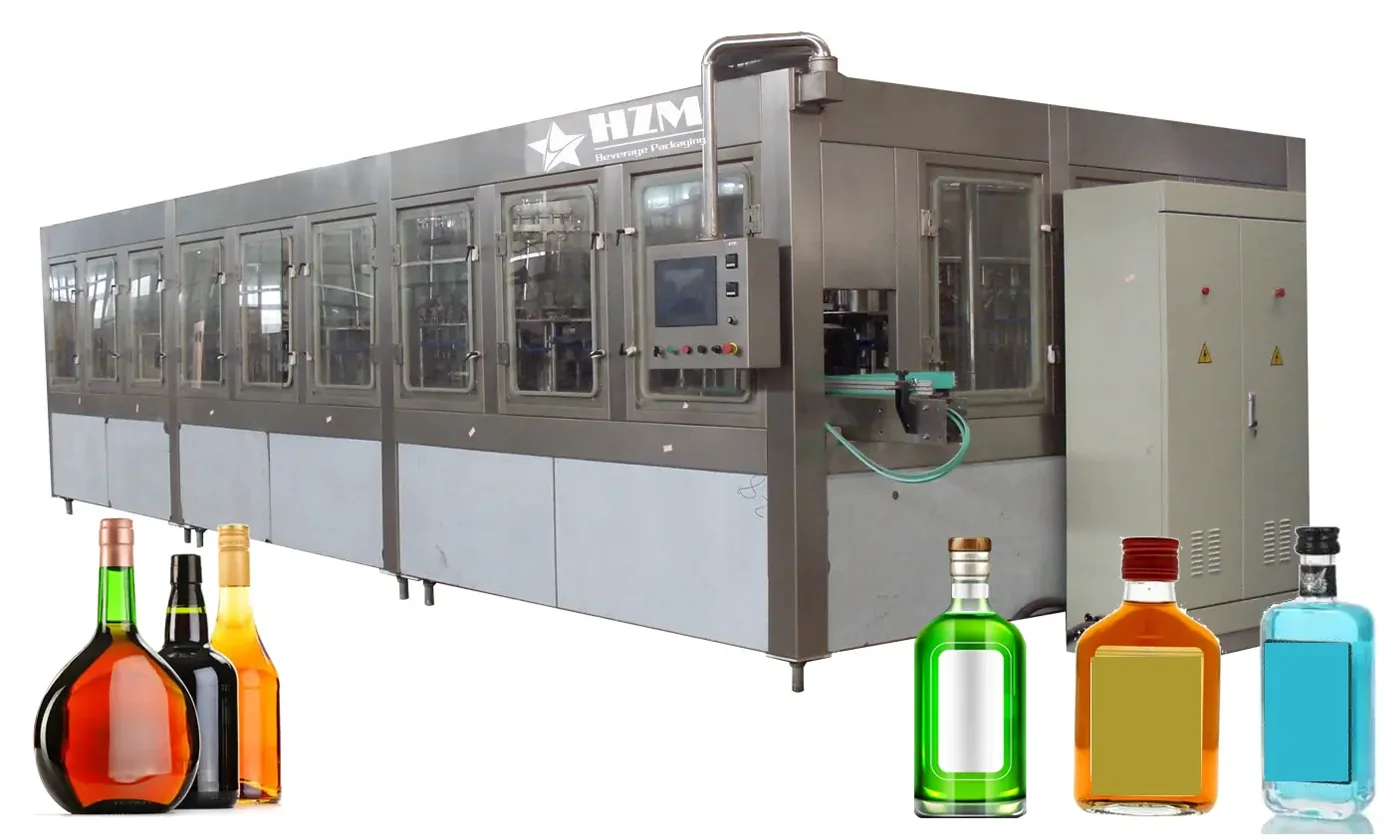
Equipment
Automatic Glass Wine Bottle Filling Machine
The glass-bottle filling machine combines rinsing, filling and capping for wine and compatible beverage products.
Learn more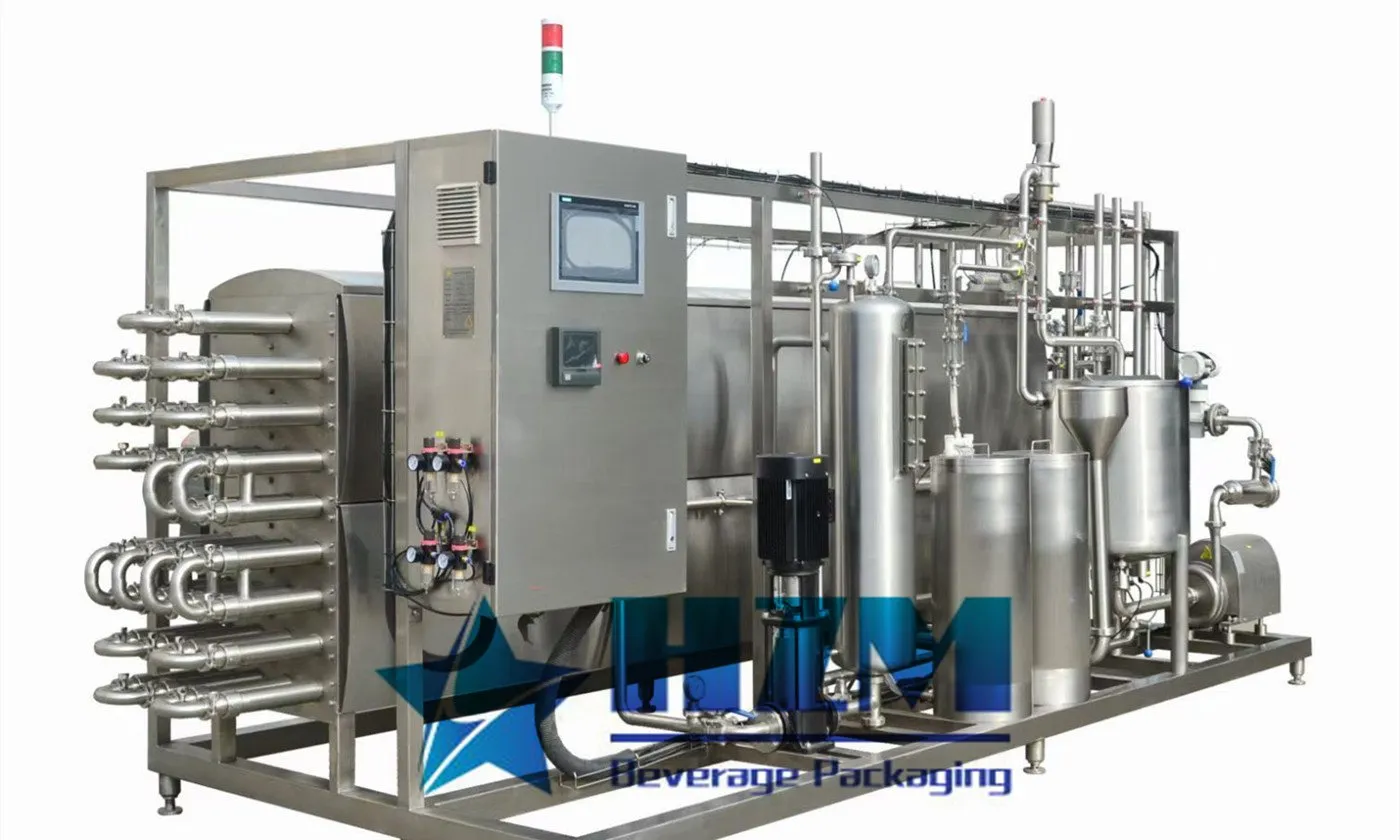
Equipment
UHT Sterilizer
The UHT sterilizer heats and cools liquid products continuously in a closed system.
Learn more
Equipment
Glass Bottle Filling Machine – DXGF14-12-5
DXGF14-12-5 glass bottle rinsing, isobaric filling and capping for carbonated drinks, at 2,000–3,000 bottles/hour for 750 ml bottles.
Learn more
Equipment
Automatic Water Bottle Labeling Machine
Automatic hot-glue labelling for water and beverage bottles, with HG models from 8,000 to 24,000 bottles/hour.
Learn more
Equipment
Blowing-Filling-Capping Machine
A PET combiblock that combines preform heating, bottle blowing, filling and capping at 12,000–48,000 bottles/hour at 500 ml.
Learn more
Equipment
Bottle Washing-Filling-Capping Machine
Large-bottle water rinsing, filling and capping with design outputs of 1,500 bottles/hour at 5 L, 1,000 at 7 L and 700 at 10 L.
Learn more
2023-10-03
Beer Filling Machine Principle
The beer filling process is well-established and can be divided into seven basic parts. The filling machine is designed around the filling process, and its working principle involves the following steps
Learn more
2023-10-05
Basic Principles of Beer Packaging
The beer packaging process is a complex step in the beer production, serving as the final stage that significantly impacts the quality of the end product and its sales. Filtered beer is transferred into bottles, cans, or kegs, and undergoes processes such as capping, biostabilization treatment, labeling, and boxing to become the finished beer product or is directly sold as such.
Learn more
2023-10-10
Forms and Methods of Beer Packaging
Different methods are employed for beer packaging, each with its unique advantages. The most common methods include pressurized filling, vacuum-assisted CO2 filling, double vacuum filling, CO2 counter-pressure filling, hot filling, and aseptic filling.
Learn more
2023-10-12
Processes and Maintenance of Beer Bottling Systems
CO2 → Bottle Caps → Labels → Beer Bottles → Selection → Bottle Washing Machine → Bottle Inspection → Filling Machine → Capping Machine → Quality Inspection → Sterilization Machine → Quality Inspection → Labeling Machine → Filtration of Beer → Packaging Machine → Bottled Beer
Learn more
2023-10-15
Key Points for Beer Filling in Beer Bottling Systems
When filling beer, it is essential to maintain strict sterility, minimize beer loss, prevent carbon dioxide (CO2) loss, and avoid contact between the beer and air to prevent oxidation. The filling valves must be clean and provide a good seal to prevent turbulence and beer surging.
Learn more
2023-10-27
Precautions for Beer Filling Machine
It is essential to control sterilization temperature and time to guarantee the sterilization effect. Additionally, one should avoid excessively high sterilization temperatures or prolonged sterilization times to minimize beer oxidation. After sterilization, the beer should be rapidly cooled to below a certain temperature (preferably below 35°C).
Learn more