Insights & Updates
Processes and Maintenance of Beer Bottling Systems
CO2 → Bottle Caps → Labels → Beer Bottles → Selection → Bottle Washing Machine → Bottle Inspection → Filling Machine → Capping Machine → Quality Inspection → Sterilization Machine → Quality Inspection → Labeling Machine → Filtration of Beer → Packaging Machine → Bottled Beer
- Cleaning of Empty Bottles
Both new and used bottles must undergo thorough cleaning. Recycled used bottles should be carefully selected, removing oil-stained bottles, bottles with defects, and cracked bottles. New bottles are cleaned by rinsing with high-temperature high-pressure hot water at 75°C (±3°C) or by spraying with a 1% alkali solution to remove grease. Recycled bottles may have varying levels of contamination, requiring an appropriate detergent formula for effective cleaning and sterilization. Common detergent formulas are listed in Table 5-2-1. The detergent used should be non-toxic.
(1) Requirements for Bottle Cleaning Process: The primary requirement is to have no residue inside or outside the bottle, sterile interior, and no alkaline reaction in any water drips from the bottle.
- The concentration and temperature of the alkaline water in each tank of the bottle washing machine must strictly follow the process parameters.
- The nozzles must remain unblocked. The temperature requirements for high-pressure rinsing are: hot alkaline water at 70°C, hot water at 50°C, warm water at 25–35°C, and cold water at 15–20°C. The spraying pressure is 0.2MPa, and the rinsing pressure is ≥0.15MPa.
- Sterile compressed air at a pressure of 0.4–0.6 MPa is used to blow out any remaining water from inside the bottles.
- The alkaline solution used during bottle washing can be recycled.
- Clean bottles should be free of residue, both inside and outside. When inverted for 2 minutes, no more than 3 drops of water should come out, and there should be no residual alkali (0.5% phenolphthalein should not turn red).
(2) Types of Bottle Washing Machines:
- Classified by structure: Single-end (both bottle entry and exit are on the same end of the machine) and double-end (bottle entry and exit are on opposite ends of the machine).
- Classified by operation mode: Intermittent and continuous.
- Classified by washing method: Spray and soak method (uses a specific temperature washing solution for immersing and spraying old bottles), brush method (uses brushes and is now outdated).
- Classified by material of the bottle crate: Full plastic type, semi-plastic type, and full metal type.
(3) Key Components of the Bottle Washing Machine:
- The machine’s body is a rectangular casing with 5–9 compartments separated by partitions. It contains two or more heaters to maintain the required temperatures in different soaking tanks and spray systems. The piping system includes steam pipes, cold water pipes, detergent pipes, and several water pumps to circulate the alkaline solution and warm water in the soaking tanks, as well as to spray the bottles.
- The main drive system is powered by an electromagnetic continuously variable-speed motor and a gearbox that drives the main drive shaft. It also drives the chain box device, spraying frame, bottle entry system, bottle exit system, etc. The main drive shaft has overload protection safety features, and there are clutch and automatic return mechanisms in case of faults in the entry and exit mechanisms.
- The bottle entry system varies depending on the machine type. Common systems include bottle support beam, rotating bottle entry device, and cam mechanism for bottle entry. These systems ensure that bottles are pushed into the crate while moving downward to provide sufficient time to place the bottles inside the crate.
- The bottle exit system can be free-falling, rotating bottle receiving, or reciprocating bottle receiving.
- The label removal device consists of a circular steel belt, sprockets, chains, and a blower. It aims to remove labels that detach during alkaline soaking to prevent clogs in the nozzle and ensure proper cleaning.
- The spray system includes a spray frame driving device and spray nozzles. The spray frame moves back and forth along with the chain box’s movement. During approximately 2/3 of its movement, it sprays along with the chain box, while the remaining 1/3 is the return journey.
- Additional equipment includes electrical control cabinets and operating panels.
(4) Maintenance and Care of the Bottle Washing Machine:
- Continuous observation of the machine’s operation during its runtime is essential. Any abnormal conditions should be addressed immediately. Regularly lubricate the bearings of the sleeve roller chain, bottle entry system, bottle exit system, and return mechanism every shift. Lubricate the chain box drive shaft, universal joint, and other bearings every two shifts. Inspect the lubrication of various gearboxes every quarter and replace lubricating oil as needed. After changing the washing solution and discharging wastewater, thoroughly clean the machine’s interior, removing dirt and broken glass, and clean the filter cartridges. Brush and clear the nozzles monthly, ensuring proper alignment. High-pressure water should be used to clean the heaters every quarter, and filters and level detectors in the steam pipeline should be cleaned. Chain tensioners of various types should be inspected every six months and adjusted as needed.
(5) Key Process Conditions:
- Bottle washing temperature: 20°C → 50°C → 70°C → 50°C → 30°C → 15°C.
- Bottle washing pressure: Spraying pressure of 0.25MPa, rinsing pressure of 0.15MPa.
- Sterile air pressure: 0.4–0.6MPa.
Adjust the soaking bottle temperature based on ambient temperature. The temperature rise and fall for soaking should be smooth, and the temperature difference between the liquid and the bottle should not exceed 35°C to prevent bottle breakage. The soaking temperature for alkaline washing solution should be controlled between 65–70°C, never below 55°C, and the temperature for alkali solution spraying should not exceed 75–85°C. Test the alkaline solution concentration approximately every 2 hours to maintain stability.
(6) Empty Bottle Inspection:
Empty bottle inspection methods include optical inspection and manual inspection.
- Optical inspection includes bottom inspection and full-bottle inspection techniques. Full-bottle inspection may include one or more bottom inspection stations, checking for alkali solution or residual liquid twice and examining the bottle’s walls. The seal area is primarily examined. Optical inspection devices automatically push out dirty and damaged bottles from the conveyor belt, and they can include a device for identifying and removing abnormal bottles.
- Manual inspection involves using lighting to inspect the bottle neck, body, and bottom. If a bottle does not meet the requirements, it is immediately removed and handled separately. Inspectors must rotate regularly. The bottle conveyor speed is generally 80–100 bottles per minute, and for high-speed filling, a dual-track inspection system can be used.
Empty bottle inspection process requirements: Bottles should be clean inside and out, free of dirt, debris, and residue from old labels. Bottles should not have cracks, chipped rims, or other defects, and their heights should be consistent.
(7) Maintenance and Care of the Bottle Washing Machine:
- Continuous monitoring of the synchronization of various parts, abnormal noises, looseness of fasteners, compliance with temperature and liquid level requirements, normal water and steam pressure, nozzle cleanliness and blockage, bearing temperatures, and lubrication quality is crucial. Any abnormal conditions should be promptly addressed.
- Follow maintenance requirements as per the bottle washing machine’s manual. Lubricate the bearings of the sleeve roller chain, bottle entry system, bottle exit system, and return mechanism every shift. Lubricate the chain box drive shaft, universal joint, and other bearings every two shifts. Inspect the lubrication of various gearboxes every quarter and replace lubricating oil when necessary. After each change of the washing solution and wastewater discharge, conduct thorough machine interior cleaning, removing dirt and broken glass, and clean filter cartridges. Brush and clear the nozzles every month, adjusting the nozzle alignment as needed. Use high-pressure water to clean the heaters quarterly and clean the dirt filters and level detectors in the steam pipeline. Inspect various chain tensioners every six months and adjust as needed.
Talk to our engineering team
Need help planning your packaging line?
Share your product, bottle and capacity requirements for a practical equipment recommendation.
Equipment
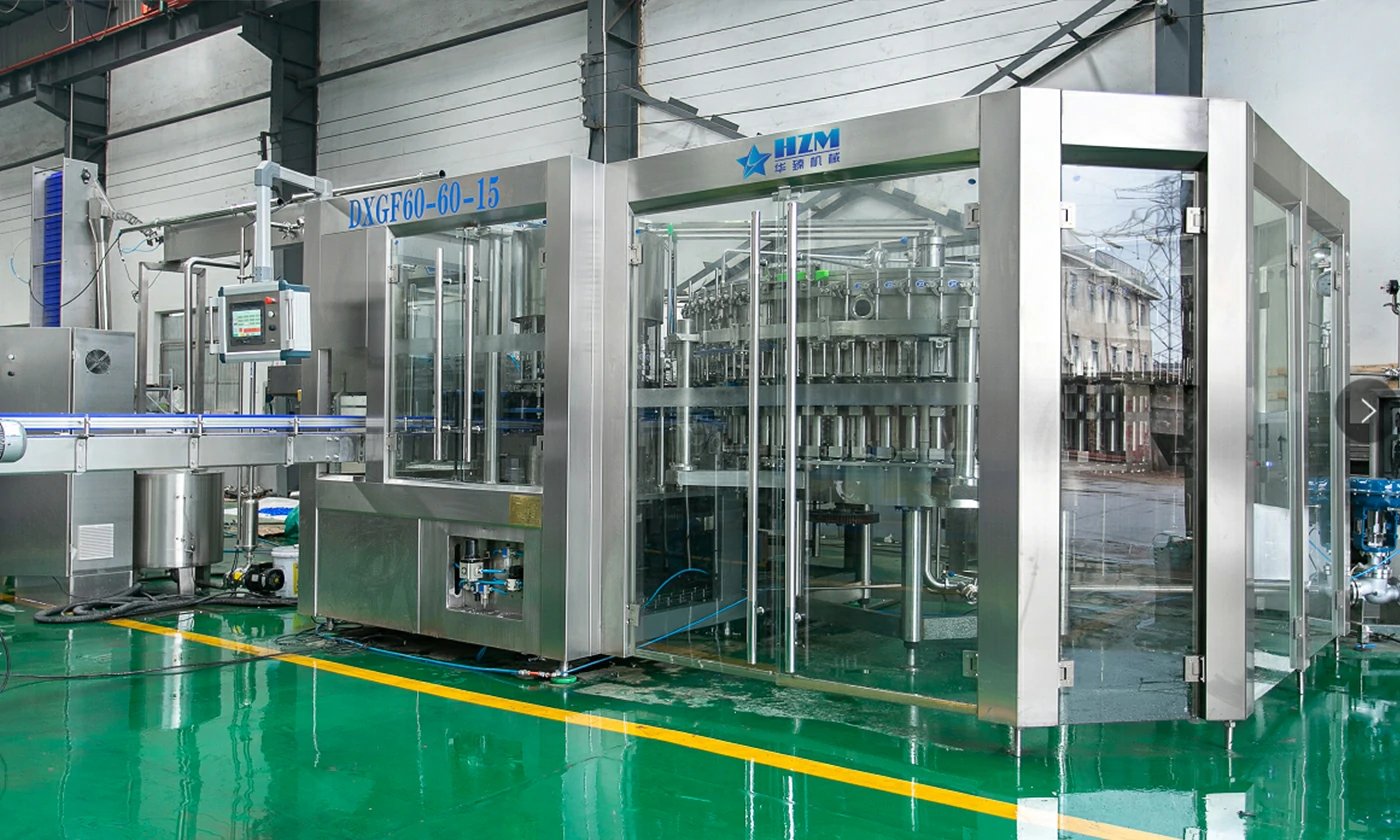
Glass Bottle Beer & Beverage Filling Machine
DXGF60-60-15 glass bottle rinsing, isobaric filling and capping for beer and beverages, at 18,000 bottles/hour for 500 ml bottles.
Learn more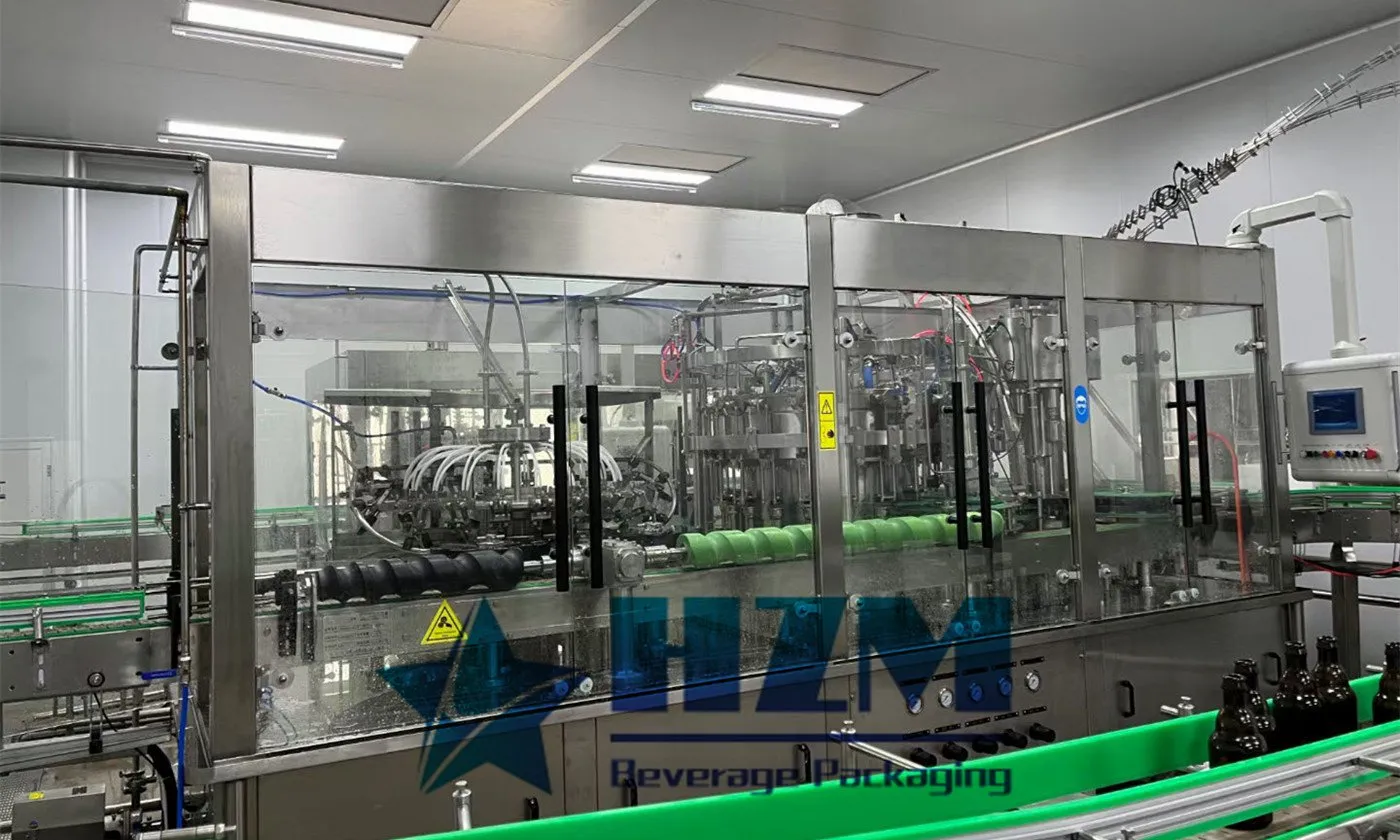
Equipment
Craft Beer Can Filling Machine
Craft beer can filling and seaming with CGS models from 6,000 to 36,000 cans/hour at 330 ml.
Learn more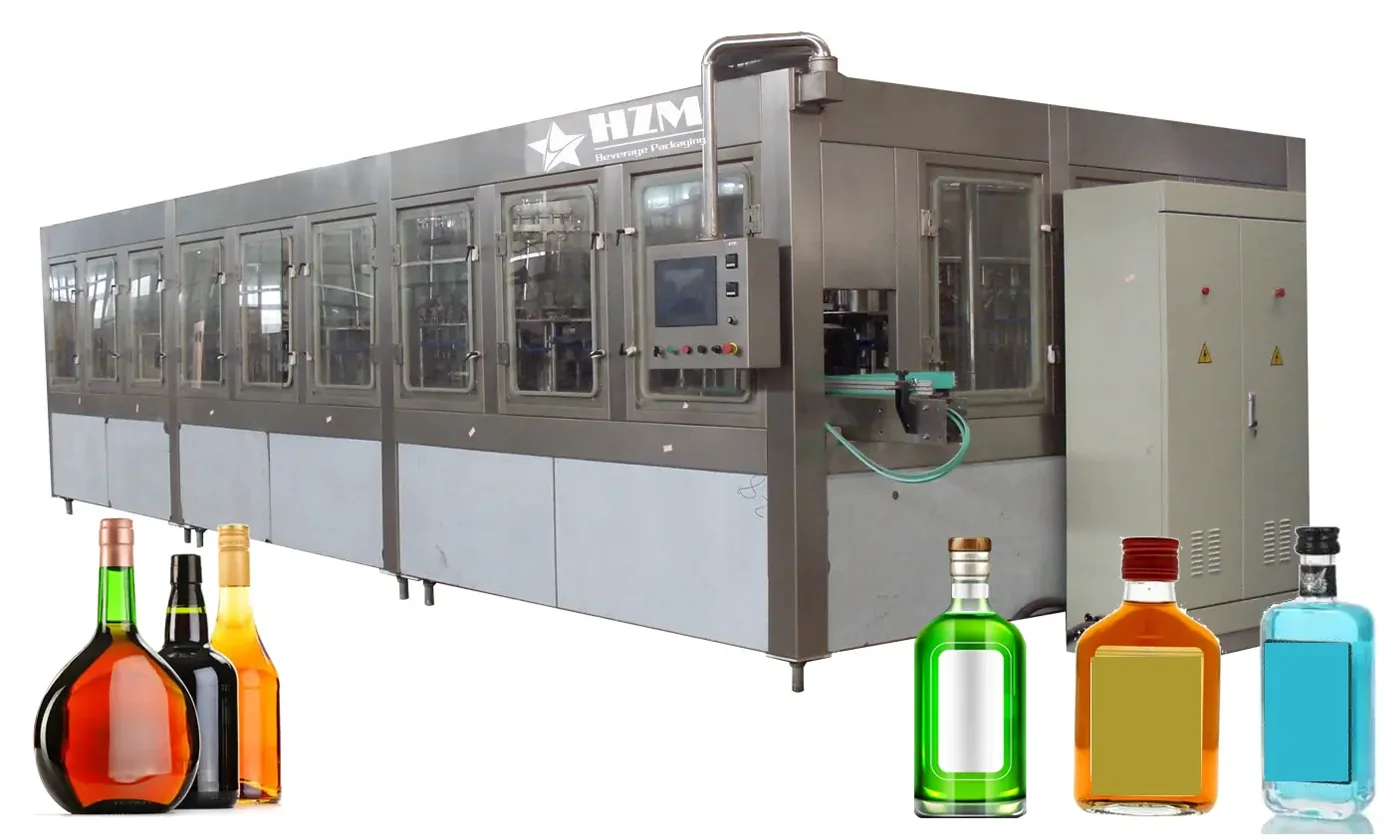
Equipment
Automatic Glass Wine Bottle Filling Machine
The glass-bottle filling machine combines rinsing, filling and capping for wine and compatible beverage products.
Learn more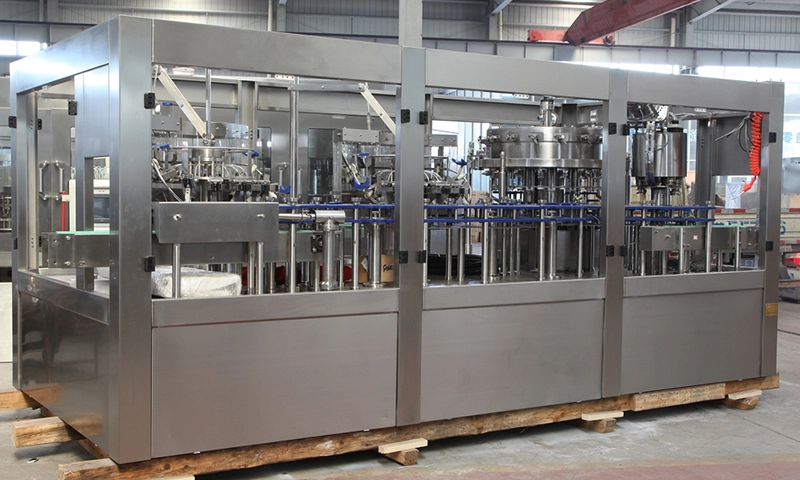
Equipment
Glass Bottle Filling Machine – DXGF14-12-5
DXGF14-12-5 glass bottle rinsing, isobaric filling and capping for carbonated drinks, at 2,000–3,000 bottles/hour for 750 ml bottles.
Learn more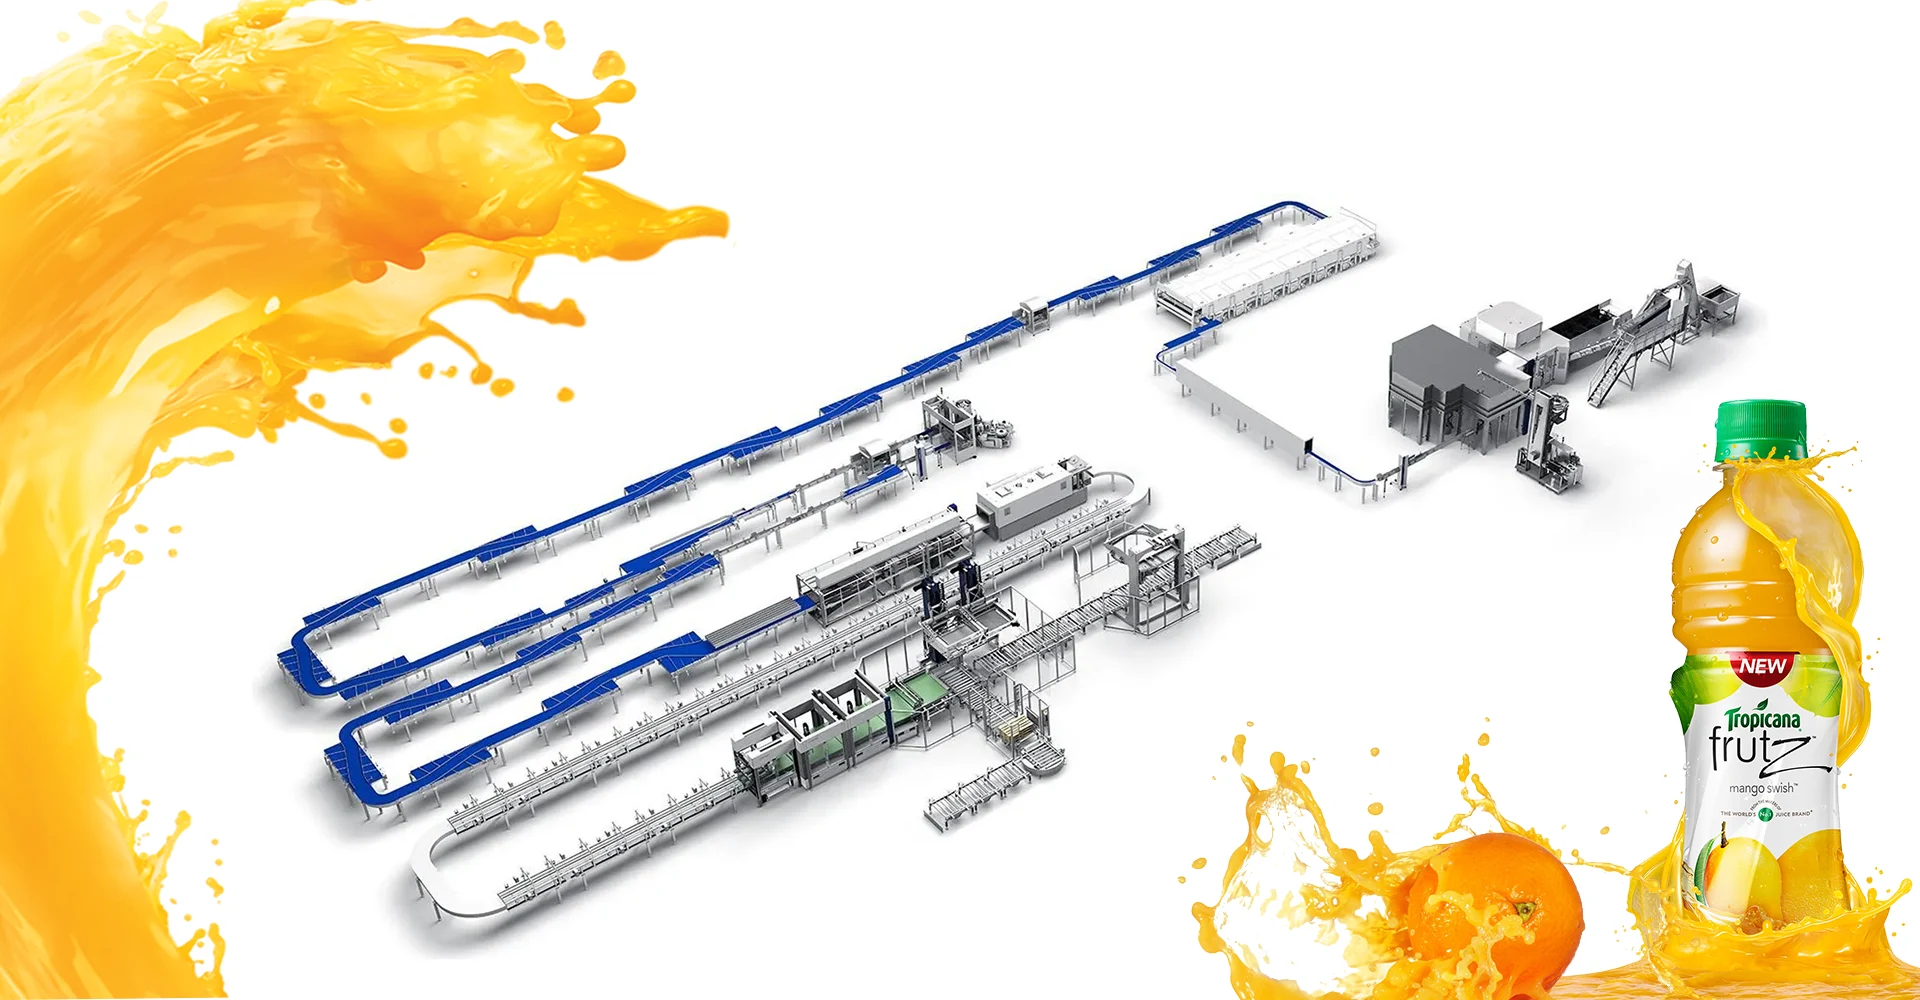
Equipment
Beverage Filling Line – Juice, Water, Soft Drinks, cola, Beer
Complete beverage filling lines for juice, water, soft drinks and beer, with bottle and can packaging options.
Learn more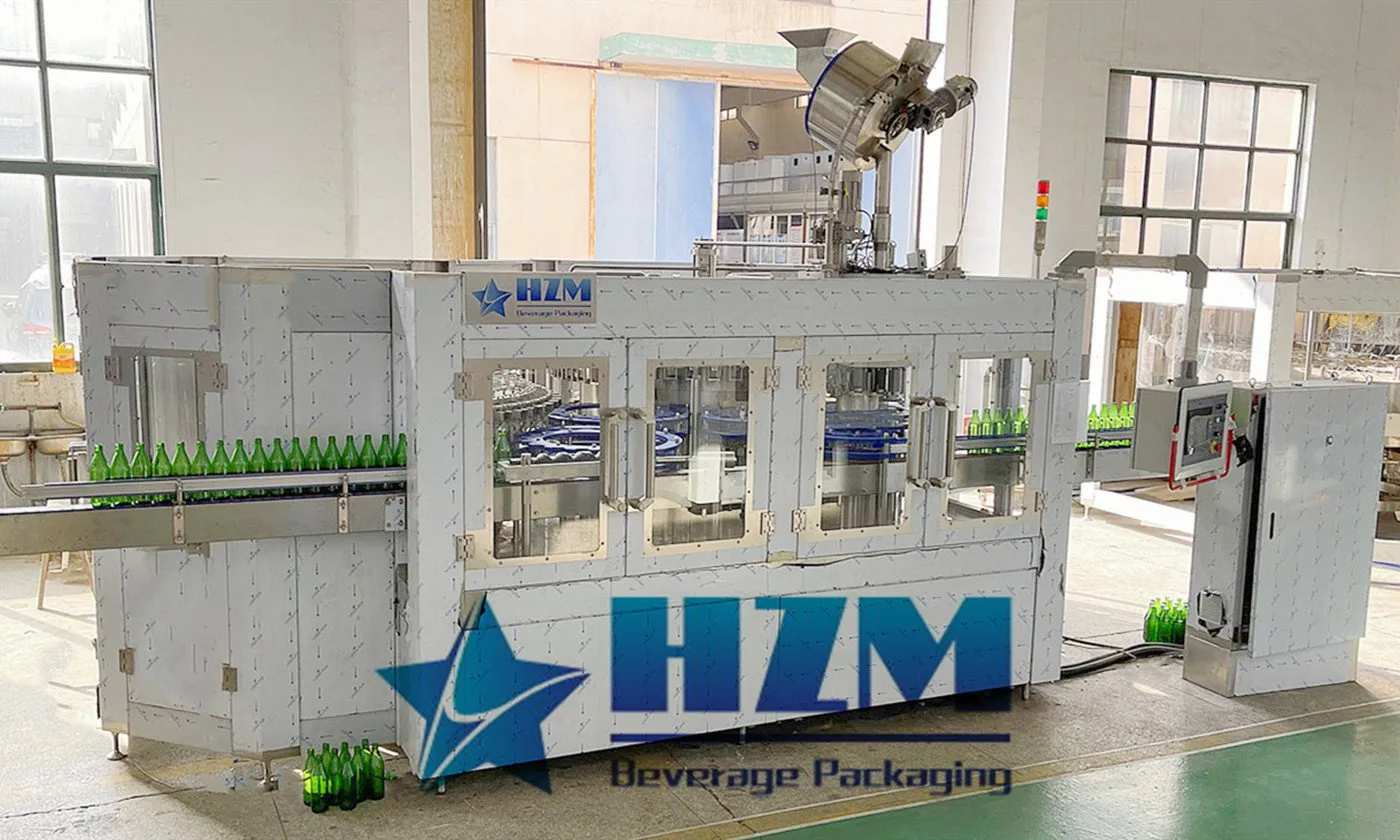
Equipment
Glass Bottle CSD Beverage Filling Machine
Glass bottle filling for carbonated beverages, with isobaric filling and capacities of 2,000–20,000 bottles/hour at 500 ml.
Learn more
Equipment
Glass Bottle Juice Beverage Filling Machine
Glass bottle juice filling with rinsing and capping, for juice, tea and other still beverages.
Learn more
Equipment
Glass Bottle CSD & Water Drinks Filling Machine
DXGF24-24-8-8 glass bottle isobaric filling for carbonated drinks, with rinsing and two capping stations.
Learn more
Equipment
Glass Bottle Carbonated Beverage Filling Bottling Line
This glass bottle carbonated beverage line combines bottle rinsing, isobaric filling and capping with conveying, labelling and packing.
Learn more
2023-10-03
Beer Filling Machine Principle
The beer filling process is well-established and can be divided into seven basic parts. The filling machine is designed around the filling process, and its working principle involves the following steps
Learn more
2023-10-05
Basic Principles of Beer Packaging
The beer packaging process is a complex step in the beer production, serving as the final stage that significantly impacts the quality of the end product and its sales. Filtered beer is transferred into bottles, cans, or kegs, and undergoes processes such as capping, biostabilization treatment, labeling, and boxing to become the finished beer product or is directly sold as such.
Learn more
2023-10-10
Forms and Methods of Beer Packaging
Different methods are employed for beer packaging, each with its unique advantages. The most common methods include pressurized filling, vacuum-assisted CO2 filling, double vacuum filling, CO2 counter-pressure filling, hot filling, and aseptic filling.
Learn more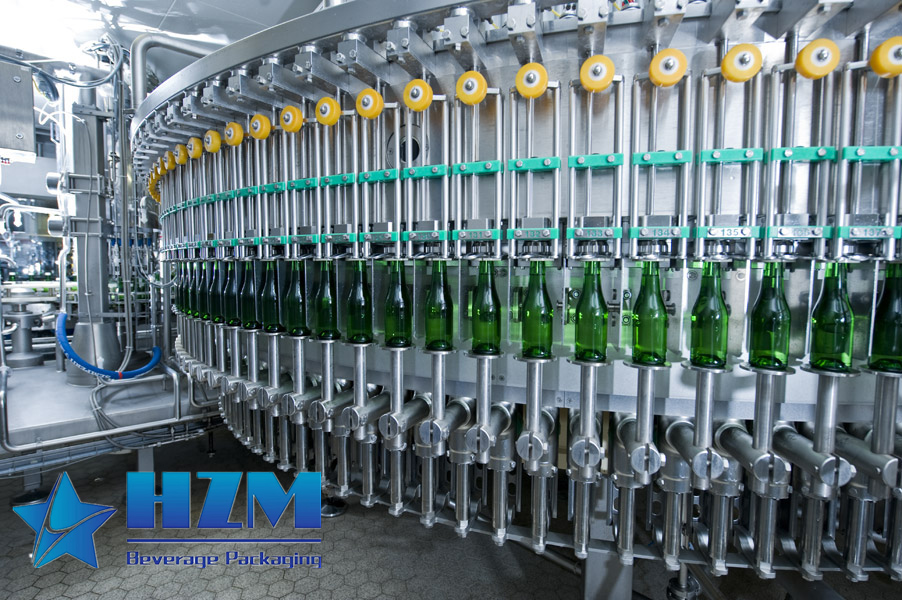
2023-10-15
Key Points for Beer Filling in Beer Bottling Systems
When filling beer, it is essential to maintain strict sterility, minimize beer loss, prevent carbon dioxide (CO2) loss, and avoid contact between the beer and air to prevent oxidation. The filling valves must be clean and provide a good seal to prevent turbulence and beer surging.
Learn more
2023-10-17
Capping, Sterilization, and Labeling in Beer Bottling Systems
Filled beer bottles should be capped promptly, ensuring there is no air in the bottle neck during capping. Glass bottles used for beer are typically sealed with crown caps, which have 21 serrations that seal the bottle when pressed together during capping.
Learn more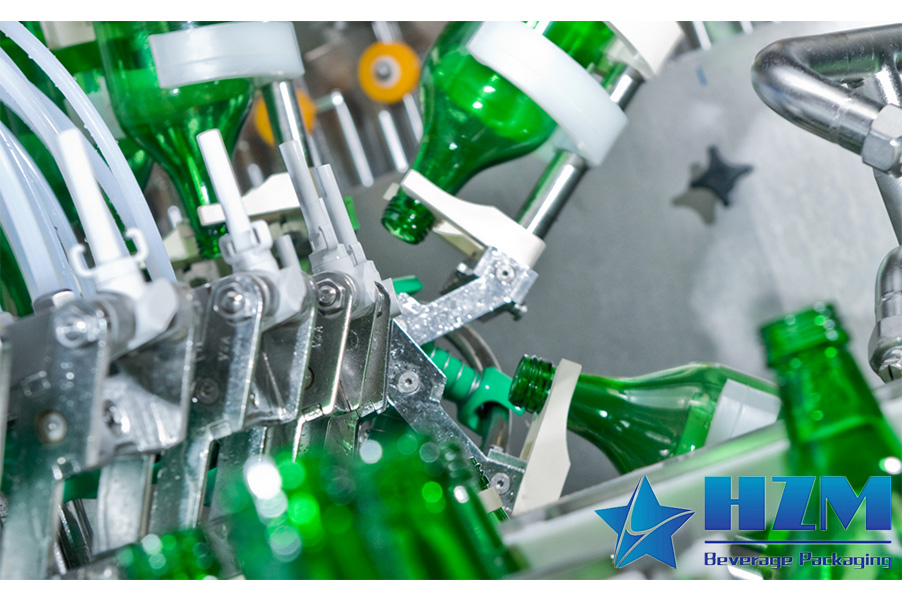
2023-10-27
Precautions for Beer Filling Machine
It is essential to control sterilization temperature and time to guarantee the sterilization effect. Additionally, one should avoid excessively high sterilization temperatures or prolonged sterilization times to minimize beer oxidation. After sterilization, the beer should be rapidly cooled to below a certain temperature (preferably below 35°C).
Learn more